 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


45-degree elbow mold (1-cavity-4)
FEATURES
Hard Infrastructure — The Foundation of Customer Trust
1.1 Mold Machining Equipment
Ansix is equipped with 5-axis high-speed machining centers capable of machining complex curved surfaces with 0.002mm precision. This ensures that the parting lines on your 45-degree elbow products are smooth and free from burrs — eliminating secondary deburring operations and reducing post-processing costs.
Slow wire EDM (Electrical Discharge Machining) is available for machining fine micro-holes and narrow slots as small as 0.03mm. This capability is critical for the 45-degree elbow geometry, preventing thin-wall deformation and ensuring dimensional integrity in the elbow's curved sections.
-
Mold Description
Product Materials:
pvc
Mold Material:
S136ESR
Number of Cavities:
2+2
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
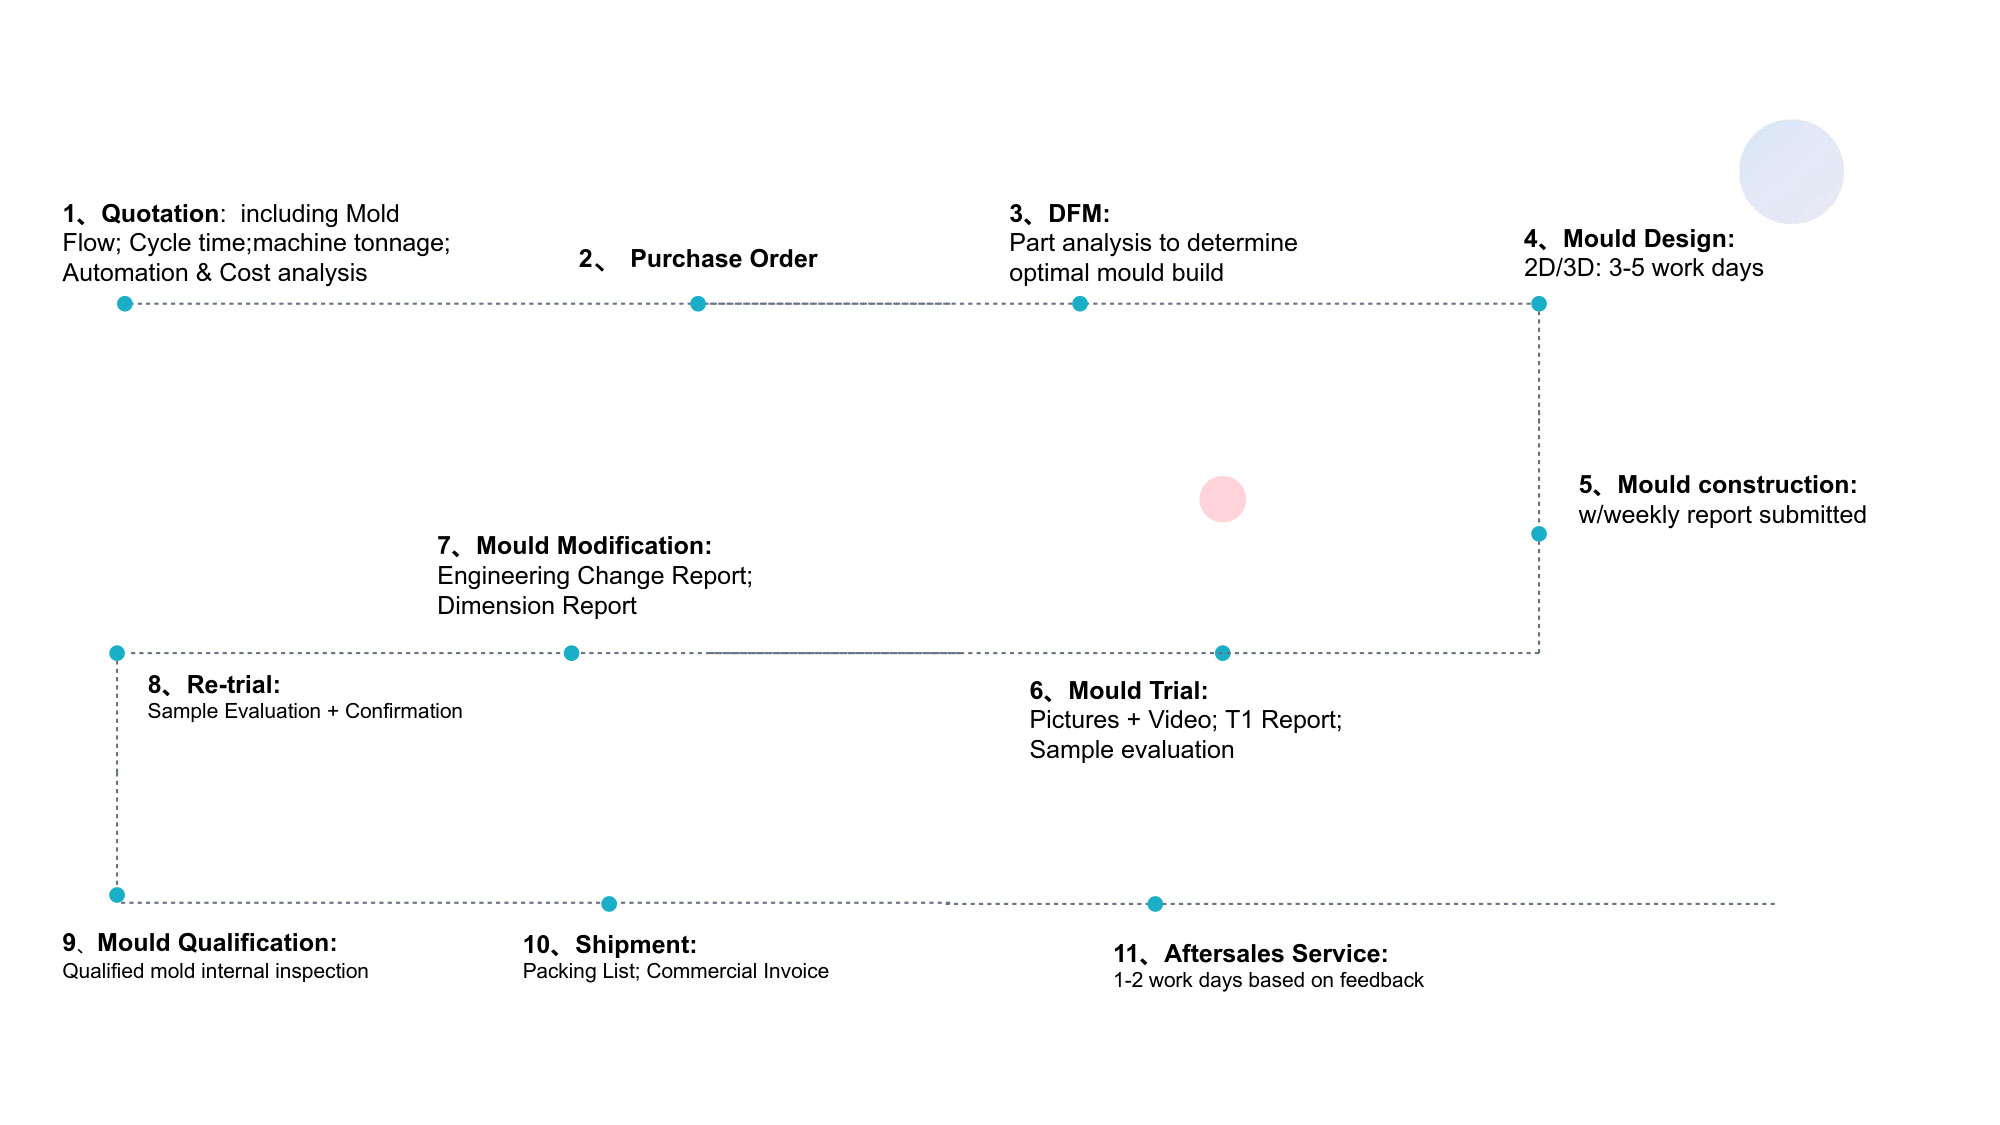
- The mold manufacturing process and product material selection
Injection Molding Machine Fleet
Ansix operates a comprehensive range of injection molding machines with clamping forces ranging from 30 tons to 4,000 tons, covering a broad spectrum of product sizes from miniature precision components to large-diameter pipe fittings.
All machines are equipped with full servo-motor drives, delivering stable repeatability accuracy of ±0.1% . This means every shot in a production run is consistent with the previous one — batch after batch, day after day. For customers, this translates to predictable quality, reduced scrap rates, and fewer production interruptions.
-
Inspection and Metrology Equipment
Ansix employs CMM (Coordinate Measuring Machines) and optical image measurement instruments as standard inspection tools. Every mold undergoes a full dimensional report comparison before shipment. Critical dimensions are verified with Cpk ≥ 1.33 — a statistical measure that demonstrates the process capability index, indicating that the manufacturing process is stable, capable, and produces parts well within specification tolerances.
For customers, this means:
Zero dimensional surprises when the mold arrives at your facility
Immediate production readiness — no need for rework or adjustment
Predictable part quality from the very first production run
Part II: Mold Manufacturing Core Competitiveness — Speaking in Numbers
2.1 Mold Life Expectancy
Parameter Technical Specification Customer Value
Mold Base P20 steel Structural integrity and long-term stability
Core/Cavity S136, 2344, 2343, 8407, SKD11/61, DC53, M340, 4Cr13, 9Cr18, NAK80, H13 Optimized material selection for specific application requirements
Mold Life (Glass-filled materials) 500,000 shots guaranteed Long production runs without mold replacement
Mold Life (Standard plastics) 1,000,000 shots guaranteed Maximum ROI on mold investment
Ansix provides material certificates and heat treatment curves for all mold steels, ensuring full traceability and quality documentation.
2.2 Achievable Tolerances
Component Type Achievable Tolerance Industry Context
General structural components ±0.05mm Standard industry requirement
Precision gears / medical components ±0.005mm Meets the most demanding applications
For the 45-degree elbow, where angular accuracy and sealing surface integrity are critical, these tolerances ensure:
Leak-free connections in pipe fitting applications
Consistent flow characteristics across all produced parts
Interchangeability between production batches
2.3 Mold Type Capabilities
Ansix offers a comprehensive range of mold configurations:
Hot runner systems — reduce material waste by eliminating cold runner scrap, raising material utilization from 60–70% to 95–98%
Stack molds — double production efficiency with the same machine footprint
Two-shot / multi-material molds — for complex multi-component parts
High-gloss molds — surface finish Ra < 0.05μm, ideal for transparent or cosmetic-grade components
2.4 Gating System Optimization
Ansix employs Moldflow analysis to predict weld line locations, gas trap positions, and filling behavior before steel is cut. This enables:
Optimized gate location and quantity for balanced cavity filling
Elimination of short shots and incomplete filling
Reduced cycle time through optimized flow paths
Minimized part stress and warpage
Customer value: The 1-cavity-4 configuration means four elbows are produced in each cycle. Balanced filling across all four cavities ensures that every elbow is identical — no "good cavity/bad cavity" variation.
2.5 Lead Time Standards
Mold Complexity Standard Lead Time Expedited Lead Time
Simple molds 10 days —
Medium complexity 25–45 days 20 days (with full validation maintained)
Critical note: Even under expedited schedules, Ansix does not skip or shorten validation steps. Every mold undergoes full testing and verification before shipment — protecting customers from the risk of receiving an unproven tool.
Part III: Injection Molding Process Control — Eliminating Quality Anxiety
3.1 Process Standardization
All Ansix machines are networked and integrated with a MES (Manufacturing Execution System) . Injection parameters — temperature, pressure, speed, and time — are locked within the MES system and can only be modified by authorized engineers.
First-article and last-article inspections are performed for every production batch. This ensures:
Zero drift in production quality over long runs
Full traceability from raw material to finished part
Immediate detection of any process deviation
3.2 Dimensional Stability Control
Ansix employs mold temperature controllers with zonal temperature control, maintaining the core and cavity temperature differential within ±2°C. This minimizes warpage and distortion — particularly critical for the 45-degree elbow's curved geometry.
Real-world validation data: For similar bracket products, three consecutive production batches over one week showed key hole spacing variation ≤ 0.02mm — demonstrating exceptional process stability.
3.3 Surface Finish Capabilities
Requirement Achievable Standard Application
Transparent parts No bubbles, no flow marks Clear PVC/PC elbows
Plated parts No gas marks Decorative or corrosion-resistant fittings
High-gloss parts Surface roughness Ra ≤ 0.2μm Cosmetic-grade components
Printed/coated parts Print registration accuracy ±0.1mm (with pre-compensation) Branded or marked fittings
3.4 Special Material Capabilities
Ansix has extensive production experience with a wide range of engineering plastics:
PC/ABS — automotive and appliance applications
PC — transparent and high-impact applications
PPS + 40% GF — high-temperature, chemical-resistant applications
PEEK — high-performance engineering applications
PTFE / PFA — chemical-resistant and non-stick applications
PA6 + GF30 — structural and automotive applications
PBT — electrical and electronic applications
PEI / PPS / LCP — high-temperature electronic applications
Liquid Silicone Rubber (LSR) — medical and sealing applications
Flame retardancy: UL94 V-0 rated materials available for electrical housing applications.
Weather resistance: UV testing validated to 3,000 hours without discoloration.
Part IV: Full-Service Lifecycle — Reducing Customer Management Costs
4.1 Early-Stage Intervention — DFM Report
Before any contract is signed, Ansix provides a comprehensive Design for Manufacturability (DFM) report. This includes:
Draft angle recommendations — ensuring easy part ejection
Wall thickness optimization — balancing strength, weight, and cooling
Gate location suggestions — optimizing fill and minimizing visible marks
Ejector pin mark location guidelines — placing marks in non-critical areas
Moldflow analysis results — predicting and preventing defects
Customer value: Problems are identified and solved before the mold is built — not after. This eliminates costly design changes, reduces time-to-market, and prevents the "we should have caught this earlier" scenario.
4.2 Trial Molding and Sampling
Ansix provides T0 through T3 trial samples, with improvement reports accompanying each iteration. The team can rapidly exchange inserts to validate different design approaches without rebuilding the entire mold — saving both time and money.
4.3 Small-Batch Validation
Before committing to full-scale production, Ansix offers 100–500 shot pilot runs. During this phase:
Yield rate is statistically calculated
Cpk is verified on all critical dimensions
Process stability is confirmed
Only after passing this validation does Ansix proceed to mass production. This protects customers from the risk of scaling up an unstable process.
4.4 Maintenance and Spare Parts
Spare wear parts (ejector pins, core inserts) are delivered with the mold
Maintenance service is provided every 200,000 shots
Lifetime repair service is available at cost price
Part V: Competitive Differentiation — Direct Solutions to Common Industry Pain Points
5.1 Addressing Common Customer Complaints
Customer Complaint Ansix's Professional Response Measurable Benefit
"Molds need frequent repairs, disrupting orders" 2,000-shot aging test before delivery with wear report; 3-year structural warranty (excluding normal wear parts) Predictable production uptime; no unexpected downtime
"Excessive flash, high post-processing costs" Parting line machined to 0.005mm fit tolerance; self-locking clamp force compensation; flash controlled to ≤ 0.03mm per batch Eliminates manual deburring; reduces labor costs
"Dimensions vary between batches" Ultrasonic wall thickness sensors with real-time feedback; in-mold temperature/pressure sensors for closed-loop control Consistent dimensions batch after batch
"Mold repair takes too long" In-house electrode machining and EDM workshop; routine weld repair/insert replacement completed within 24 hours Minimizes production stoppage time
5.2 The Ansix Value Proposition
"To our valued customers: a mold is not just a piece of steel — it's a money-printing machine. When we design a mold, we simultaneously plan for injection molding robustness, venting paths, and thermal balance. The result is a mold that arrives at your production line ready to run — no debugging, minimal flash, maximum lifespan."
Part VI: Detailed Manufacturing Process — 45-Degree Elbow Mold (1-Cavity-4)
6.1 Raw Material Selection and Material Characteristics
The material selection for the 45-degree elbow component is driven by the application requirements — pipe fittings must withstand pressure, temperature variations, and often chemical exposure.
Common materials for 45-degree elbow fittings:
PVC (Polyvinyl Chloride) — widely used for plumbing and drainage applications
PP-R (Polypropylene Random Copolymer) — hot and cold water plumbing systems
PE (Polyethylene) — gas and water distribution systems
PC/ABS blends — higher temperature and impact resistance
Nylon (PA6/PA66) with glass fiber reinforcement — high-strength industrial applications
Material properties considered:
Melt flow index — affects fill behavior and cycle time
Shrinkage rate — critical for dimensional accuracy
Thermal stability — affects cooling and cycle time
Chemical resistance — determines application suitability
Ansix provides full material certification and traceability documentation for every production batch.
6.2 Mold Flow Analysis and DFM
Mold flow analysis is conducted using industry-standard simulation software. For the 45-degree elbow 1-cavity-4 configuration, the analysis focuses on:
Balanced filling across all four cavities — ensuring each elbow is identical
Weld line prediction — identifying and mitigating weak points in the elbow's curved section
Gas trap identification — preventing burn marks and incomplete filling
Pressure drop analysis — ensuring adequate packing pressure reaches all areas
Cooling analysis — optimizing cycle time while maintaining dimensional stability
DFM recommendations include:
Draft angle optimization for easy ejection from the curved geometry
Wall thickness analysis to prevent sink marks and warpage
Gate placement to minimize visible marks on cosmetic surfaces
Ejector pin placement in non-critical areas
6.3 Mold Design Key Points
The 45-degree elbow mold design presents unique challenges due to the part's geometry:
Core pulling mechanism — the 45-degree angle requires specialized slide or lifter mechanisms to release the part
Parting line selection — must accommodate the elbow's curved geometry while maintaining a clean, flash-free seal
Cooling system design — conformal cooling channels follow the elbow's curvature for uniform heat extraction
Ejection system — must clear the curved geometry without damaging the part
6.4 Mold Manufacturing Challenges and Process Flow
Manufacturing challenges for the 45-degree elbow mold:
Complex curved surfaces — requiring 5-axis machining capability
Tight tolerances on the sealing surfaces — critical for leak-free fittings
Core and cavity alignment — must maintain precise registration across the parting line
Surface finish requirements — smooth surfaces for proper flow and easy release
Manufacturing process flow:
CAD/CAM design — 3D modeling and toolpath generation
High-speed CNC milling — roughing and finishing of mold components
EDM (Electrical Discharge Machining) — for fine details and complex cavities
Heat treatment — achieving target hardness (typically HRC 48-55 for tool steels)
Precision grinding — achieving micron-level surface finishes
Polishing — achieving required surface roughness (Ra < 0.05μm for high-gloss applications)
Assembly and fitting — ensuring proper slide and ejector operation
Testing and validation — trial shots and dimensional verification
6.5 Cooling System / Water Lines / Runners / Gating / Ejection System Design
Cooling system: Designed for uniform heat extraction across all four cavities. Conformal cooling channels follow the elbow's geometry where possible. Zonal temperature control maintains core/cavity temperature differential within ±2°C.
Runner system: Optimized for balanced fill across all four cavities. Hot runner systems are recommended for high-volume production, eliminating cold runner waste and reducing cycle time.
Gating system: Gate location and size are optimized through Moldflow analysis. Options include:
Edge gates — for general applications
Submarine gates — for automatic degating
Hot tip gates — for high-quality cosmetic surfaces
Ejection system: Designed for reliable, damage-free part ejection. Ejector pins are placed in non-critical areas. The system accounts for the 45-degree elbow's geometry, ensuring smooth release without distortion.
6.6 Mold Validation and Injection Molding Challenges
Validation process:
T0 trial — first shot, check for basic fill and function
T1 trial — dimensional verification, identify issues
T2 trial — process optimization, fine-tuning
T3 trial — final validation, Cpk verification
Small-batch validation — 100-500 shots, yield rate and capability confirmation
Injection molding challenges for the 45-degree elbow:
Balanced filling across four cavities in a single cycle
Warpage control — the curved geometry is prone to distortion
Sink marks — at thick sections of the elbow
Weld lines — where flow fronts meet in the curved section
Ejection — clearing the 45-degree geometry without damage
6.7 Injection Molding Process Optimization
Efficiency improvement:
Cycle time reduction through optimized cooling and process parameters
Hot runner systems reducing material waste from 30-40% to 2-5%
Servo-hydraulic systems reducing energy consumption by up to 22%
Automated handling reducing labor costs and improving consistency
Cost control:
Material savings through hot runner systems — ROI typically achieved in 3-6 months at high production volumes
Reduced scrap through process stability and real-time monitoring
Lower energy costs through servo-driven machines
Minimized post-processing through flash control (≤ 0.03mm)
6.8 Quality Control and Assurance
In-process quality control:
First-article inspection — every batch begins with a full dimensional check
In-process inspection — regular sampling throughout the production run
Last-article inspection — verification at the end of each batch
Real-time monitoring — MES-integrated sensors for temperature, pressure, and wall thickness
Final quality assurance:
Full dimensional report — every critical dimension measured and documented
Cpk ≥ 1.33 on all critical dimensions
Material certification — full traceability from raw material to finished part
Visual inspection — surface finish, color consistency, and cosmetic quality
6.9 Packaging and Rapid Delivery
Packaging: Customized packaging solutions protect parts during transit. Options include:
Bulk packaging — for high-volume, cost-sensitive applications
Tray packaging — for automated handling and assembly
Individual packaging — for high-value or cosmetic-critical parts
Delivery: Ansix's integrated manufacturing capabilities enable rapid delivery:
In-house electrode machining and EDM — mold repairs completed within 24 hours
Vertical integration — reduced dependency on external suppliers
Efficient logistics — optimized shipping routes and documentation
Part VII: Industry Experience and Customer Value Proposition
7.1 Cost Reduction Across Three Dimensions
Ansix reduces customer costs through optimization in three key areas:
Cost Dimension Optimization Approach Typical Savings
Material Hot runner systems eliminate cold runner waste; optimized gate design reduces scrap Material utilization increases from 60-70% to 95-98%
Process Cycle time optimization; servo-driven energy efficiency; automated operations 18% cycle time reduction; 22% energy savings
Efficiency 1-cavity-4 configuration maximizes output per machine; reduced post-processing Higher throughput per machine hour; lower labor costs
7.2 Risk Mitigation
DFM reports identify problems before mold construction
T0-T3 trials validate the mold before production commitment
Cpk ≥ 1.33 verification ensures process capability
2,000-shot aging test validates mold durability
3-year structural warranty protects against premature failure
7.3 Capacity and Lead Time Assurance
30-4,000 ton machine fleet covers all product size ranges
In-house manufacturing eliminates external supplier delays
24-hour repair capability minimizes production interruptions
100-500 shot pilot runs validate before scaling
Conclusion
Ansix Tech's 28 years of manufacturing experience, combined with advanced equipment, rigorous quality systems, and a customer-centric approach, position the company as a leader in 45-degree elbow mold manufacturing. The 1-cavity-4 configuration maximizes production efficiency while maintaining exceptional quality consistency.
The Ansix difference is not just in the technology — it's in the translation of technical capability into customer value. Every process, every specification, and every quality check is designed to answer one question: "How does this help our customer succeed?"
From DFM reports that prevent problems before they occur, to Cpk-verified processes that ensure batch-to-batch consistency, to 24-hour repair capability that minimizes downtime — Ansix delivers not just molds, but manufacturing solutions that drive customer profitability.
Ansix Tech Co Ltd
If you have any plans related to 45-degree elbow mold (1-cavity-4) , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #45-degree elbow mold (1-cavity-4) #45-degree elbow mold (1-cavity-4) Material #45-degree elbow mold (1-cavity-4) Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #45-degree elbow mold (1-cavity-4) injection molding #45-degree elbow mold (1-cavity-4) injection tools #45-degree elbow mold (1-cavity-4) injection moulds #45-degree elbow mold (1-cavity-4) plastic mould #45-degree elbow mold (1-cavity-4) plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #45-degree elbow mold (1-cavity-4) injection molding Customized #Ansix mold factory #45-degree elbow mold (1-cavity-4) china #45-degree elbow mold (1-cavity-4) molds #injection factory for 45-degree elbow mold (1-cavity-4) #45-degree elbow mold (1-cavity-4) injection molding #45-degree elbow mold (1-cavity-4) injection molding factory #injection molding company #45-degree elbow mold (1-cavity-4) injection mold companies #45-degree elbow mold (1-cavity-4) Tooling #45-degree elbow mold (1-cavity-4) mold limited #Ansix mold china #Ansix companies for 45-degree elbow mold (1-cavity-4) #Ansix company China #45-degree elbow mold (1-cavity-4) facotry #Ansix Tech #Ansix Tech mould #45-degree elbow mold (1-cavity-4) injection moulding #45-degree elbow mold (1-cavity-4) injection moulding company #Ansix 45-degree elbow mold (1-cavity-4) parts injection mold companies #45-degree elbow mold (1-cavity-4) injection molding companies china #45-degree elbow mold (1-cavity-4) china factory #Ansix moulding companies #Ansix molding company #45-degree elbow mold (1-cavity-4) injection moulding facotry #Ansix Tech mold #45-degree elbow mold (1-cavity-4) mould #45-degree elbow mold (1-cavity-4) plastic injection molding #ansix plastic mold #45-degree elbow mold (1-cavity-4) Mold manufacturing #45-degree elbow mold (1-cavity-4) parts manufacturing #45-degree elbow mold (1-cavity-4) plastic parts factory #45-degree elbow mold (1-cavity-4) injection parts mold #45-degree elbow mold (1-cavity-4) PRECISION MANUFACTURING #45-degree elbow mold (1-cavity-4) TOOL #China 45-degree elbow mold (1-cavity-4) mold #45-degree elbow mold (1-cavity-4) Material injection moulding china #45-degree elbow mold (1-cavity-4) mould china #china precision mold #45-degree elbow mold (1-cavity-4) Material mold in china #45-degree elbow mold (1-cavity-4) mold china #45-degree elbow mold (1-cavity-4) Precision molds #High-precision molds #45-degree elbow mold (1-cavity-4) High-precision tool #Injection molds #45-degree elbow mold (1-cavity-4)Factory #45-degree elbow mold (1-cavity-4)Company #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #45-degree elbow mold (1-cavity-4)Company #45-degree elbow mold (1-cavity-4)Factory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #45-degree elbow mold (1-cavity-4) Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #45-degree elbow mold (1-cavity-4) Large Injection Mold Manufacturer #45-degree elbow mold (1-cavity-4) Plastic Mold Factory #Injection Mold #Plastic Mold