 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


Custom Stethoscope
FEATURES
The "Hard Power" Foundation — Building Customer Trust Through Equipment Excellence
Mold Processing Equipment
Ansix's mold manufacturing facility is equipped with state-of-the-art machinery designed to achieve micron-level precision required for medical device components:
Five-Axis High-Speed Machining Centers: These advanced systems enable machining of complex curved surfaces with an accuracy of 0.002mm, ensuring that product parting lines remain smooth and free from burrs. This precision is critical for stethoscope components where surface finish directly impacts both acoustic performance and user comfort.
Slow-Wire EDM (Electrical Discharge Machining): This technology enables the creation of fine micro-holes and narrow slots down to 0.03mm, essential for intricate stethoscope chestpiece designs and acoustic channels. The precision of slow-wire EDM prevents thin-wall deformation, a common challenge in medical device manufacturing.
Electrode Machining Center and EDM Workshop: Ansix maintains in-house electrode production and EDM capabilities, ensuring that mold repairs and modifications can be completed without outsourcing. This vertical integration reduces turnaround time for mold maintenance and modifications to within 24 hours for routine repairs.
-
Mold Description
Product Materials:
AL ABS/PC
Soft rubber: PVC
Mold Material:
S136ESR
Number of Cavities:
1
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
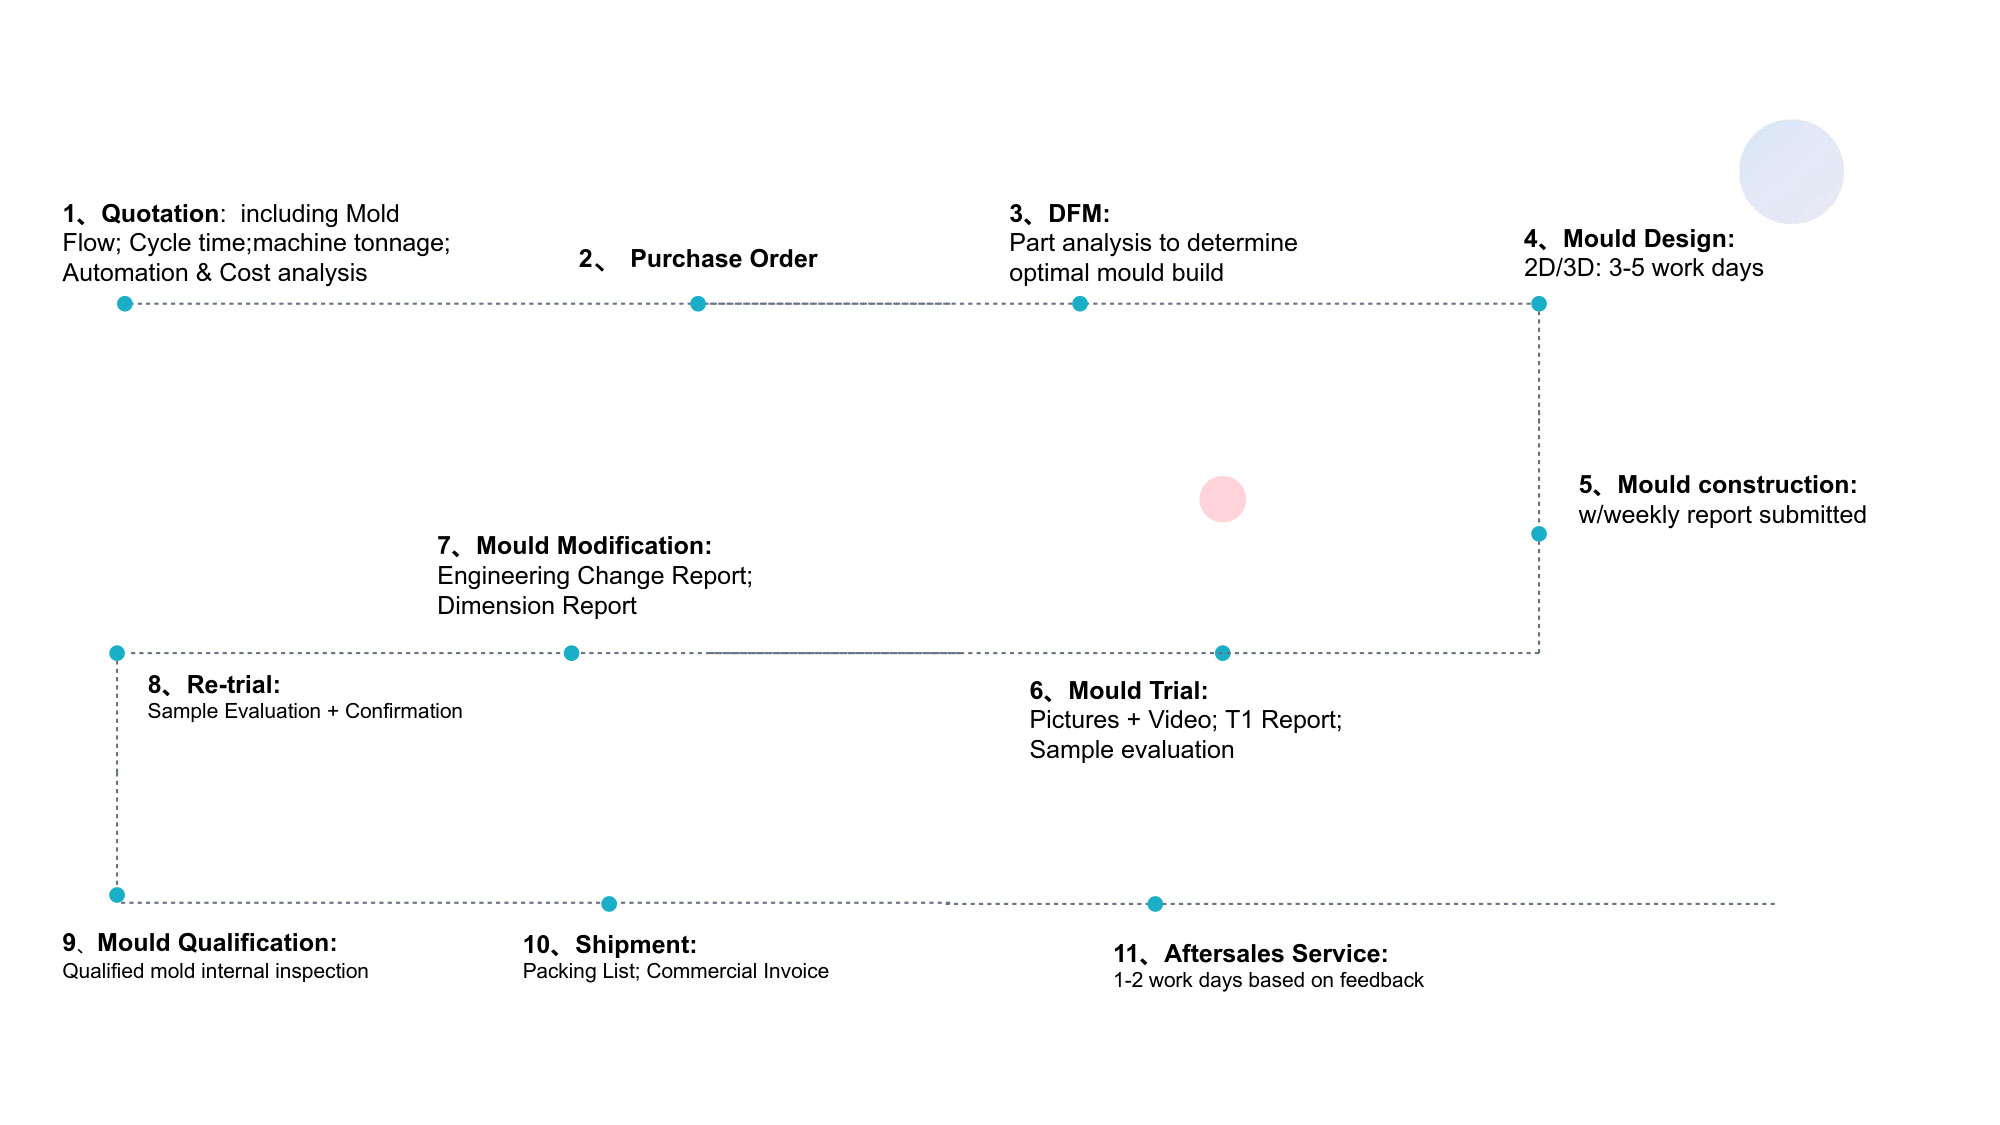
- The mold manufacturing process and product material selection
Injection Molding Machine Fleet
Ansix operates a comprehensive fleet of injection molding machines with clamping forces ranging from 30 tons to 4,000 tons, covering the full spectrum of stethoscope component sizes—from tiny acoustic diaphragms to larger chestpiece housings and tubing connectors.
All-Servo Electric Drive Systems: Every machine in the fleet is equipped with all-servo electric drives, delivering stable repeatability accuracy of ±0.1%. This ensures that every shot—whether the first or the hundred-thousandth—maintains identical dimensional and cosmetic quality.
Real-Time Process Monitoring: All machines are networked to a Manufacturing Execution System (MES) that locks critical process parameters—temperature, pressure, speed, and timing—with access restricted to authorized engineers only. This eliminates unauthorized adjustments and ensures process consistency across production batches.
Inspection and Metrology Equipment
Coordinate Measuring Machines (CMM): Every mold undergoes full-dimensional inspection before delivery. Critical dimensions are verified against CAD models, with comprehensive reports documenting every measured feature.
Optical Inspection Systems: High-resolution optical measurement systems enable rapid, non-contact inspection of complex geometries, ensuring that even the most intricate stethoscope features meet design specifications.
Statistical Process Control: Ansix maintains that for every mold delivered, a full-dimensional comparison report is provided, with Critical Process Capability Index (CPK) values maintained at ≥1.33 for all key dimensions. This ensures that production processes remain stable and capable of consistently meeting specifications.
-
Mold Manufacturing Core Competitiveness — Speaking Through Metrics
Mold Life Expectancy
Customers' primary concern is how long the mold will last before requiring significant maintenance or replacement. Ansix provides clear, data-driven commitments:
Mold Component Material Specification Mold Life Guarantee
Mold Base P20 Structural integrity guaranteed
Core/Cavity S136, 2344, 2343, 8407, SKD11/61, DC53, M340, 4Cr13, 9Cr18, NAK80, H13 500,000 shots with glass-fiber reinforced materials; 1,000,000 shots with standard plastics
Ansix provides material certificates and heat treatment curves for all mold steel, ensuring full traceability and quality verification.
Achievable Tolerances
Component Type Achievable Tolerance
General structural components ±0.05mm
Precision gears and medical-grade components ±0.005mm
This level of precision ensures that stethoscope components fit together seamlessly, maintaining acoustic integrity and patient comfort.
Mold Types and Capabilities
Hot Runner Systems: Reduce material waste by eliminating cold runner scrap, directly lowering per-part material costs while improving cycle efficiency.
Stack Molds: Double production output in the same machine footprint, effectively halving per-part manufacturing costs for high-volume stethoscope components.
Two-Shot/Multi-Material Molds: Enable the production of multi-material stethoscope components—such as soft-touch grips over rigid structural cores—in a single molding cycle, eliminating secondary assembly operations.
High-Gloss Molds: Achieve surface finishes of Ra < 0.05μm, ideal for transparent stethoscope components where optical clarity is essential.
Gate and Feed System Design
Through comprehensive mold flow analysis, Ansix predicts weld line locations, air trap positions, and filling imbalances before steel is cut. This enables:
Optimization of gate count and positioning
Balanced cavity filling
Elimination of aesthetic defects
Reduced scrap rates
Documented Impact: One case study demonstrates that mold flow analysis enabled cycle time reduction from over 60 seconds to just 37.3 seconds, while shot size decreased from 19.72cc to 14.86cc—representing a 38% cycle time improvement and 25% material savings.
Lead Time Standards
Mold Complexity Standard Lead Time Expedited Lead Time*
Simple molds 10 days 7 days
Medium complexity 25-45 days 20 days
High complexity 45-60 days 35 days
*Expedited timelines are achieved through parallel processing without compromising validation steps—all critical verification stages remain fully intact.
Part Three: Injection Molding Process Control — Eliminating Quality Anxiety
Common Customer Concerns and Ansix Solutions
Customer Concern Ansix Solution
Sink marks and shrinkage Mold flow analysis pre-identifies shrinkage-prone areas; process parameters optimized to minimize defects
Flash and burrs 0.005mm fit tolerance on parting surfaces; self-locking clamp force compensation keeps flash below 0.03mm
Dimensional instability Ultrasonic wall thickness sensors provide real-time feedback; automatic compensation of packing pressure
Batch-to-batch color variation Fully automated material handling; closed-loop color monitoring
Process Standardization
Parameter Lockdown: All machine parameters are locked within the MES system. Changes require engineering authorization with full documentation of reasons, approvals, and validation results.
First-Article and Last-Article Inspection: Every production batch begins and ends with full dimensional and cosmetic inspection, ensuring that process drift is detected and corrected immediately.
Dimensional Stability Control
Zone Temperature Control: Ansix employs mold temperature controllers with zone-specific regulation, maintaining core and cavity temperature differences within 2°C. This minimizes warpage and distortion, particularly critical for thin-walled stethoscope components.
Validation Data: For similar bracket-type products, three consecutive production batches over one week demonstrated key hole spacing variation of ≤0.02mm—proving exceptional process stability.
Surface Finish Capabilities
Requirement Achievable Standard
Transparent components No bubbles, no flow marks
Plating-ready components No gas marks
High-gloss surfaces Ra ≤ 0.2μm
Printing/painting compatibility Deformation compensation预留; print registration accuracy ±0.1mm
Special Material Processing Expertise
Ansix has extensive production experience with a wide range of engineering thermoplastics, including:
PC/ABS blends
PC (polycarbonate)
PPS + 40% GF (glass fiber)
PEEK (polyether ether ketone)
PTFE/PFA (fluoropolymers)
PA6 + GF30 (nylon)
PBT (polybutylene terephthalate)
PEI/PPS/LCP (high-performance engineering plastics)
LSR (liquid silicone rubber)
Regulatory Compliance: Components can meet UL94 V-0 flame retardancy ratings for electronic stethoscope housings and demonstrate UV stability (3,000 hours without discoloration) for products requiring long-term environmental exposure.
Part Four: Full-Service Process — Reducing Customer Management Costs
Early Stage Intervention (DFM Reports)
Before any contract is signed, Ansix provides comprehensive Design for Manufacturability (DFM) reports, including:
Draft angle recommendations for optimal mold release
Wall thickness optimization to balance strength and fillability
Gate location analysis to minimize cosmetic defects
Ejector pin mark position allowances
Identification of potential molding challenges
Customer Value: This early intervention prevents costly design revisions after tooling has been cut—saving customers significant time and expense.
Trial Molding and Sampling
T0 to T3 Samples: Ansix provides progressive trial samples from T0 (first shot) through T3 (validated production), with improvement reports accompanying each iteration.
Quick-Change Inserts: The ability to rapidly swap inserts enables validation of different design variations without the cost and time of building entirely new molds.
Pre-Production Validation
Prior to full-scale production, Ansix offers 100-500 shot pilot runs to:
Establish baseline yield rates
Verify process capability indices (CPK)
Confirm stability before committing to mass production
Maintenance and Spare Parts
Spare Parts Package: Critical wear components (ejector pins, core inserts) are delivered with the mold, ensuring immediate availability when replacement becomes necessary.
Scheduled Maintenance: Preventive maintenance at every 200,000 shots, with lifetime repair services available at cost.
Structural Warranty: Three-year structural warranty on molds (excluding normal wear on consumable components).
Part Five: Differentiated Commitments — Direct Solutions to Industry Pain Points
Common Industry Complaint Ansix's Guaranteed Response
Molds require frequent repairs, disrupting orders 2,000-shot aging test before delivery with wear report; 3-year structural warranty
Excessive flash increases post-processing costs 0.005mm parting surface fit tolerance; self-locking clamp force compensation keeps flash ≤0.03mm
Inconsistent dimensions between batches Ultrasonic wall thickness sensors with real-time feedback and automatic pressure compensation; optional in-mold temperature/pressure sensors for closed-loop control
Long mold repair lead times In-house electrode and EDM facilities; most repairs completed within 24 hours
Technical Deep Dive: Custom Stethoscope Mold Manufacturing and Injection Molding Solutions
Product Introduction: Custom Stethoscope Components
Custom stethoscopes consist of multiple precision components, each requiring specific manufacturing approaches:
Chestpiece (Bell and Diaphragm): The acoustic interface between the stethoscope and the patient. These components require precise geometric control to ensure optimal sound transmission. Ansix produces chestpieces through injection molding of engineering thermoplastics or, for premium products, metal injection molding (MIM) where powdered metal is mixed with a polymeric binder to create a feedstock. MIM enables complex geometries with surface roughness (Ra) of ≤1.6 microns in unpolished state.
Y-Connector and Acoustic Tubing: The branching connector that splits sound transmission to both earpieces. These components require tight dimensional control to ensure proper fit with tubing and consistent acoustic performance.
Eartips: Soft, ergonomic components that contact the user's ears. Often manufactured from medical-grade silicone or elastomeric materials through liquid silicone rubber (LSR) molding.
Housings for Electronic Stethoscopes: Enclosures for digital stethoscope electronics, requiring EMI shielding considerations, precise PCB mounting features, and aesthetic surface finishes.
Material Selection for Stethoscope Components
Component Recommended Material Key Properties
Chestpiece (acoustic) PC, ABS, PC/ABS Acoustic damping, impact resistance, dimensional stability
Chestpiece (premium) MIM (17-4PH stainless steel) Superior acoustic properties, premium feel, durability
Y-connector PA6+GF30, PBT Strength, chemical resistance, dimensional stability
Eartips LSR, medical-grade silicone Biocompatibility, comfort, durability
Electronic housing PC/ABS, PPS+40%GF UL94 V-0, dimensional stability, EMI shielding compatibility
Tubing connectors PE, PP, PA Flexibility, chemical resistance, seal integrity
Mold Flow Analysis and DFM
Ansix employs advanced CAE simulation tools to analyze plastic melt flow within the mold cavity. This analysis identifies potential defects before steel is cut:
Weld Line Prediction: Identifies where melt fronts meet, enabling gate placement optimization to position weld lines in non-critical areas.
Air Trap Identification: Locates areas where trapped air may cause burn marks or incomplete filling, guiding vent placement.
Shrinkage Analysis: Predicts sink mark locations and material shrinkage behavior, enabling compensation in mold design.
Cooling Analysis: Optimizes cooling channel placement to ensure uniform cooling and minimize cycle time.
Mold Design Priorities
Parting Line Strategy: For stethoscope components, parting lines must be positioned to minimize aesthetic impact while ensuring clean mold release. Ansix designs 5° draw angles on mold core corners to facilitate smooth ejection.
Cooling System Design: Conformal cooling channels follow the component contour, enabling faster, more uniform cooling. This reduces cycle time and minimizes warpage.
Runner and Gate Design: Hot runner systems minimize material waste, while gate placement is optimized through mold flow analysis to ensure balanced filling and minimal cosmetic defects.
Ejector System: Precision ejector pin placement prevents component deformation during ejection while minimizing visible marks.
Mold Manufacturing Process
1. Steel Selection and Heat Treatment: Based on production volume and material requirements, Ansix selects appropriate tool steels. Heat treatment processes are documented with full temperature curves, ensuring consistent hardness and wear resistance.
2. Rough Machining: Five-axis machining centers remove excess material, establishing the basic mold geometry.
3. Precision Machining: High-speed machining achieves final dimensions with 0.002mm accuracy.
4. EDM (Electrical Discharge Machining): For features inaccessible to cutting tools—fine ribs, narrow slots, complex cavities—EDM provides precision down to 0.03mm.
5. Polishing and Surface Finishing: For high-gloss or transparent components, surfaces are polished to Ra < 0.05μm.
6. Fitting and Assembly: Mold components are fitted with 0.005mm precision on parting surfaces to minimize flash.
7. Trial and Validation: T0 through T3 sampling with full dimensional inspection and process validation.
Injection Molding Process Optimization
Cycle Time Reduction: Through mold flow analysis and process optimization, Ansix has achieved significant cycle time reductions—documented cases showing reduction from 60+ seconds to 37.3 seconds.
Material Efficiency: Shot size optimization reduced material consumption from 19.72cc to 14.86cc in one documented case—a 25% material savings.
Process Parameter Optimization: Systematic experimentation identifies optimal combinations of:
Injection speed and pressure profiles
Packing pressure and duration
Cooling time and temperature
Mold temperature distribution
Automation Integration: Robotic part removal and conveyor systems enable lights-out manufacturing, maximizing machine utilization.
Quality Control and Assurance
Incoming Material Inspection: All raw materials are verified against specifications with full traceability.
In-Process Monitoring:
Shot-to-shot weight monitoring
Dimensional sampling at defined intervals
Visual inspection for cosmetic defects
Final Inspection:
100% critical dimension verification for medical components
Full cosmetic inspection
Functional testing where applicable
Documentation: Full traceability from raw material to finished product, with batch records maintained for regulatory compliance.
Cleanroom Manufacturing: For Class II medical devices such as stethoscopes, Ansix maintains ISO 7 cleanroom capabilities, ensuring product cleanliness and compliance with ISO 13485 standards.
Packaging and Delivery
Protective Packaging: Components are packaged to prevent damage during transit, with options for sterile packaging where required.
Delivery Assurance: With in-house mold maintenance capabilities and robust supply chain management, Ansix maintains on-time delivery rates exceeding industry standards.
Customer Value Summary: What Ansix Delivers
Problem Solving
Customer Problem Ansix Solution
Design not optimized for manufacturing DFM reports identify and resolve issues before tooling
Mold failures disrupting production 2,000-shot validation; 3-year structural warranty
Inconsistent part quality MES-locked parameters; real-time process monitoring
Long lead times for mold repairs In-house repair capability; 24-hour turnaround
High material costs Hot runner systems; optimized shot sizes
Regulatory compliance concerns ISO 13485-compliant processes; full traceability
Cost Savings
Material savings: Up to 25% through shot size optimization and hot runner systems
Cycle time reduction: Up to 38% through process optimization
Reduced post-processing: Flash kept below 0.03mm, eliminating manual deburring
Lower maintenance costs: Extended mold life (500,000-1,000,000 shots)
Reduced inventory costs: Reliable supply chain with consistent quality
Risk Reduction
Design risk: DFM analysis identifies manufacturability issues before tooling
Production risk: Pre-production validation ensures process stability
Quality risk: CPK ≥1.33 for critical dimensions; full traceability
Regulatory risk: ISO 13485-compliant processes and documentation
Supply chain risk: In-house capabilities minimize external dependencies
Conclusion
For Ansix, a mold is not merely a block of steel—it is a precision instrument designed to be a "money-printing machine" for customers. Every design decision—from steel selection and cooling system layout to gate placement and ejector design—is made with the customer's production efficiency, quality requirements, and cost targets in mind.
Ansix's core philosophy: Design the mold with production in mind. When the mold reaches the customer's production floor, it should require no debugging, produce minimal flash, and deliver maximum service life.
The company's 28 years of experience, combined with state-of-the-art equipment, rigorous quality systems, and a customer-centric approach, position Ansix as the preferred partner for custom stethoscope manufacturing—delivering products that meet the highest standards of medical device quality while reducing costs and mitigating risks for customers worldwide.
Ansix Tech Co Ltd
If you have any plans related to Custom stethoscope , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #Custom stethoscope #Custom stethoscope Material #Custom stethoscope Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #Custom stethoscope injection molding #Custom stethoscope injection tools #Custom stethoscope injection moulds #Custom stethoscope plastic mould #Custom stethoscope plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #Custom stethoscope injection molding Customized #Ansix mold factory #Custom stethoscope china #Custom stethoscope molds #injection factory for Custom stethoscope #Custom stethoscope injection molding #Custom stethoscope injection molding factory #injection molding company #Custom stethoscope injection mold companies #Custom stethoscope Tooling #Custom stethoscope mold limited #Ansix mold china #Ansix companies for Custom stethoscope #Ansix company China #Custom stethoscope facotry #Ansix Tech #Ansix Tech mould #Custom stethoscope injection moulding #Custom stethoscope injection moulding company #Ansix Custom stethoscope parts injection mold companies #Custom stethoscope injection molding companies china #Custom stethoscope china factory #Ansix moulding companies #Ansix molding company #Custom stethoscope injection moulding facotry #Ansix Tech mold #Custom stethoscope mould #Custom stethoscope plastic injection molding #ansix plastic mold #Custom stethoscope Mold manufacturing #Custom stethoscope parts manufacturing #Custom stethoscope plastic parts factory #Custom stethoscope injection parts mold #Custom stethoscope PRECISION MANUFACTURING #Custom stethoscope TOOL #China Custom stethoscope mold #Custom stethoscope Material injection moulding china #Custom stethoscope mould china #china precision mold #Custom stethoscope Material mold in china #Custom stethoscope mold china #Custom stethoscope Precision molds #High-precision molds #Custom stethoscope High-precision tool #Injection molds #Custom stethoscopeFactory #Custom stethoscopeCompany #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #Custom stethoscopeCompany #Custom stethoscopeFactory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #Custom stethoscope Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #Custom stethoscope Large Injection Mold Manufacturer #Custom stethoscope Plastic Mold Factory #Injection Mold #Plastic Mold