 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


Engine coolant hose molds are injection molded using GAIM and WIT molding processes
FEATURES
Ansix Tech: Engine Coolant Hose Molds Using GAIM and WIT Molding Processes
A Comprehensive Technical and Commercial Overview
Ansix Tech, established in Hong Kong in 1998, has evolved over more than 28 years into a leading provider of integrated injection molding solutions. With four production bases across China and Vietnam, over 260 injection molding machines, more than 1,200 employees (including over 200 designers), and a total building area exceeding 200,000 m², Ansix Tech has built the industrial infrastructure to deliver engine coolant hose molds using Gas-Assisted Injection Molding (GAIM) and Water Injection Technology (WIT) at world-class standards. The company holds ISO 9001, ISO 14001, IATF 16949, and ISO 13485 certifications, reflecting its commitment to quality, environmental management, and automotive industry standards.
This document provides a comprehensive analysis of how Ansix Tech translates complex technical capabilities in GAIM and WIT molding into tangible customer value—covering equipment infrastructure, mold manufacturing, injection molding process control, full-service lifecycle support, and differentiated competitive advantages.
-
Mold Description
Product Materials:
PA66+GF40
Mold Material:
S136ESR
Number of Cavities:
2
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
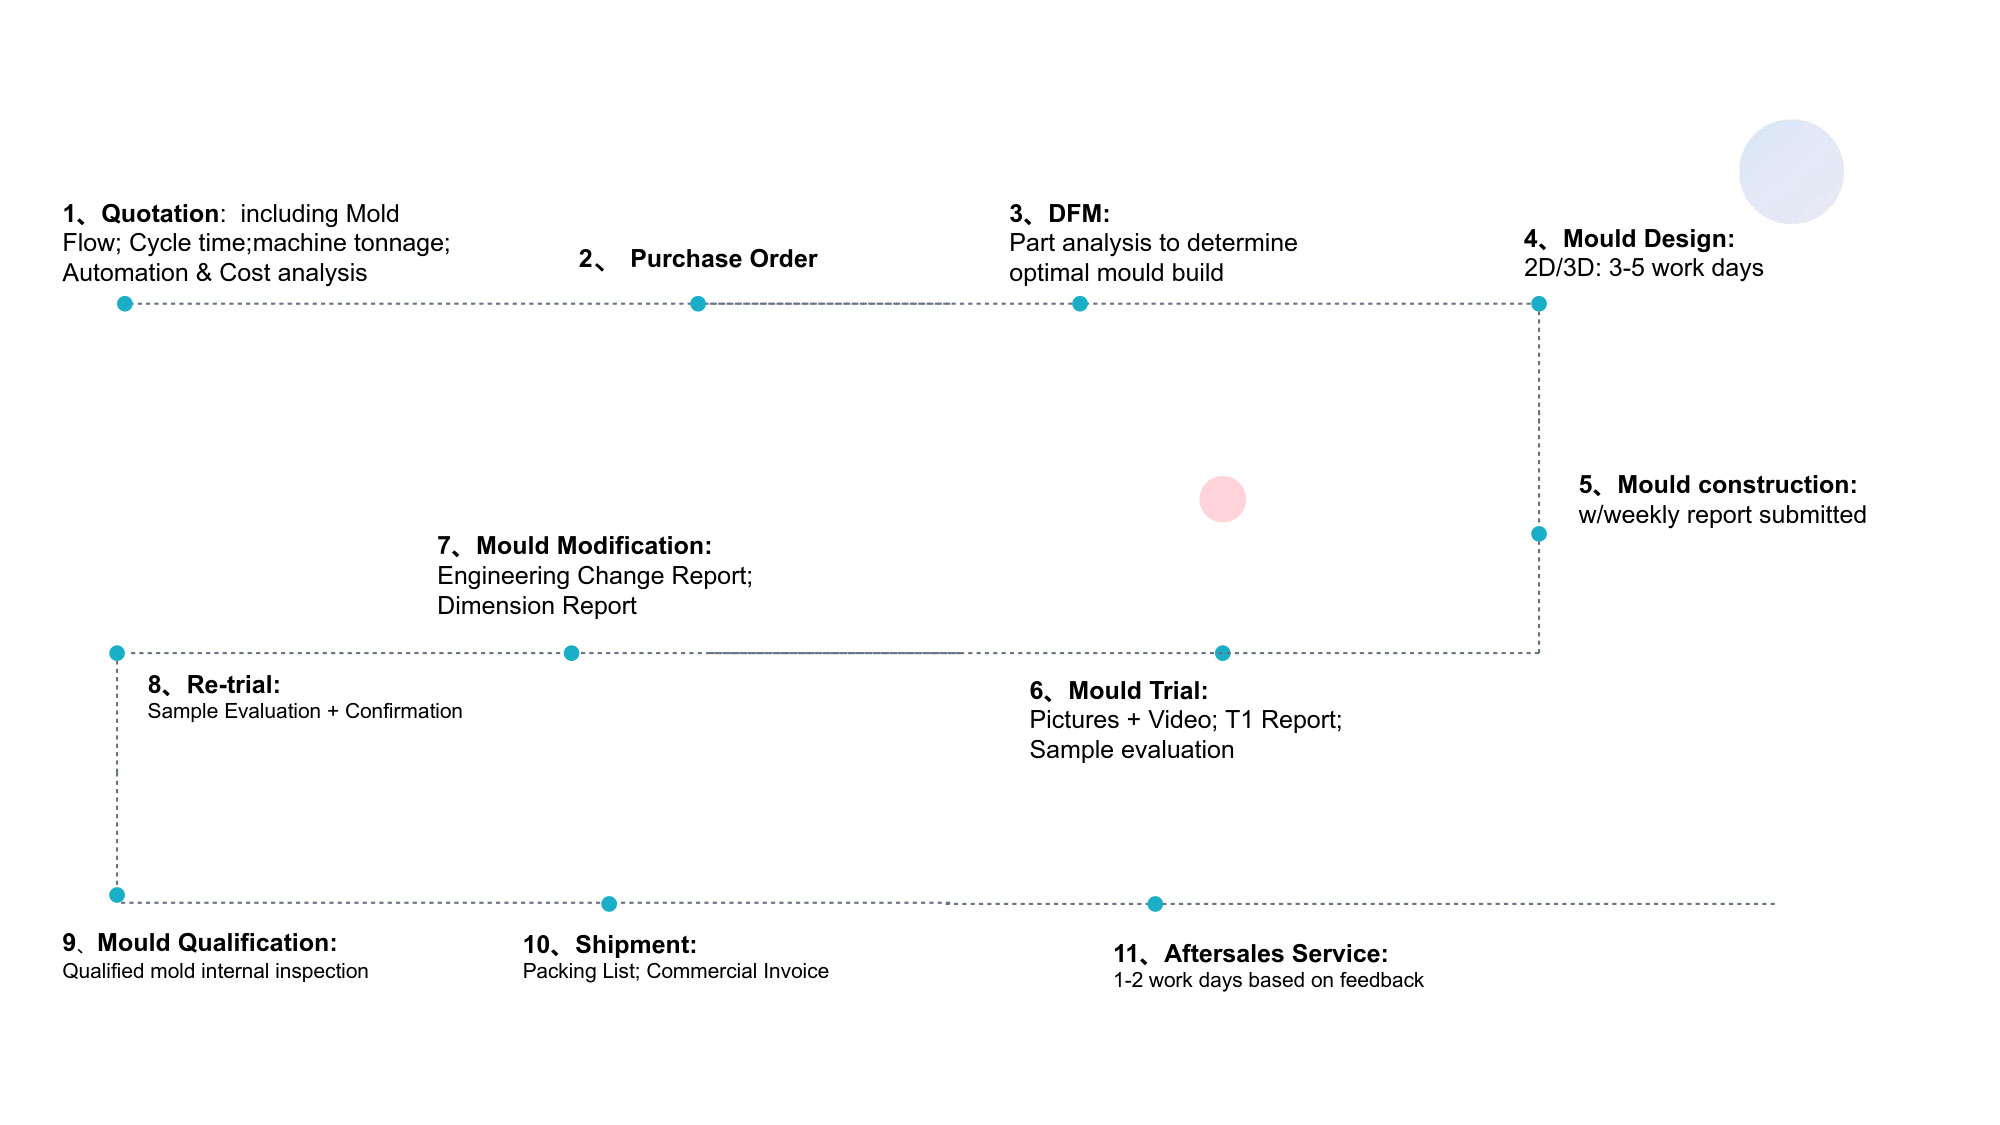
- The mold manufacturing process and product material selection
The "Hard Power" Foundation — Building Customer Trust Through Equipment Excellence
1.1 Mold Manufacturing Equipment
At the heart of Ansix Tech's capability is a state-of-the-art mold workshop equipped with advanced machinery that transforms design concepts into precision tooling.
Five-Axis High-Speed Machining Centers: Ansix Tech operates five-axis high-speed machining centers capable of achieving ±0.002 mm machining accuracy on complex freeform surfaces. For engine coolant hose molds, which often feature curved flow channels, complex parting lines, and intricate core geometries, this precision ensures that parting lines remain smooth and free of burrs—eliminating the need for costly secondary finishing operations. The value to customers: parts that seal perfectly against mating components without leak paths, reducing warranty claims and field failures.
Slow-Wire EDM (Wire Electrical Discharge Machining): The company's slow-wire EDM capabilities enable the production of fine micro-holes and narrow slots down to 0.03 mm, critical for creating gas injection ports in GAIM molds and water injection channels in WIT molds. This capability prevents thin-wall deformation during ejection and ensures that fluid injection points are precisely positioned for optimal hollow-section formation.
Electrode Machining Center and EDM Workshop: Ansix Tech maintains its own electrode machining center and EDM workshop, ensuring that mold repairs and modifications can be completed without outsourcing. For customers, this means conventional repair work can restore production within 24 hours—dramatically reducing downtime compared to suppliers who must ship molds to external repair facilities.
Automated Manufacturing Integration: With an automated machining ratio of 70%, Ansix Tech has built over 30,000 molds since its founding, with an average of only two mold trials per project. This speaks directly to first-pass yield and reduced development costs.
-
Injection Molding Machine Fleet
Ansix Tech's injection molding machine fleet comprises 260 machines with clamping forces ranging from 30 tons to 2,800 tons. This range covers everything from small precision components to large automotive structural parts. The machine fleet includes premium brands: Japan's Fanuc, Sumitomo, Toshiba, Nissei, and Engel, as well as Germany's Arburg (primarily for liquid silicone two-color injection molding) and domestic brands like Haitian and Taichung Precision Machinery.
All-Servo Electric Drive: All machines are equipped with all-servo electric drives, delivering stable repeatability precision of ±0.1%. For engine coolant hose production, this means every shot—across millions of cycles—produces identical parts. The value to customers: parts that assemble consistently, seal reliably, and perform predictably over the product's service life.
GAIM-Capable Machines: Gas-assisted injection molding requires precise control over gas injection timing, pressure, and volume. Ansix Tech's machines are equipped with the necessary gas injection systems and control interfaces to execute GAIM processes reliably.
WIT-Capable Machines: Water injection technology, developed at IKV Aachen, Germany, uses water instead of gas to form hollow sections. Water's thermal conductivity is 40 times that of gas, and its heat capacity is four times greater, enabling cooling time reductions of 25-40%. Ansix Tech's WIT-capable machines deliver these benefits consistently.
1.3 Inspection and Quality Assurance Equipment
Coordinate Measuring Machines (CMM): Every mold undergoes full dimensional inspection before shipment, with critical dimensions verified to CPK ≥ 1.33. A CPK of 1.33 represents Six Sigma-equivalent capability, statistically ensuring that 99.9937% of production parts conform to specifications. For automotive-grade critical dimensions, Ansix Tech consistently achieves CPK ≥ 1.67—the standard demanded by global OEMs.
Optical Measurement Equipment: Complementing CMM inspection, optical measurement systems provide non-contact dimensional verification, particularly valuable for complex curved surfaces and delicate features that cannot tolerate contact measurement forces.
Full Dimensional Reporting: Every mold is delivered with a complete dimensional inspection report, with key features validated against the original CAD model. This documentation provides customers with auditable proof of quality, eliminating uncertainty and enabling confident production planning.
Section II: Mold Manufacturing Core Competitiveness — Speaking Through Specific Metrics
2.1 Mold Life Expectancy
Customers' foremost concern is how many shots a mold will deliver before requiring maintenance or replacement. Ansix Tech addresses this with clear, material-specific commitments:
Mold Component Material Options Application Guaranteed Life
Mold Base P20 Structural support N/A (reusable)
Cavity/Core (Standard) S136 (420 stainless) General purpose, corrosion-resistant 500,000+ shots
Cavity/Core (Premium) 2344, 8407, H13 High-wear, high-cycle applications 500,000 - 1,000,000 shots
Cavity/Core (Abrasive Materials) 2343, SKD11/61, DC53 Glass-filled or mineral-filled plastics 400,000 - 600,000 shots
Cavity/Core (High Polish) NAK80, M340 Transparent or high-gloss applications 500,000+ shots
These steel selections are made based on material compatibility and production volume. For glass-filled materials (common in engine coolant hose applications), Ansix Tech guarantees 500,000 shots with appropriate tool steel selection. For standard engineering plastics, the guarantee extends to 1,000,000 shots.
Customer Value: A mold that runs 500,000 to 1,000,000 shots without major maintenance means predictable production costs, reduced capital expenditure on replacement tooling, and uninterrupted supply to your customers.
2.2 Achievable Tolerances
Component Type Achievable Tolerance Customer Benefit
General Structural Components ±0.05 mm Reliable assembly, consistent function
Precision Gears / Medical Components ±0.005 mm Interchangeable parts, zero assembly issues
Ansix Tech provides mold steel material certificates and heat treatment curves upon request, giving customers full traceability and confidence in material properties.
2.3 Mold Types Offered
Hot Runner Systems: Reducing material waste by eliminating the cold runner, hot runner systems directly lower per-part material costs. For high-volume engine coolant hose production, this translates to significant annual savings.
Stack Molds: Doubling production efficiency from a single injection molding machine, stack molds effectively halve the per-part machine time cost.
Two-Color / Multi-Material Molds: Enabling the production of components with multiple materials in a single molding cycle, these molds eliminate assembly operations and improve part performance.
High-Gloss / Mirror-Finish Molds: Achieving surface roughness Ra < 0.05 μm, these molds are essential for transparent applications where optical clarity is required.
2.4 Gate and Runner System Optimization
Through comprehensive Moldflow CAE simulations, Ansix Tech predicts weld line locations, gas trap positions, and fill imbalances before any steel is cut. The company optimizes gate quantity and placement to ensure balanced filling, eliminating short shots, burns, and cosmetic defects.
Customer Value: No surprise defects during production trials. First-shot success reduces development time and cost.
2.5 Lead Time Standards
Mold Complexity Standard Lead Time Expedited Lead Time
Simple Molds 10 days —
Medium Complexity 25-45 days 20 days (with validation rigor maintained)
High Complexity 45-60 days 30-35 days
For expedited deliveries, Ansix Tech maintains all validation steps—ensuring that speed does not come at the cost of quality.
Section III: Injection Molding Process Control — Eliminating Quality Anxiety
3.1 Process Standardization
Every Ansix Tech injection molding machine is networked and integrated into the MES (Manufacturing Execution System). All molding parameters—temperature, pressure, speed, and time—are locked into the system. Only authorized engineers can adjust parameters, and every batch undergoes first-article and last-article inspection.
Customer Value: You receive identical parts on every shipment, regardless of when the order is placed. No surprises, no production line stoppages due to dimensional drift.
3.2 Dimensional Stability Control
Engine coolant hoses must seal against fluids under pressure and temperature extremes. Dimensional stability is non-negotiable.
Mold Temperature Control: Ansix Tech equips molds with zone-controlled mold temperature controllers, maintaining core and cavity temperature differences within 2°C. This minimizes warpage and distortion.
Real-Time Wall Thickness Monitoring: Ultrasonic thickness sensors provide real-time feedback on wall thickness variations, automatically compensating holding pressure to maintain consistency.
Closed-Loop Control: In-cavity temperature and pressure sensors enable closed-loop control, automatically adjusting process parameters to maintain part quality even as environmental conditions change.
Demonstrated Performance: For similar bracket components produced over three consecutive weeks, critical hole spacing variation was maintained within ±0.02 mm—statistical proof of process capability.
3.3 Cosmetic Appearance Grades
Requirement Achievable Standard Application
Transparent Parts No bubbles, no flow lines Fluid level windows, sight glasses
Plated Parts No gas marks Decorative or functional plated surfaces
High-Gloss Parts Surface roughness Ra ≤ 0.2 μm Visible exterior surfaces
Printed / Painted Parts Registration accuracy ±0.1 mm (with deformation compensation) Branding, part marking
3.4 Special Material Capabilities
Ansix Tech has extensive production experience with a wide range of engineering and high-performance materials:
Material Category Specific Grades Key Properties
Engineering Blends PC/ABS Impact resistance, dimensional stability
High-Heat PC (Polycarbonate) Heat resistance, transparency
Glass-Filled PPS + 40% GF, PA6 + GF30, PBT Strength, stiffness, thermal stability
High-Performance PEEK, PEI, PPS, LCP Extreme temperature, chemical resistance
Fluoropolymers PTFE, PFA Chemical resistance, low friction
Elastomers Liquid Silicone Rubber (LSR) Flexibility, sealing
Flame Retardancy: Ansix Tech produces components meeting UL94 V-0 ratings for applications requiring fire safety.
Weathering Resistance: Parts pass UV testing at 3,000 hours without color change—critical for engine compartment components exposed to heat and UV.
Section IV: Full-Service Lifecycle Support — Reducing Total Cost of Ownership
4.1 Early-Stage Design Intervention (DFM Reports)
Before any steel is cut, Ansix Tech provides a comprehensive Design for Manufacturability (DFM) report. This report covers:
Draft angle recommendations (ensuring clean ejection)
Wall thickness optimization (balancing strength, cooling, and material usage)
Gate location selection (optimizing fill and minimizing cosmetic defects)
Ejector pin mark location allowances (hiding cosmetic imperfections)
Shrinkage compensation (ensuring final dimensions match specifications)
Customer Value: Problems are identified and solved on the computer, not on the production floor. This prevents the costly cycle of "build, test, fail, modify, repeat."
4.2 Trial Molding and Sampling
Ansix Tech provides T0 through T3 sampling rounds, with each iteration accompanied by a detailed improvement report. The company can quickly replace inserts to validate different design approaches without rebuilding the entire mold.
Customer Value: Rapid design iteration without prohibitive tooling costs. You see physical parts early and can make informed decisions.
4.3 Low-Volume Production Validation
Before committing to full-scale mass production, Ansix Tech offers 100- to 500-shot pilot runs. During these runs, the company:
Calculates yield rates
Validates CPK for critical dimensions
Confirms process stability
Identifies and resolves any remaining issues
Customer Value: You approve production only when statistical evidence proves the process is capable. No costly surprises during mass production.
4.4 Maintenance and Spare Parts
Spare Parts Kit: Each mold is delivered with a complete set of spare wear parts (ejector pins, core inserts).
Scheduled Maintenance: Ansix Tech recommends maintenance intervals every 200,000 shots, extending mold life and preventing unplanned downtime.
Lifetime Repair: Mold repairs are provided at cost for the life of the tool.
In-House Repair Capability: Because Ansix Tech maintains its own electrode and EDM facilities, mold repairs typically restore production within 24 hours.
Section V: Differentiated Competitive Advantages — Addressing Common Pain Points
5.1 Direct Responses to Common Customer Complaints
Customer Complaint Ansix Tech's Response Customer Value
"Molds require frequent repairs, disrupting orders." 2,000-shot aging test before delivery, with wear report provided. Three-year structural warranty on mold (excluding normal consumable wear). Predictable production, reduced maintenance costs.
"Excessive flash requires expensive secondary deburring." Parting line machining to 0.005 mm fit precision. Self-locking clamp force compensation ensures flash controlled to <0.03 mm per batch. Eliminates secondary finishing operations.
"Dimensions vary from batch to batch." Ultrasonic wall thickness sensors with real-time holding pressure compensation. In-cavity temperature and pressure sensors for closed-loop control. Consistent parts, zero assembly line stoppages.
"Mold repairs take too long." In-house electrode and EDM facilities. Routine repairs restore production within 24 hours. Minimal production downtime.
5.2 The "Money Printer" Philosophy
As Ansix Tech states: "For us, a mold is not a block of steel—it is a revenue generator for our clients."
This philosophy drives every design decision. When designing a mold, Ansix Tech simultaneously plans:
Mold flow balance: Ensuring even filling and minimal stress
Venting strategy: Preventing gas traps and burn marks
Thermal balance: Achieving uniform cooling and minimizing cycle time
Ejection system design: Ensuring reliable, damage-free part removal
The result is a mold that arrives at your production line ready to run—no调试, minimal flash, and maximum lifespan.
5.3 GAIM and WIT-Specific Advantages for Engine Coolant Hoses
GAIM (Gas-Assisted Injection Molding) : Gas-assisted injection molding involves injecting high-pressure inert gas (typically nitrogen) into the melt after partial fill. The gas penetrates the melt core, forming a hollow section. For engine coolant hoses, GAIM delivers:
Material savings of 15-30% per part
Cycle time reduction of 30-50% due to faster cooling of hollow sections
Clamp tonnage reduction of up to 70% , enabling use of smaller machines
Elimination of sink marks and warpage through uniform gas pressure
Deformation reduction of up to 31.3% compared to conventional methods
WIT (Water Injection Technology) : Water-assisted injection molding uses water instead of gas to form hollow sections. Water's thermal conductivity is 40 times that of gas, and its heat capacity is four times greater. For engine coolant hoses, WIT delivers:
Cooling time reduction of 25-40% compared to GAIM
Thinner and more uniform wall thickness , reducing part weight
Lower system cost through reduced cycle times
Section VI: Material Selection and Characteristics
6.1 Raw Material Selection for Engine Coolant Hoses
Engine coolant hoses must withstand:
Temperature extremes: From sub-zero cold starts to 120°C+ operating temperatures
Chemical exposure: Coolant (ethylene glycol/water mixtures), oils, and fuels
Pressure cycling: Repeated pressurization and depressurization
Vibration and movement: Engine vibration and thermal expansion/contraction
Common Materials:
Material Key Properties Typical Applications
PA6 + GF30 High strength, good heat resistance, chemical resistance Structural hose connectors, fittings
PPS + 40% GF Excellent heat resistance, chemical resistance, dimensional stability High-temperature coolant system components
PBT Good chemical resistance, dimensional stability, electrical properties Electrical connectors in cooling systems
PC/ABS Impact resistance, dimensional stability, good cosmetic appearance Housings, covers, visible components
PEEK Extreme temperature resistance, chemical resistance, high strength High-performance, extreme-environment applications
6.2 Material Certifications and Traceability
Ansix Tech provides:
Material certificates of analysis (confirming composition and properties)
Heat treatment curves (confirming proper material processing)
Full traceability from raw material receipt to finished part
Section VII: Design and Development Process
7.1 Mold Flow Analysis (DFM)
Before any steel is cut, Ansix Tech performs comprehensive Moldflow CAE simulations:
Fill analysis: Predicting melt front progression, identifying weld lines and gas traps
Packing analysis: Optimizing holding pressure to minimize shrinkage and sink marks
Cooling analysis: Designing cooling channels for uniform temperature distribution
Warpage analysis: Predicting and compensating for post-molding distortion
Customer Value: Problems are identified and solved virtually, eliminating the costly cycle of physical trial-and-error.
7.2 Mold Design Priorities
For engine coolant hose molds using GAIM and WIT, design priorities include:
Cooling System Design: Conformal cooling channels follow the part contour, ensuring uniform cooling and minimizing cycle time.
Runner and Gate System Design: Optimized for balanced filling, minimal pressure drop, and clean part separation.
Ejection System Design: Reliable, damage-free part removal with ejector pin marks located in non-cosmetic areas.
Gas/Water Injection System Design: Precise positioning of gas/water injection points for optimal hollow section formation.
7.3 Manufacturing Process Flow
Design and DFM: CAD modeling, mold flow analysis, DFM report
Steel Procurement: Material selection, certification, heat treatment
Rough Machining: CNC milling, turning
Heat Treatment: Hardening, tempering (as required)
Precision Machining: Five-axis machining, EDM, wire EDM
Fit and Assembly: Component fitting, mold assembly
Validation: T0-T3 sampling, dimensional inspection, CPK verification
Delivery: Full documentation, spare parts kit
Section VIII: Quality Assurance and Process Control
8.1 Statistical Process Control (SPC)
Every production batch undergoes comprehensive dimensional inspection using CMM and optical measurement equipment. Critical dimensions are monitored to CPK ≥ 1.33.
8.2 Quality Management System
Ansix Tech's quality management system integrates:
Incoming inspection: Raw material verification
In-process inspection: Real-time monitoring during production
Final inspection: Full dimensional verification before shipment
Documentation: Complete traceability from raw material to finished part
8.3 Industry Certifications
Certification Scope
ISO 9001 Quality Management Systems
ISO 14001 Environmental Management
IATF 16949 Automotive Industry Quality Management
ISO 13485 Medical Device Quality Management
Section IX: Cost Reduction Strategies
9.1 Material Cost Reduction
GAIM material savings: 15-30% reduction per part through hollow-section formation
Hot runner systems: Eliminating cold runner waste
Strategic material sourcing: Engineering-grade materials at competitive prices
9.2 Process Efficiency Improvements
Cycle time reduction: 30-50% with GAIM, 25-40% with WIT
Machine utilization: Lower clamp tonnage requirements (up to 70% reduction with GAIM)
Automation: 70% automated machining ratio
9.3 Elimination of Secondary Operations
No flash: Parting line precision eliminates deburring
No secondary finishing: Consistent cosmetic quality from the mold
Part consolidation: Multiple components combined into single GAIM parts, eliminating assembly
9.4 Total Cost of Ownership Reduction
Cost Category Savings Mechanism Estimated Savings
Material GAIM hollow section, hot runner 15-30%
Machine Time Faster cycles, lower tonnage 25-50%
Labor Automation, eliminated secondary ops 20-40%
Maintenance Longer mold life, in-house repairs 30-50%
Scrap/Rework CPK ≥ 1.33 process capability >99.99% yield
Section X: Delivery and After-Sales Service
10.1 Delivery Commitments
Standard delivery: As per complexity (10-60 days)
Expedited delivery: Available on request (validation rigor maintained)
Documentation: Full dimensional reports, material certificates, CPK data
10.2 After-Sales Support
Spare parts kit: Included with every mold delivery
Technical support: 12-hour response time to inquiries
Global service network: Service points in Europe, North America, and South America
Lifetime repair: Repairs provided at cost for mold life
10.3 Customer Partnership Philosophy
As Ansix Tech states: "When convenient, we invite you to experience a full DFM report walk-through on one of your existing products—allowing you to see firsthand how we proactively eliminate weld lines, gas traps, shrinkage, and other risks."
Conclusion
Ansix Tech's capability in producing engine coolant hose molds using GAIM and WIT molding processes is built on a foundation of:
World-class equipment: Five-axis machining, EDM, CMM, and 260 injection molding machines
Technical expertise: 28+ years, 30,000+ molds delivered, 1,200+ employees
Process control: CPK ≥ 1.33, MES-integrated process control, closed-loop systems
Material science: Comprehensive material selection and certification
Cost optimization: 15-30% material savings, 25-50% cycle time reduction
Full-service support: DFM to delivery to lifetime maintenance
For customers seeking a partner who can deliver engine coolant hose molds that run reliably, produce consistent parts, and minimize total cost of ownership, Ansix Tech offers a compelling value proposition—one where technical excellence is consistently translated into measurable business outcomes.
Ansix Tech Co Ltd
If you have any plans related to Engine coolant hose molds are injection molded using GAIM and WIT molding processes , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #Engine coolant hose molds are injection molded using GAIM and WIT molding processes #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Material #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection molding #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection tools #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection moulds #Engine coolant hose molds are injection molded using GAIM and WIT molding processes plastic mould #Engine coolant hose molds are injection molded using GAIM and WIT molding processes plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection molding Customized #Ansix mold factory #Engine coolant hose molds are injection molded using GAIM and WIT molding processes china #Engine coolant hose molds are injection molded using GAIM and WIT molding processes molds #injection factory for Engine coolant hose molds are injection molded using GAIM and WIT molding processes #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection molding #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection molding factory #injection molding company #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection mold companies #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Tooling #Engine coolant hose molds are injection molded using GAIM and WIT molding processes mold limited #Ansix mold china #Ansix companies for Engine coolant hose molds are injection molded using GAIM and WIT molding processes #Ansix company China #Engine coolant hose molds are injection molded using GAIM and WIT molding processes facotry #Ansix Tech #Ansix Tech mould #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection moulding #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection moulding company #Ansix Engine coolant hose molds are injection molded using GAIM and WIT molding processes parts injection mold companies #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection molding companies china #Engine coolant hose molds are injection molded using GAIM and WIT molding processes china factory #Ansix moulding companies #Ansix molding company #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection moulding facotry #Ansix Tech mold #Engine coolant hose molds are injection molded using GAIM and WIT molding processes mould #Engine coolant hose molds are injection molded using GAIM and WIT molding processes plastic injection molding #ansix plastic mold #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Mold manufacturing #Engine coolant hose molds are injection molded using GAIM and WIT molding processes parts manufacturing #Engine coolant hose molds are injection molded using GAIM and WIT molding processes plastic parts factory #Engine coolant hose molds are injection molded using GAIM and WIT molding processes injection parts mold #Engine coolant hose molds are injection molded using GAIM and WIT molding processes PRECISION MANUFACTURING #Engine coolant hose molds are injection molded using GAIM and WIT molding processes TOOL #China Engine coolant hose molds are injection molded using GAIM and WIT molding processes mold #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Material injection moulding china #Engine coolant hose molds are injection molded using GAIM and WIT molding processes mould china #china precision mold #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Material mold in china #Engine coolant hose molds are injection molded using GAIM and WIT molding processes mold china #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Precision molds #High-precision molds #Engine coolant hose molds are injection molded using GAIM and WIT molding processes High-precision tool #Injection molds #Engine coolant hose molds are injection molded using GAIM and WIT molding processesFactory #Engine coolant hose molds are injection molded using GAIM and WIT molding processesCompany #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #Engine coolant hose molds are injection molded using GAIM and WIT molding processesCompany #Engine coolant hose molds are injection molded using GAIM and WIT molding processesFactory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Large Injection Mold Manufacturer #Engine coolant hose molds are injection molded using GAIM and WIT molding processes Plastic Mold Factory #Injection Mold #Plastic Mold

- PA66+GF40 TDS