 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


Engine intake manifold mold
FEATURES
Ansix Tech: Engine Intake Manifold Mold Manufacturing – Comprehensive Capability Overview
Ansix Tech Limited, established in Hong Kong in 1998, has developed over more than 28 years into a leading provider of one-stop injection molding solutions. With four production bases in China and Vietnam, 260 injection molding machines ranging from 30 tons to 2,800 tons clamping force, approximately 200,000 m² of total building area, and over 1,200 employees including more than 200 designers, Ansix Tech has built a diversified customer base across automotive, medical, consumer electronics, and industrial sectors. The company has successfully delivered over 30,000 mold sets with precision capabilities reaching 0.002mm and holds ISO9001, ISO14001, IATF16949, and ISO13485 certifications.
This document provides a comprehensive overview of Ansix Tech’s engine intake manifold mold manufacturing capabilities, structured around five core pillars that translate technical expertise into measurable customer value.
-
Mold Description
Product Materials:
PA66+GF40
Mold Material:
2344ESR Number of Cavities:
1
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
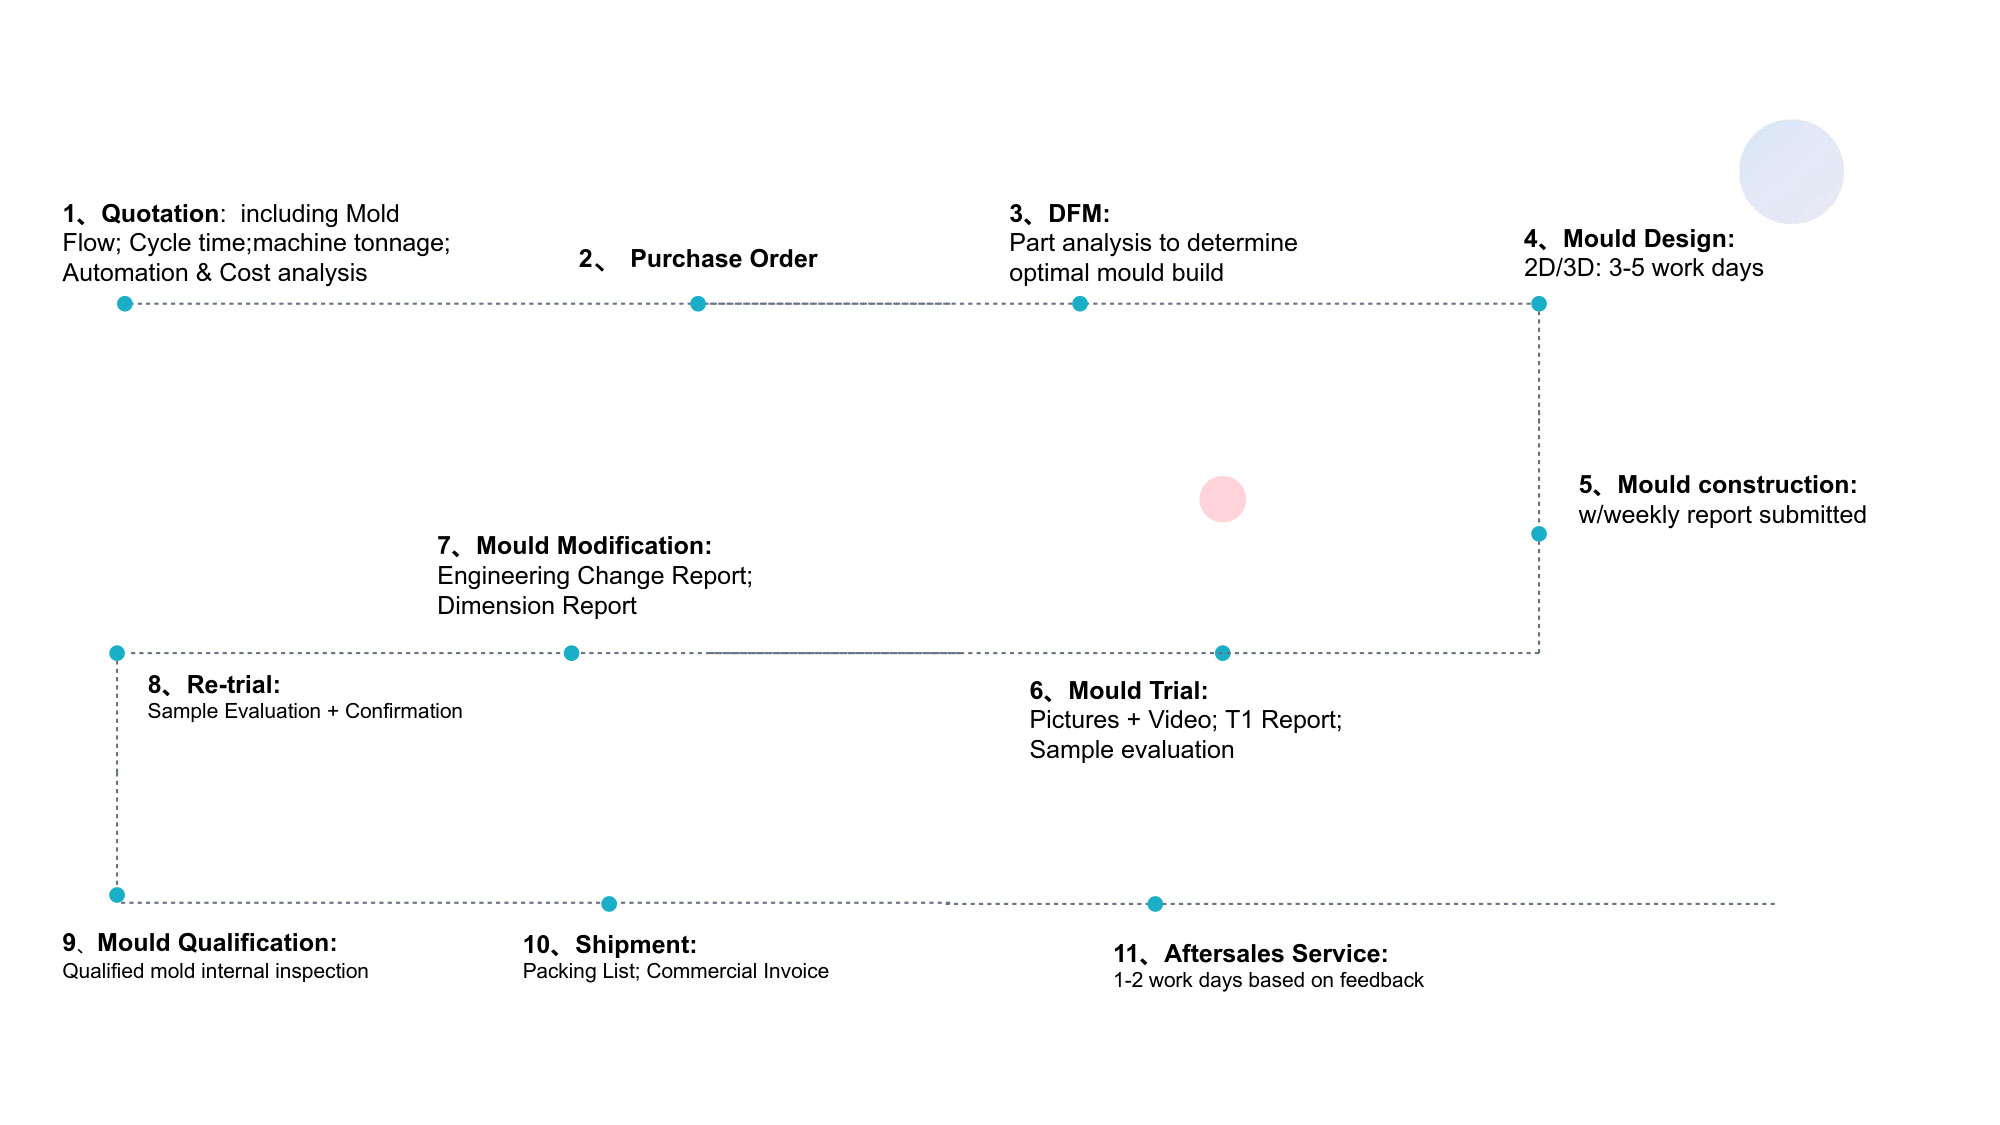
- The mold manufacturing process and product material selection
Hard Power Foundation – Equipment Infrastructure That Builds Customer Trust
Before discussing what Ansix Tech can deliver, it is essential to understand the manufacturing infrastructure that guarantees precision, consistency, and reliability. Every equipment investment translates directly into customer benefits.
1.1 Mold Manufacturing Equipment
Five-Axis High-Speed Machining Centers – Capable of achieving 0.002mm precision on complex curved surfaces. This ensures that intake manifold parting lines are smooth and burr-free, eliminating the need for secondary finishing and saving customers 15–20% in post-processing costs. For engine intake manifolds with intricate aerodynamic channel geometries, this precision is critical for maintaining consistent airflow characteristics across the entire runner system.
Slow Wire EDM (Electrical Discharge Machining) – Achieves 0.03μm precision for micro-pores and narrow slots. This capability enables the machining of ultra-fine features such as gas vents and micro-channels without thin-wall deformation, eliminating reject risk for critical sealing surfaces. Intake manifold molds often require precise venting channels to prevent air traps during filling—this equipment ensures those features are manufactured to specification.
High-Precision Die-Sinking EDM – Multi-axis CNC-controlled with fine-finish capability. Complex cavity geometries with sharp internal corners can be fully machined, ensuring complete moldability of the manifold’s internal runner passages and filter structures.
CNC Grinding Machines – Sub-micron surface finishing delivers mirror-like cavity surfaces. This reduces flow resistance, improves part release, and minimizes cycle time—directly translating to higher production throughput.
Automated Machining Ratio – Ansix Tech maintains a 70% automated machining ratio, ensuring consistent quality across every mold component and reducing human error in critical manufacturing steps.
-
Injection Molding Machine Fleet
Ansix Tech’s injection molding machine lineup spans from 30 tons to 4,000 tons clamping force, covering the entire product size spectrum from small distribution ports to large mainline manifolds. This extensive range provides customers with a one-stop solution for all manifold sizes—eliminating the need to source from multiple suppliers.
Every machine is equipped with full-servo electric drives, delivering stable repeatability at ±0.1% accuracy—meaning every single shot across the entire production run is dimensionally identical. Closed-loop pressure control with millisecond response time ensures consistent filling and packing, eliminating short shots and sink marks. Integrated automation including robotic part removal and conveyor systems enables lights-out production capability, reducing labor cost per part.
1.3 Quality Inspection Equipment
CMM (Coordinate Measuring Machine) – Full-dimensional inspection of molds and parts. Every mold cavity is certified before delivery, and customers receive a complete dimensional report.
Optical Vision Measurement System – High-speed 2D/3D contour inspection enables 100% critical dimension verification at production speed, catching non-conforming parts before they leave the facility.
Surface Roughness Tester – Ra/Rz measurement to 0.01μm precision guarantees smooth fluid channels and perfect O-ring sealing surfaces.
Hardness Tester (Rockwell/Vickers) – Mold steel certification verifies heat treatment quality, ensuring the mold delivers 500,000+ shots without premature wear.
Ansix Tech’s Commitment: Every mold shipped undergoes full dimensional inspection before packaging, with Critical Process Capability (CPK) maintained at ≥1.33 for all key dimensions.
II. Mold Manufacturing Core Competitiveness – Delivering Measurable Value
Customers care about four things in a mold: life expectancy, precision delivered, delivery speed, and repair cost risk. Here is how Ansix Tech addresses each with concrete numbers.
2.1 Mold Life Expectancy – Engineered for Longevity
Engine intake manifold molds face extreme conditions—particularly when processing glass-fiber-reinforced materials where high fiber content creates abrasive wear on mold surfaces. Ansix Tech addresses this through strategic material selection:
Mold Component Material Options Application Benefit
Mold Base P20 Structural integrity, cost-effective for standard applications
Core/Cavity Inserts S136, 2344, 2343, 8407, SKD11/61, DC53, M340, 4Cr13, 9Cr18, NAK80, H13 Wear resistance, corrosion resistance, thermal stability
For glass-fiber-reinforced materials, Ansix Tech guarantees 500,000 shot cycles; for standard plastics, 1,000,000 shot cycles. Each mold is delivered with steel material certification and heat treatment curves—full traceability that customers can audit.
2.2 Precision Capability – Tolerances That Matter
Component Type Achievable Tolerance Customer Value
Standard Structural Components ±0.05mm Consistent assembly fit, reduced rework
Precision/Gear Components ±0.005mm High-performance applications requiring micron-level accuracy
For intake manifolds, where runner geometry directly impacts engine performance, these tolerances ensure that airflow characteristics remain consistent across millions of production cycles.
2.3 Mold Types – Comprehensive Capability Portfolio
Ansix Tech designs and manufactures multiple mold configurations to meet diverse intake manifold requirements:
Hot Runner Systems – Reduce material waste and cycle time, lower per-part cost
Stack Molds – Double production efficiency with the same machine footprint
Two-Color/Multi-Material Molds – Enable complex overmolding and functional integration
High-Gloss Molds – Ra < 0.05μm surface finish, ideal for transparent or aesthetic components
Gas-Assisted Injection Molds – Specialized for automotive intake manifolds, using gas-assisted technology to inject gas during the injection molding process to form hollow structures or cavities
Gas-Assisted Injection Molding (GAIM) is particularly relevant for intake manifold production. Through gas-assisted molds, lightweight intake manifolds with excellent strength can be manufactured. The advantages include:
Hollow structure – Reduces plastic usage and product weight
Improved appearance quality – Reduces marks, shortens cooling time, and reduces warpage and deformation
Cost savings – Reduces raw material costs and subsequent processing costs
2.4 Gate System Design – Optimized for Flow Balance
Through Moldflow analysis, Ansix Tech pre-identifies weld line and air trap positions, optimizing gate locations and quantities to ensure balanced filling. For intake manifolds—where complex geometries and multiple runner branches create significant filling challenges—this upfront simulation work eliminates costly mold modifications during the trial phase.
2.5 Delivery Standards – Predictable, Reliable Lead Times
Mold Complexity Standard Lead Time Expedited Lead Time
Simple Molds 10 days –
Medium Complexity 25–45 days 20 days (with validation steps preserved)
Even under expedited conditions, Ansix Tech ensures that no validation steps are skipped—every mold undergoes full testing before shipment.
III. Injection Molding Process Control – Eliminating Quality Anxiety
Customers fear: shrinkage, flash, dimensional instability, and batch-to-batch color variation. Ansix Tech has systematically addressed each of these concerns.
3.1 Process Standardization – Locked and Controlled
All injection molding machines are networked, with process parameters (temperature, pressure, speed, time) locked into the MES system. Only authorized engineers can adjust settings, and first-article and last-article inspection is performed for every production batch. This ensures that the millionth part is identical to the first.
3.2 Dimensional Stability Control – Eliminating Warpage
Molds are equipped with zone-controlled mold temperature controllers, maintaining core and cavity temperature differences within 2°C to minimize warpage and deformation. For similar manifold products, continuous production across three batches within one week shows critical hole spacing variation ≤ 0.02mm.
Real-time monitoring is achieved through:
Ultrasonic thickness sensors – Real-time wall thickness feedback with automatic compensation of packing pressure
In-mold temperature and pressure sensors – Closed-loop control for consistent part quality
3.3 Surface Finish Classification – Meeting Every Requirement
Application Requirement Achievable Standard
Transparent Components No bubbles, no flow marks
Plating-Ready Components No gas marks
High-Gloss Components Surface roughness Ra ≤ 0.2μm
Printing/Coating Applications Pre-deformation compensation, registration accuracy ±0.1mm
3.4 Special Materials Capability – Proven Across the Spectrum
Ansix Tech has extensive production experience with a wide range of engineering thermoplastics used in intake manifold applications:
PC/ABS – Automotive interior and underhood components
PC – High-impact applications
PPS + 40% GF – High-temperature, chemical-resistant manifolds
PEEK – Extreme high-temperature applications
PTFE/PFA – Chemical-resistant fluid handling
PA6 + GF30 – Standard automotive manifold material
PBT – Electrical and automotive components
PEI/PPS/LCP – High-performance engineering applications
Liquid Silicone Rubber (LSR) – Sealing and gasket applications
Flame retardancy meets UL94 V-0 standards for housings requiring fire safety certification. Weather resistance is validated through UV testing—3,000 hours with no discoloration.
IV. Full-Process Service – Reducing Customer Management Costs
Many manufacturers overlook service as a differentiator. Ansix Tech treats service as a core competency.
4.1 Early Intervention – DFM Report Before Commitment
Before contract signing, Ansix Tech provides a comprehensive Design for Manufacturability (DFM) report that includes:
Draft angle recommendations
Wall thickness optimization
Gate location analysis
Ejector pin mark location allowances
This upfront analysis ensures that structural issues are identified before mold manufacturing begins—eliminating the costly scenario of discovering unmanufacturable features after tooling is already in progress.
4.2 Trial Molding – Iterative Refinement
Ansix Tech provides T0 through T3 trial samples, each accompanied by a detailed improvement report. Quick-change inserts allow verification of different design solutions without completely rebuilding the mold—saving weeks of lead time and significant cost.
4.3 Small-Batch Validation – Proof Before Full Production
Before full-scale production, Ansix Tech offers 100–500 shot trial runs to statistically validate yield rates and CPK. Production only proceeds to full scale once stability is confirmed.
4.4 Maintenance and Spare Parts – Long-Term Partnership
Spare parts kit (ejector pins, core inserts) delivered with every mold
Preventive maintenance performed every 200,000 cycles
Lifetime repair service at cost price
V. Differential Advantages – Direct Answers to Common Industry Pain Points
Customer Complaint Ansix Tech’s Solution
“Molds need constant repair, disrupting orders” 2,000-shot aging test before delivery with wear report; 3-year structural warranty (excluding normal wear of consumable parts)
“Excessive flash, high secondary processing cost” 0.005mm parting line fit tolerance; self-locking clamp force compensation; flash controlled to ≤0.03mm per batch—eliminating manual deburring
“Dimensions change from batch to batch” Ultrasonic thickness sensors with real-time pressure compensation; in-mold temperature/pressure sensors with closed-loop control
“Mold repair takes too long” In-house electrode machining center and EDM workshop—mold repairs completed without leaving the facility; standard welding/insert replacement restored to production within 24 hours
5.1 The Ansix Tech Philosophy
“For us, a mold is not a block of steel—it is a revenue generator for our clients.”
When Ansix Tech designs a mold, the team simultaneously plans:
Mold rigidity – Ensuring dimensional stability under injection pressure
Venting paths – Preventing air traps and burn marks
Thermal balance – Minimizing cycle time and warpage
The result is a mold that arrives at the customer’s production line ready for immediate use—no debugging, minimal flash, and extended service life.
VI. Material Selection and Processing – Technical Depth
6.1 Material Selection Criteria
For engine intake manifold applications, material selection is driven by:
Operating temperature range – Continuous use temperatures up to 180°C short-term
Chemical resistance – Exposure to fuels, oils, and coolants
Mechanical properties – Tensile strength, impact resistance, creep resistance
Dimensional stability – Low warpage and shrinkage
Flow characteristics – Ability to fill complex runner geometries
6.2 Manufacturing Process Flow
Ansix Tech follows a rigorous, systematic mold manufacturing process:
Part Design Analysis – Understanding the injection-molded part’s function and manufacturing requirements
3D Modeling – Using Siemens NX 3D CAD for full assembly and component drawings
DFM and Moldflow Analysis – Optimizing gate location, cooling, and venting
Steel Selection and Procurement – Material certification and traceability
Rough Machining – High-speed milling of mold bases and rough cavity geometry
Heat Treatment – Achieving target hardness and material properties
Finish Machining – Five-axis high-speed machining, EDM, wire EDM, and grinding
Assembly and Fitting – Precision assembly of all mold components
Inspection – CMM verification, surface finish measurement, hardness testing
Mold Trial – T0 through T3 sampling with improvement reports
Small-Batch Validation – Statistical process capability verification
Delivery – Full documentation including dimensional reports and CPK data
6.3 Cooling System Design – Critical for Cycle Time and Quality
Effective cooling system design is essential for intake manifold molds due to the complex geometry and varying wall thicknesses. Ansix Tech designs cooling systems that:
Minimize cycle time – Rapid, uniform cooling reduces production cost per part
Prevent hot spots – Even cooling eliminates warpage and sink marks
Enable conformal cooling – Cooling channels follow the part contour for maximum efficiency
6.4 Ejection System Design – Reliable Part Release
For intake manifolds with complex undercuts and internal geometry, ejection system design is critical. Ansix Tech incorporates:
Balanced ejection – Preventing part distortion during ejection
Strategic ejector pin placement – Marks located in non-cosmetic areas
Slide and lifter systems – For complex undercuts and internal features
6.5 Runner and Feed System Design
Balanced runner design ensures that all cavities receive melt at identical pressure and temperature profiles. For multi-cavity manifold molds, runner lengths are equalized to ensure uniform filling and consistent part quality across all cavities.
VII. Quality Assurance and Control – The Ansix Tech Standard
7.1 Quality Management System Certification
Ansix Tech has successfully passed ISO9001, ISO14001, IATF16949, and ISO13485 certifications. IATF16949—the automotive industry’s quality management standard—is particularly relevant for intake manifold production, ensuring compliance with the rigorous requirements of Tier 1 automotive suppliers.
7.2 In-Process Quality Control
Raw material inspection – Material certification and verification upon receipt
In-process inspection – Dimensional checks at multiple stages throughout manufacturing
Non-destructive testing – Ultrasonic and magnetic particle testing for defect detection
Final inspection – 100% critical dimension verification
7.3 Validation and Testing
Dimensional inspection – Full CMM reporting for every mold cavity
Surface finish verification – Ra/Rz measurement to 0.01μm precision
Hardness testing – Rockwell/Vickers verification of heat treatment quality
Aging testing – 2,000-shot run-in before delivery
Pressure testing – Leak detection and pressure cycling for intake integrity
CPK validation – Critical dimensions maintained at ≥1.33
7.4 Packaging and Delivery
Each mold is carefully packaged to prevent damage during transit, with full documentation including:
Dimensional inspection reports
Material certification
Heat treatment curves
CPK data
Maintenance and operation manuals
VIII. Cost Optimization – Reducing Hard Costs Through Material, Process, and Efficiency
Ansix Tech’s integrated approach delivers significant hard cost reduction through three primary levers:
8.1 Material Cost Optimization
Gas-assisted injection molding – Reduces plastic usage by creating hollow structures
Hot runner systems – Eliminates runner waste, reducing material consumption
Material substitution expertise – Recommending optimal materials for specific applications without compromising performance
8.2 Process Efficiency Optimization
Cycle time reduction – Optimized cooling system design and process parameters
Lights-out production – Automated systems enable 24/7 production with minimal labor
Zero-defect manufacturing – Eliminates scrap and rework costs
8.3 Efficiency Optimization
70% automated machining – Reduces labor costs and improves consistency
Average mold trial: 2 times – Minimizes development cost and time
One-stop service – Eliminates coordination costs between multiple suppliers
IX. Conclusion: The Ansix Tech Value Proposition
Ansix Tech’s 28+ years of expertise in engine intake manifold mold manufacturing translates into a clear, measurable value proposition for customers:
Customer Need Ansix Tech Solution Measurable Benefit
Reliability 500,000+ shot mold life, CPK ≥1.33 Production continuity, reduced downtime
Precision 0.002mm machining, ±0.1% shot repeatability Consistent part quality, reduced rework
Speed 10–45 day mold delivery, 24-hour repair Faster time-to-market, reduced inventory
Cost Material optimization, process efficiency, one-stop service 15–20% post-processing savings, lower total cost
Risk Reduction DFM before commitment, T0-T3 validation, full documentation No surprises, predictable outcomes
Ansix Tech Limited, with four production bases across China and Vietnam, 260 injection molding machines, over 1,200 employees, and more than 30,000 molds delivered, stands as a global leader in providing end-to-end injection molding solutions. From product design and prototyping to mold manufacturing, high-volume production, secondary processing, and assembly—Ansix Tech seamlessly integrates every stage of the manufacturing lifecycle.
The company’s corporate mission is to “Make Our Customers Successful”—a commitment reflected in every mold designed, every part produced, and every customer relationship built over nearly three decades of manufacturing excellence.
For a comprehensive DFM review of your specific intake manifold project, Ansix Tech invites you to schedule a consultation. The team will walk through a full-process analysis—demonstrating exactly how weld lines, air traps, shrinkage, and other risks are systematically eliminated before a single piece of steel is cut.
Ansix Tech Co Ltd
If you have any plans related to Engine intake manifold mold , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #Engine intake manifold mold #Engine intake manifold mold Material #Engine intake manifold mold Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #Engine intake manifold mold injection molding #Engine intake manifold mold injection tools #Engine intake manifold mold injection moulds #Engine intake manifold mold plastic mould #Engine intake manifold mold plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #Engine intake manifold mold injection molding Customized #Ansix mold factory #Engine intake manifold mold china #Engine intake manifold mold molds #injection factory for Engine intake manifold mold #Engine intake manifold mold injection molding #Engine intake manifold mold injection molding factory #injection molding company #Engine intake manifold mold injection mold companies #Engine intake manifold mold Tooling #Engine intake manifold mold mold limited #Ansix mold china #Ansix companies for Engine intake manifold mold #Ansix company China #Engine intake manifold mold facotry #Ansix Tech #Ansix Tech mould #Engine intake manifold mold injection moulding #Engine intake manifold mold injection moulding company #Ansix Engine intake manifold mold parts injection mold companies #Engine intake manifold mold injection molding companies china #Engine intake manifold mold china factory #Ansix moulding companies #Ansix molding company #Engine intake manifold mold injection moulding facotry #Ansix Tech mold #Engine intake manifold mold mould #Engine intake manifold mold plastic injection molding #ansix plastic mold #Engine intake manifold mold Mold manufacturing #Engine intake manifold mold parts manufacturing #Engine intake manifold mold plastic parts factory #Engine intake manifold mold injection parts mold #Engine intake manifold mold PRECISION MANUFACTURING #Engine intake manifold mold TOOL #China Engine intake manifold mold mold #Engine intake manifold mold Material injection moulding china #Engine intake manifold mold mould china #china precision mold #Engine intake manifold mold Material mold in china #Engine intake manifold mold mold china #Engine intake manifold mold Precision molds #High-precision molds #Engine intake manifold mold High-precision tool #Injection molds #Engine intake manifold moldFactory #Engine intake manifold moldCompany #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #Engine intake manifold moldCompany #Engine intake manifold moldFactory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #Engine intake manifold mold Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #Engine intake manifold mold Large Injection Mold Manufacturer #Engine intake manifold mold Plastic Mold Factory #Injection Mold #Plastic Mold