 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


Engine oil pan mold
FEATURES
The Foundational Blueprint: From Digital Prototype to Verified Design
The journey from concept to physical prototype is a digital-first odyssey at Ansix Tech. Using advanced 3D modeling software, designers create a virtual prototype of the oil pan. This stage is where potential pitfalls are identified and eliminated. A core tenet of their DFM practice is ensuring adequate draft angles—a minimum of 2 degrees is standard, but this increases to 3-5 degrees or more for textured surfaces to guarantee consistent part release.
Equally critical is maintaining uniform wall thickness. Variations lead to differential cooling, which causes warpage, sinks, and internal stresses, compromising the part's structural integrity. Where additional strength is needed, Ansix designers incorporate ribs and gussets rather than thickening walls, preserving material efficiency and cycle time. Every sharp corner is transitioned into a radius, with the outer radius typically 1.5 times the wall thickness, to disperse stress and prevent fracture points.
-
Mold Description
Product Materials:
ABS/PC
Mold Material:
S136ESR
Number of Cavities:
1
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
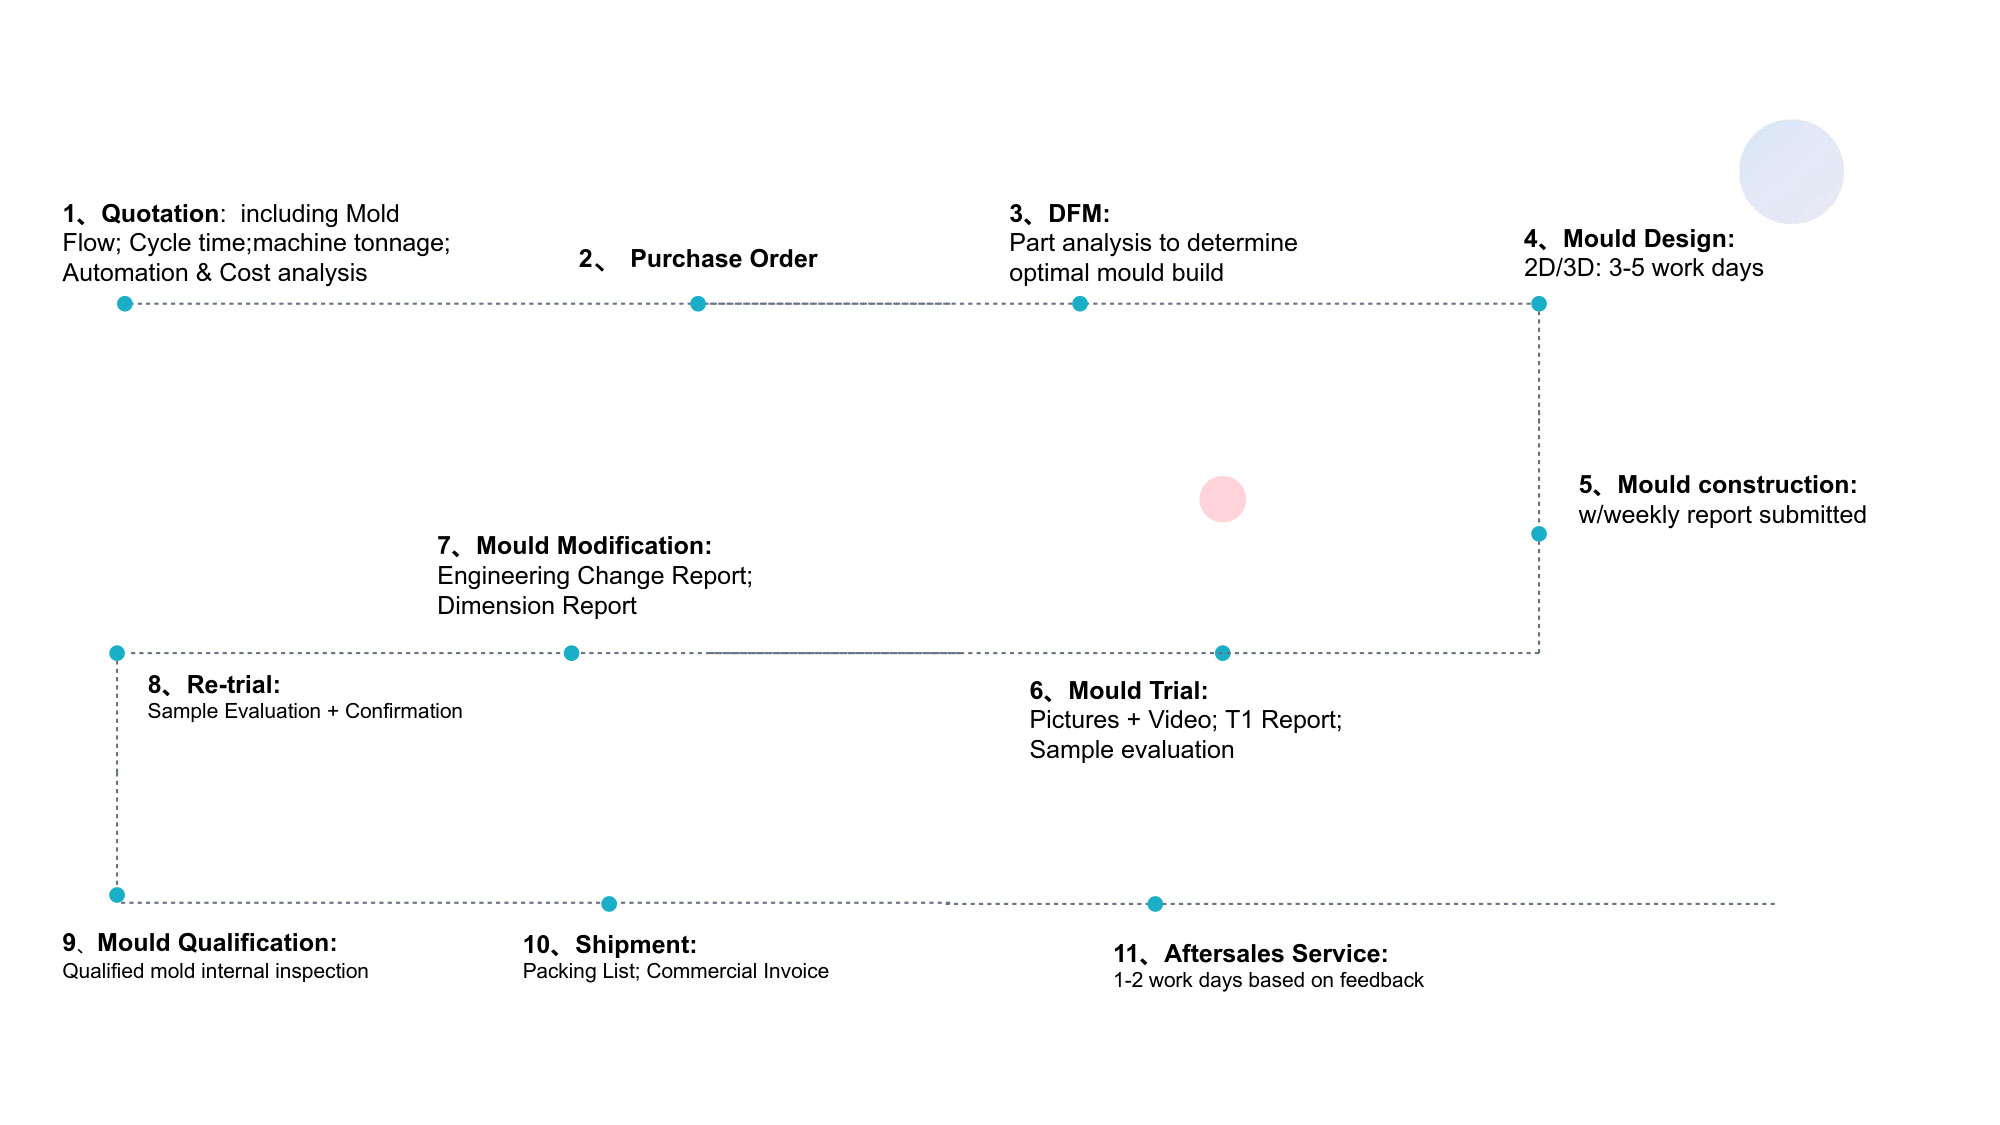
- The mold manufacturing process and product material selection
Key DFM Considerations for Engine Oil Pan Design

This digital model undergoes rigorous prototype design verification. Using techniques analogous to the flexible mold systems noted in contemporary research for diesel oil pans, Ansix rapidly produces functional prototypes for fit, form, and initial function testing. This step validates assembly interfaces, clearances, and basic geometry before committing to expensive mold steel, saving clients weeks of potential rework.
2 The Science of Selection: Materials and Mold Flow Analysis
With a verified design, the focus shifts to two parallel material selections: the plastic for the final oil pan and the steel for the mold itself.
2.1 Selecting the Engineered Plastic
The oil pan material must meet a stringent set of requirements: high heat deflection temperature to resist engine heat, excellent resistance to hydrocarbon oils, good impact strength at varying temperatures, and dimensional stability. Common candidates include filled polypropylene (PP), polyamide (PA, Nylon), and, for more demanding applications, polyphenylene sulfide (PPS).
Ansix Tech employs a sophisticated methodology for material selection and validation. When a client's specified material is not in the standard simulation database, engineers perform a parametric match using six key properties:
Material Abbreviation (e.g., PA66)
Density
Melt Flow Rate (MFR), critical for predicting cavity fill
Shrinkage Rate, to ensure dimensional accuracy
Flexural Modulus, indicating stiffness
Heat Deflection Temperature
By matching these core parameters, Ansix can accurately simulate the behavior of a proposed or alternative material, ensuring performance is not compromised while potentially offering cost savings.
-
Simulating Success with Moldflow Analysis
The selected material model is then fed into a comprehensive Moldflow analysis (DFM). This process, as outlined in industry texts, involves three stages: pre-processing, analysis, and post-processing.
Pre-processing involves importing and meshing the 3D model, then defining the analysis sequence, processing parameters, and building virtual systems for gating, cooling, and ejection. Analysis is the automated computational run. The crucial post-processing phase is where Ansix engineers mine the results for insights. They analyze:
Fill Pattern & Pressure: To ensure balanced filling and identify required injection pressure.
Cooling Time & Efficiency: As cooling consumes 50-70% of the cycle, optimizing it is the single biggest lever for cost reduction.
Warpage Prediction: To foresee and correct dimensional instability.
Location of Weld Lines & Air Traps: To reposition gates or modify features that create weak points or surface defects.
This virtual trial run allows Ansix to perfect the gating system design—often using a strategically placed hot runner system to minimize material waste and cycle time—and to blueprint the cooling circuit before any metal is cut, preventing catastrophic and costly mold rework.
3 Forging the Tool: Precision Manufacturing and Steel Selection
The mold itself is a masterpiece of precision engineering. Its construction begins with the strategic choice of mold steel.
3.1 Mold Steel: The Foundation of Durability
The selection is governed by the part's material, required surface finish, and projected production lifespan. For a high-volume, glass-fiber-filled oil pan mold, Ansix typically selects a premium hardened tool steel like H13 or a corrosion-resistant steel like Stavax (420 stainless). These steels offer an optimal balance of hardness, polishability, and thermal conductivity to withstand abrasive plastics and prolonged thermal cycling.
Thermal conductivity is a key but often overlooked property. As shown in Autodesk's data, a mold's ability to transfer heat away from the plastic part varies dramatically by material. While P20 steel has a conductivity of 29 W/m°C, aluminum conducts heat at 170 W/m°C. Ansix leverages this by using high-conductivity copper alloys or beryllium-copper inserts in critical hot areas of the mold, such as around deep cores or hot runner manifolds, to dramatically speed up heat extraction and reduce cycle time.
3.2 Mastering the Cooling System
The cooling system is the heart of mold efficiency. Ansix designs follow core principles to establish a thermal balance:
Uniform Cooling: Channels are placed at a consistent distance from the cavity surface (typically 10-15mm) to ensure even cooling.
Turbulent Flow: Engineers calculate the required flow rate to achieve a Reynolds number above 4,000, ensuring turbulent flow for maximum heat transfer efficiency.
Strategic Intensification: Additional cooling is always directed at the gate area (the hottest point) and thicker sections of the part.
The firm employs various techniques—baffles, bubblers, and thermal pins—to bring cooling into deep cores and hard-to-reach areas, preventing hot spots that cause long cycles and part warpage.
3.3 The Processing Workflow and Challenges
The manufacturing workflow is a symphony of Computer Numerical Control (CNC) machining, Electrical Discharge Machining (EDM), and precision grinding. Key challenges include:
Machining Deep Cores and Cavities: Maintaining precision and surface finish in deep, slender features.
Achieving Perfect Alignment: Ensuring that the core and cavity halves, along with side actions and lifters, align perfectly over millions of cycles.
Managing Thermal Expansion: Designing components and clearances to account for the heat generated during continuous production.
Ansix overcomes these challenges through a combination of high-precision machinery, in-process inspection, and experienced toolmakers who understand how steel behaves under stress and heat.
4 The Art of Molding: Process Optimization and Quality Assurance
With the completed mold mounted in a high-tonnage injection press, the focus shifts to process optimization.
4.1 Tuning the Process for Efficiency and Cost
The primary goal is to establish a robust, repeatable process window that produces perfect parts in the shortest possible cycle. Ansix technicians meticulously optimize each phase:
Fill Speed & Pressure: Balanced to pack the cavity without causing flash or excessive internal stress.
Packing & Holding: Precisely controlled to compensate for material shrinkage without over-packing.
Cooling Time: The biggest cost driver. By optimizing the cooling system design and ensuring turbulent water flow, Ansix achieves the minimum scientifically determined cooling time.
Energy Consumption: Process parameters are tuned to reduce back pressure and hydraulic pressure where possible, as over 65% of machine energy can come from screw rotation and back pressure friction.
Table 2: Key Levers for Injection Molding Cost Optimization

4.2 Rigorous Quality Control and Assurance
Every production run is governed by a comprehensive Quality Control (QC) plan. First-article inspection involves full coordinate measuring machine (CMM) checks against the CAD model. During production, critical dimensions are monitored using statistical process control (SPC) charts. For an oil pan, functional tests for leak-tightness are often integrated into the production line. This data-driven approach ensures that every part leaving the facility meets the exacting standards required for automotive integration.
4.3 Packaging and Rapid Delivery
Understanding that the mold and its parts are valuable assets, Ansix employs customized, secure packaging. Molds are cleaned, preserved with anti-corrosive coatings, and crated in reinforced wooden boxes with custom foam interiors. Parts are packed to prevent scratching or deformation during transit. The firm’s integrated project management, from design to delivery, ensures rapid turnaround times, a critical factor in today’s fast-paced automotive development cycles.
5 A Legacy of Reliability and Engineered Value
Ansix Tech’s expertise in engine oil pan mold injection molding is built on a foundation of deep industry experience and a commitment to total lifecycle value. Their process is not merely about building a mold; it is about engineering a manufacturing solution that delivers reliability on the factory floor for years.
The company’s true differentiator is its unwavering focus on reducing the total component cost for the customer. This is achieved not by cutting corners, but through intelligent engineering: selecting the optimal material that meets specs without over-engineering, designing a mold that cycles faster and lasts longer, and refining the process to minimize energy and waste. As a result, Ansix Tech delivers more than just a precision component—they deliver a competitive advantage, enabling their clients to bring durable, high-performance automotive systems to market efficiently and reliably. In the demanding world of automotive manufacturing, that engineered value is the ultimate deliverable.
Ansix Tech Co Ltd
If you have any plans related to Engine oil pan mold, you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #Engine oil pan mold#Engine oil pan mold factory #Engine oil pan mold injection mold #Ansix mold factory #Ansix injection molding #Ansix moud Ltd #Engine oil pan moldinjection molding factory #Ansix injection mould #Engine oil pan mold injection molding factory #Engine oil pan mold injection molding company #Engine oil pan mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #injection molding Engine oil pan mold# Ansix mold factory #Engine oil pan mold china #Engine oil pan moldprecision molds #injection factory #Engine oil pan mold precision injection molding #Engine oil pan moldinjection molding factory #injection molding company #Engine oil pan mold injection mold companies #Engine oil pan moldmould factory #Engine oil pan moldmold limited #Ansix mold china #Ansix companies #Ansix company China #Engine oil pan moldfacotry #Ansix Tech #Ansix Tech mould #Engine oil pan mold injection moulding #injection moulding company #Ansix Engine oil pan mold parts injection mold companies #Engine oil pan moldmould #Engine oil pan mold china #Engine oil pan mold china factory #Ansix moulding companies #Ansix molding company #Engine oil pan mold injection moulding facotry #Ansix Tech mold #Engine oil pan moldprecision mould #Engine oil pan moldplastic injection molding #ansix plastic mold #Mold manufacturing #Engine oil pan moldparts manufacturing #Engine oil pan moldplastic parts factory #Engine oil pan moldinjection parts mold #Engine oil pan moldPRECISION MANUFACTURING #Engine oil pan moldmold precision #China mold #Engine oil pan moldinjection moulding china #Engine oil pan moldmould china #china precision mold #mold in china #Engine oil pan moldprecision mold china #Precision molds #High-precision molds #Household appliance molds #Injection molds #Large Injection Molding Factory #Large Injection Molding Company #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #Large Injection Molding Company #Super Large Injection Molding Factory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #Large Injection Mold Manufacturer #Plastic Mold Factory #Injection Mold #Plastic Mold