 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


Engine underbody protection plate mold
FEATURES
Strategic Design and Foundational Analysis
The project commenced with a collaborative design phase focused on the protection plate's functional requirements. The part needed to be impact-resistant to withstand stone strikes, structurally rigid to prevent flexing at high speeds, and chemically resistant to road salts and fluids. Furthermore, weight reduction was paramount for meeting modern fuel efficiency standards.
Ansix Tech engineers employed Design for Manufacturing (DFM) principles from the outset. A critical early step was Mold Flow Analysis (DFM). Using advanced simulation software, the team analyzed how the molten plastic would fill the mold cavity. This virtual prototyping identified potential defects like air traps, weld lines (which can weaken the part), and sink marks long before steel was cut. The analysis allowed for strategic adjustments to part geometry, such as uniform wall thickness, which is crucial for minimizing warpage and achieving consistent cooling.
The gating system—the channel through which plastic enters the mold—was meticulously designed. A multi-point hot runner system was selected. This system keeps the plastic in the runners molten, eliminating solid waste (cold runner scrap) and allowing for balanced filling of the large, complex part geometry. This choice directly contributes to material savings and faster cycle times, laying the first foundation for cost control.
-
Mold Description
Product Materials:
PP+EPDM LT
Mold Material:
S136ESR
Number of Cavities:
1
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
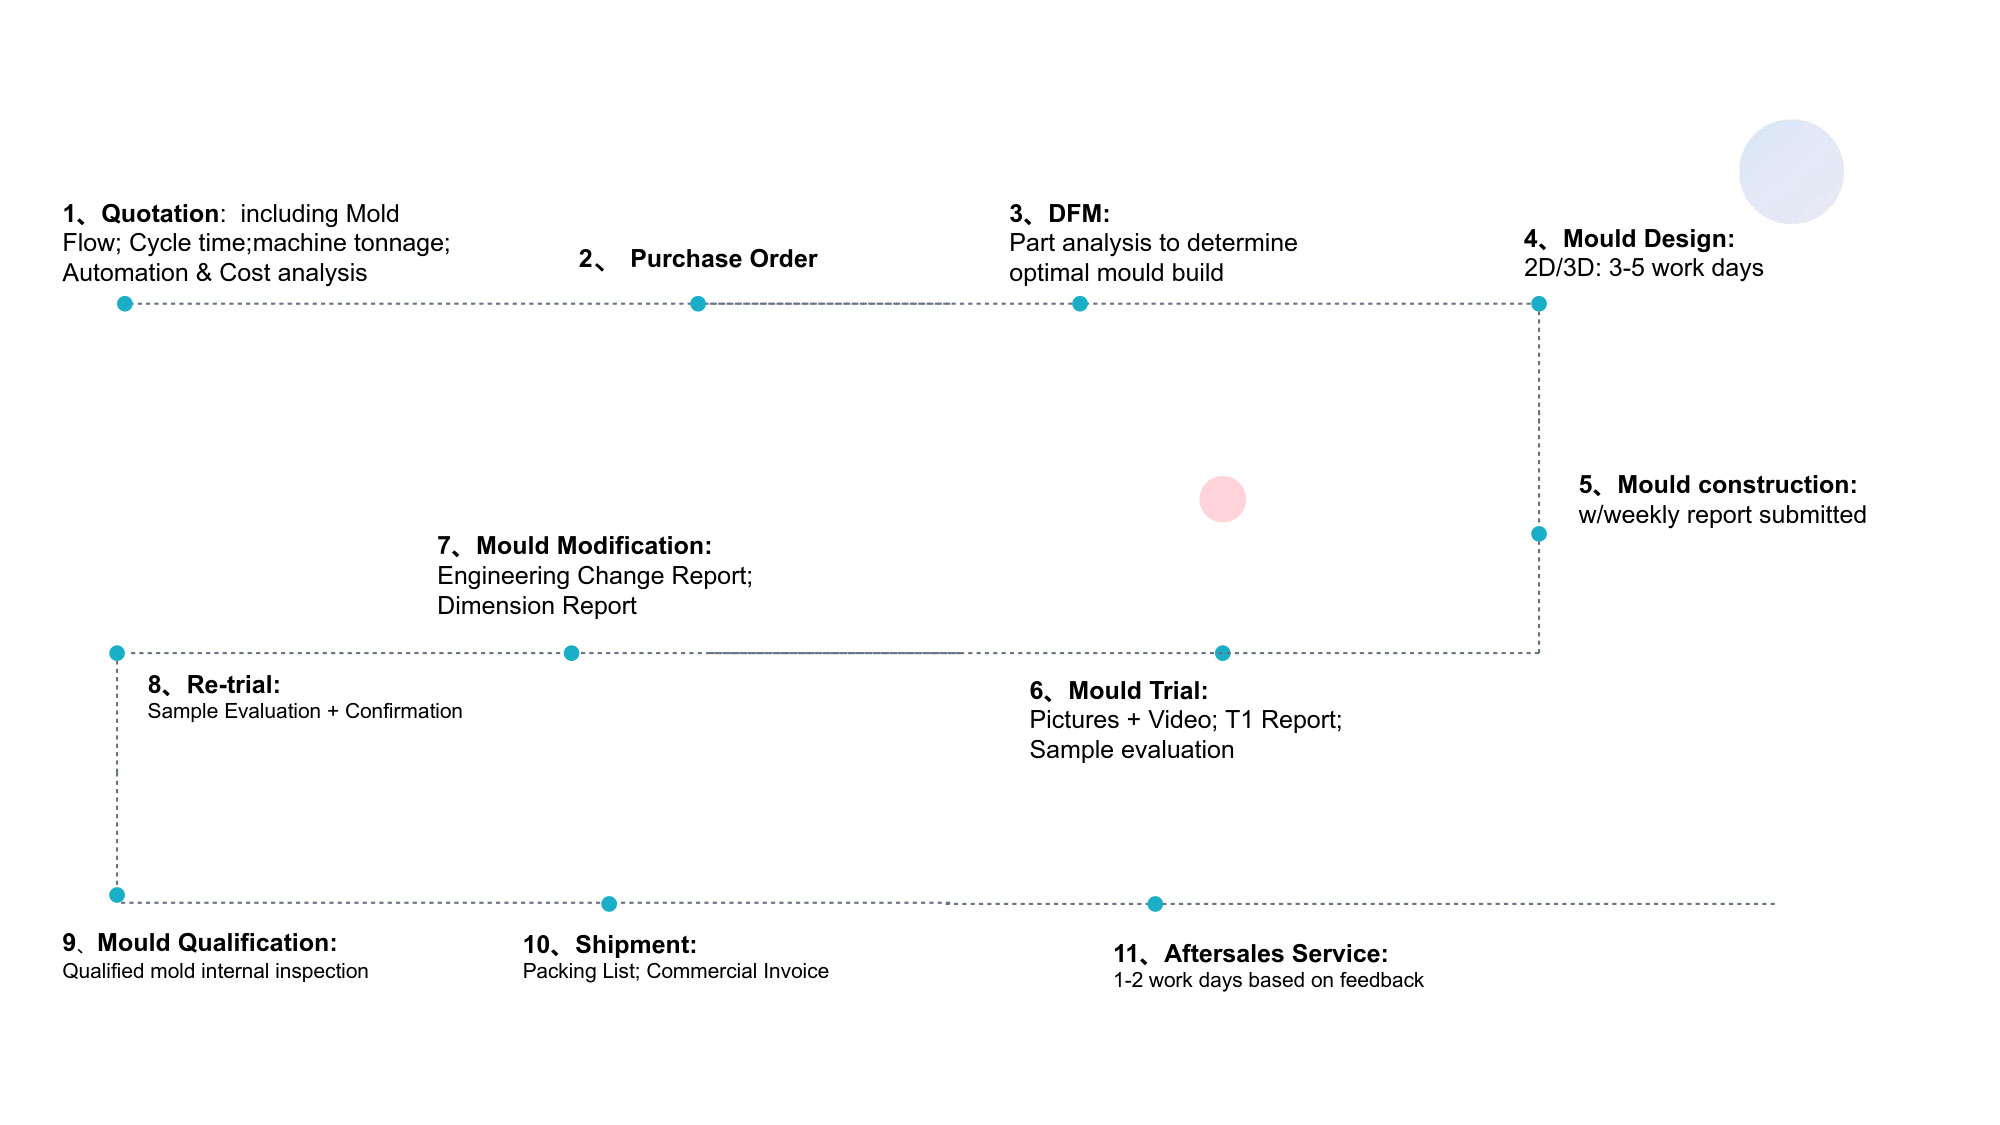
- The mold manufacturing process and product material selection
The Science of Material Selection
Choosing the right material is a cornerstone of performance and cost management. For this protection plate, Ansix Tech evaluated several engineering thermoplastics, guiding the client toward the most cost-effective choice that met all specifications.
The selected long-fiber reinforced polypropylene composite offers a compelling value proposition. The continuous fibers, typically glass, are fed directly into a compounding unit and impregnated with the polymer, resulting in a material with exceptional toughness and durability—properties essential for an underbody component. By advocating for this material, Ansix Tech provided the client with a component that was lighter than metal alternatives, corrosion-proof, and produced at a fraction of the raw material cost of more exotic plastics.
Phase 3: Precision Mold Engineering and Manufacturing
With the design and material finalized, the focus shifted to building the high-precision mold—the heart of the production process.
-
Precision Mold Engineering and Manufacturing
With the design and material finalized, the focus shifted to building the high-precision mold—the heart of the production process.
1. Advanced Mold Design: The protection plate's large size and complex curvature necessitated an innovative core and cavity design. Instead of a monolithic, difficult-to-machine block, the team designed the mold with modular, interchangeable镶块 (inserts) and滑块 (sliders). This "building block" approach offers multiple advantages: it simplifies machining, allows for replacement of only worn sections (dramatically reducing maintenance costs), and facilitates future design changes for different vehicle models.
2. Strategic Steel Selection: Mold steel was chosen based on the abrasive nature of the glass-filled material and the need for long production life. A pre-hardened tool steel with high polishability and excellent wear resistance was selected for the primary cavities. For high-wear areas like gates and intricate features, hardened tool steel inserts were used. This combination ensures longevity and maintains part quality over hundreds of thousands of cycles, controlling long-term cost-per-part.
3. Optimized Cooling System: A mold is fundamentally a heat exchange device. Efficient cooling is the single biggest factor in determining cycle time and part quality. Ansix Tech designed a conformal cooling system. Unlike traditional straight-drilled channels, conformal channels follow the 3D contour of the part cavity at a near-constant distance. This is achieved through advanced manufacturing techniques like 3D printing or specialized machining. This design ensures uniform and rapid heat extraction, which minimizes cycle time by up to 30% and prevents warpage caused by uneven cooling. The design adhered to strict principles: avoiding weld lines, prioritizing cooling near the gate, and maintaining safe distances from ejector pins and other mold components.
4. Robust Ejection System: Ejecting a large, flat part without distortion requires careful planning. A system of high-count, strategically placed ejector pins and sleeve ejectors was designed to apply even, controlled force across the part's surface. This prevents "push pins" or sticking, which can halt production and damage the mold.
Phase 4: Process Optimization for Peak Efficiency
The manufacturing challenge involved molding a large, structurally demanding part consistently and quickly. Ansix Tech's process engineers implemented several key optimizations.
Intelligent Process Control: Moving beyond traditional trial-and-error setup, the team utilized Decoupled Molding® principles and cavity pressure sensors. This scientific approach separates the filling, packing, and cooling phases of the cycle. Pressure sensors inside the cavity provide real-time data, allowing the machine to automatically adjust parameters to compensate for natural variations in material viscosity. This ensures every shot is identical, dramatically reducing scrap rates and guaranteeing quality.
Cycle Time Minimization: Every second saved in the cycle translates to thousands of dollars saved over a production run. Efforts focused on the cooling phase, which typically consumes over 80% of the cycle. The conformal cooling system was the primary contributor. Furthermore, the team optimized the packing pressure profile and time to the minimum necessary to prevent sink marks, and fine-tuned the mold opening, ejection, and closing sequences for speed without risk of damage.
Phase 5: Rigorous Quality Assurance and Rapid Delivery
Quality is engineered into every step. During sampling, parts underwent comprehensive validation: Coordinate Measuring Machine (CMM) scans verified dimensional accuracy against the CAD model; impact tests confirmed mechanical performance; and fit-checks ensured perfect assembly on the vehicle chassis.
For mass production, the integrated process control system acts as a continuous quality gate. If a shot falls outside the preset pressure or time parameters, the system can flag or even reject the part automatically. This "quality-at-the-source" philosophy prevents defective parts from progressing downstream, saving immense costs associated with rework, recalls, or warranty claims.
Finally, understanding the critical path of automotive launches, Ansix Tech executed a streamlined packaging and delivery protocol. The mold was disassembled, professionally crated with custom fixtures to prevent transit damage, and shipped via expedited logistics, ensuring it arrived at the client's press room on schedule and ready for immediate production.
Conclusion: Delivering Measurable Value Beyond the Mold
Ansix Tech's engine underbody protection plate mold project exemplifies modern, value-driven manufacturing. The client's cost savings were achieved not through corner-cutting, but through intelligent engineering at every stage:
Material Choice: Selecting LFRT PP provided performance at an optimal raw material cost.
Mold Design: The modular design reduces future maintenance and modification expenses.
Process Innovation: Conformal cooling and scientific molding slashed cycle time and scrap rates, directly lowering the cost per part.
Quality Integration: In-process monitoring virtually eliminates the high costs of post-production failure.
For automotive manufacturers facing relentless pressure to innovate while controlling costs, partnering with a mold maker like Ansix Tech, which views itself as a manufacturing process partner, is a strategic advantage. The deliverable is more than a precision tool; it is a guarantee of reliability, efficiency, and total cost ownership that drives the client's competitive edge in the global marketplace.
Ansix Tech Co Ltd
If you have any plans related to Engine underbody protection plate mold, you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #Brake light mold factory #Engine underbody protection plate mold #Ansix mold factory #Ansix injection molding #Ansix moud Ltd #Engine oil pan moldinjection molding factory #Ansix injection mould #Center console storage compartment ing factory #Engine oil pan mold injection molding company #Engine oil pan mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #injection molding Engine oil pan mold# Ansix mold factory #Engine oil pan mold china #Engine oil pan moldprecision molds #injection factory #Engine oil pan mold precision injection molding #Engine oil pan moldinjection molding factory #injection molding company #Engine oil pan mold injection mold companies #Engine oil pan moldmould factory #Engine oil pan moldmold limited #Ansix mold china #Ansix companies #Ansix company China #Engine oil pan moldfacotry #Ansix Tech #Ansix Tech mould #Engine oil pan mold injection moulding #injection moulding company #Ansix Engine oil pan mold parts injection mold companies #Engine oil pan moldmould #Engine oil pan mold china #Engine oil pan mold china factory #Ansix moulding companies #Ansix molding company #Engine oil pan mold injection moulding facotry #Ansix Tech mold #Engine oil pan moldprecision mould #Engine oil pan moldplastic injection molding #ansix plastic mold #Mold manufacturing #Engine oil pan moldparts manufacturing #Engine oil pan moldplastic parts factory #Engine oil pan moldinjection parts mold #Engine oil pan moldPRECISION MANUFACTURING #Engine oil pan moldmold precision #China mold #Engine oil pan moldinjection moulding china #Engine oil pan moldmould china #china precision mold #mold in china #Engine oil pan moldprecision mold china #Precision molds #High-precision molds #Household appliance molds #Injection molds #Large Injection Molding Factory #Large Injection Molding Company #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #Large Injection Molding Company #Super Large Injection Molding Factory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #Large Injection Mold Manufacturer #Plastic Mold Factory #Injection Mold #Plastic Mold
