 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


Injection molding of automotive light guide strip mold
FEATURES
Hard Power Infrastructure – Building Trust Through Measurable Capabilities
At Ansix Tech, transparency about manufacturing resources forms the foundation of client confidence. Optical light guide strips demand mirror-polished parting lines, flawless surface finishes, and sub-micron dimensional fidelity.
Precision Mold Processing Equipment
5-Axis High-Speed Machining Centers deliver 0.002mm geometric accuracy on complex freeform surfaces, ensuring that mating lines on transparent components remain seamless and burr-free. This capability eliminates secondary manual polishing costs and prevents light leakage defects that arise from visible parting line misalignment.
Slow Wire EDM enables the fabrication of 0.03mm micro-slots and narrow ribs without heat-affected zone distortion or burr formation. For thin-wall light guide features that resist conventional machining, wire EDM preserves wall integrity while achieving positional tolerances that sustain optical uniformity.
CNC EDM & Precision Electrode Grinding Centers provide the fine finishing required for micro-optical surface patterns. With in-house electrode manufacturing, Ansix eliminates external vendor dependency and accelerates mold repair cycles.
-
Mold Description
Product Materials:
PMMA CM205
Mold Material:
S136ESR
Number of Cavities:
2
Glue Feeding Method:
COLD runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
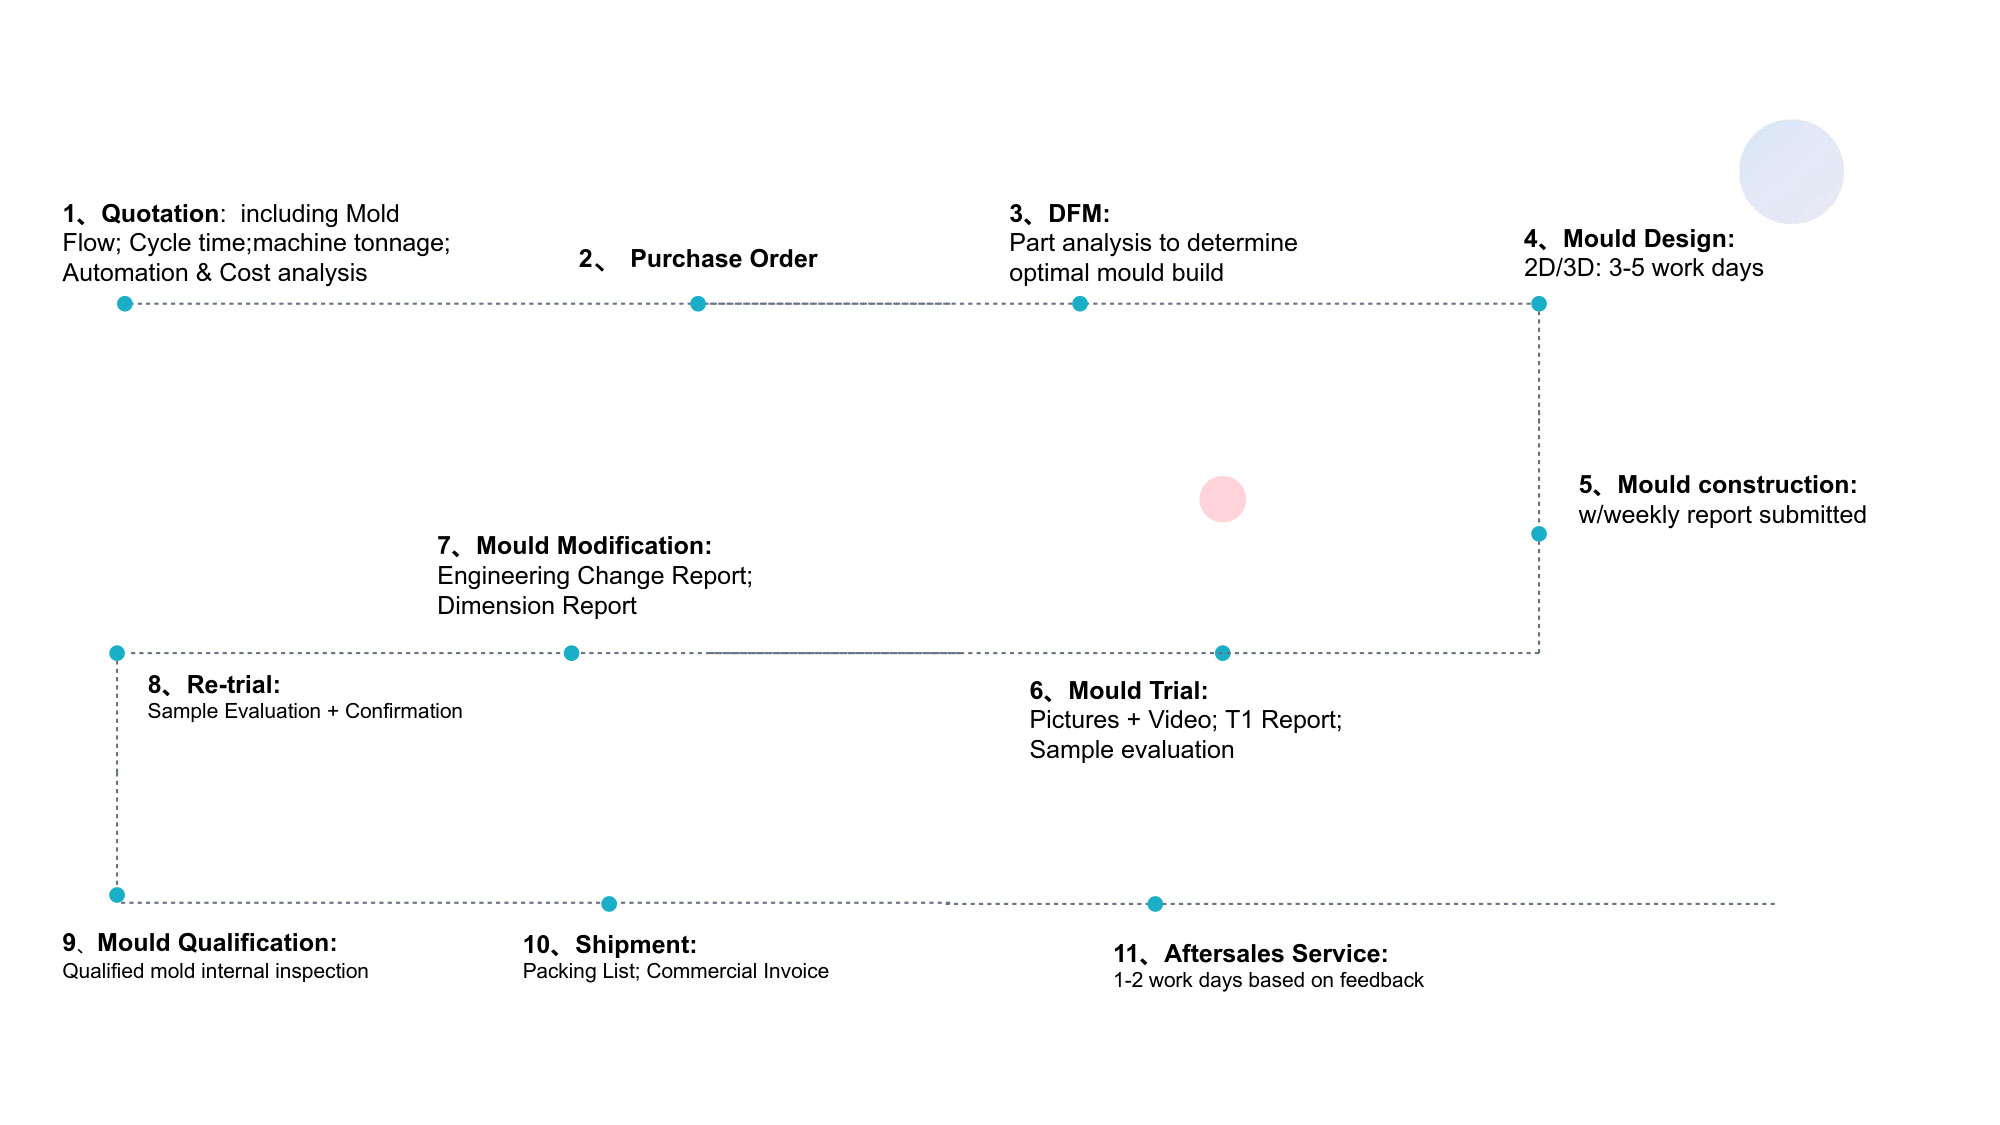
- The mold manufacturing process and product material selection
Injection Molding Machine Fleet
Light guide strips range from compact interior ambient lighting bars (150mm) to complex front grille signature strips exceeding 1200mm in length. The machine fleet spans 30 tons to 400+ tons, configured with:
All-Servo Electric Drive Systems delivering ±0.1% shot-to-shot repeatability. For light guide production, where melt temperature uniformity directly impacts clarity and stress birefringence, servo-electric precision ensures every mold cycle replicates the same optical performance standard.
Liquid Temperature Control (LTC) Zone Management with integrated mold temperature controllers achieving cavity-to-cavity thermal balance within ±1°C. For thick-wall PC light guides (5mm–15mm typical wall thickness), ±2°C temperature stability across core and cavity faces prevents differential shrinkage zones that cause rainbow banding and optical distortion.
Real-Time Process Monitoring with closed-loop feedback that automatically adjusts injection speed and pressure decay profiles based on cavity sensor inputs. For OEMs requiring PPAP documentation, machine logs provide full parameter traceability.
Quality Assurance & Metrology
Every Ansix Tech mold undergoes full dimensional validation before leaving the facility:
CMM (Coordinate Measuring Machine) inspection delivers complete geometric reports with feature-by-feature comparison against CAD baseline
Optical 3D Scanners enable non-contact full-surface evaluation for freeform optics, particularly valuable for light guide components with draft angles and varying cross-section profiles
Critical Dimension Capability (CPK ≥ 1.33) is guaranteed on all customer-identified key characteristics, including sealing interfaces, mounting boss positions, and optical lens surface profiles
-
Mold Manufacturing – Core Competitiveness Delivered Through Specific Metrics
Mold Life Expectancy
Based on material selection, Ansix provides clear lifecycle commitments:
Mold Component Material Grades Life Expectancy
Mold Base P20 Structural integrity throughout mold life
Core/Cavity (Standard) S136, 2344, 2343, 8407, SKD11/61, DC53 1 million cycles (standard plastics)
Core/Cavity (Reinforced) M340, 4Cr13, 9Cr18, NAK80, H13 500,000 cycles (glass fiber-reinforced materials)
Material certifications and heat treatment curves are provided with every mold delivery. Steel grades such as 1.2083 and 1.2709 are specified for optical-grade applications requiring high polishability and corrosion resistance.
Achievable Tolerances
Component Type Standard Tolerance Precision Capability
General structural components ±0.05mm Industry standard
Precision gears / medical components ±0.005mm Ultra-precision class
Mold Types
Ansix manufactures a comprehensive range of mold configurations:
Hot Runner Systems – Reduce material waste and improve cycle efficiency
Stack Molds – Double production output without increasing machine footprint
Two-Shot / Multi-Material Molds – Enable overmolding and complex material combinations
High-Gloss / Mirror-Finish Molds – Surface roughness Ra < 0.05μm, essential for transparent optical components
Gate System Optimization
Through advanced mold flow analysis, Ansix predicts weld line and gas trap locations before steel is cut. Gate positions and quantities are optimized to ensure fill balance, preventing flow marks, short shots, and optical defects. For light guides, the gate design must accommodate low-speed injection to avoid birefringence and internal stress.
Standard Lead Times
Mold Complexity Standard Lead Time Expedited Option
Simple molds 10 days —
Medium complexity 25–45 days 20 days (with validation protocols maintained)
High-complexity optical molds Negotiated per project Available upon request
Section Three: Injection Molding Process Control – Reducing Quality Anxiety
Clients' primary concerns are shrinkage, flash, dimensional instability, and batch-to-batch color variation.
Process Standardization
All machines are networked with成型 parameters (temperature, pressure, speed, time) locked into the MES (Manufacturing Execution System) . Only authorized engineers can adjust settings. First-article and last-article inspections are conducted for every batch, ensuring process stability throughout production runs.
Dimensional Stability Control
Molds are equipped with zone-specific mold temperature controllers, maintaining core-to-cavity temperature differentials within 2°C to minimize warpage. For a typical bracket component, three consecutive production batches over one week show critical hole spacing variation ≤ 0.02mm.
Surface Finish Quality Grades
Requirement Achievable Standard
Transparent components No bubbles, no flow marks
Platable components No gas marks
High-gloss components Surface roughness Ra ≤ 0.2μm
Components requiring painting/printing Reserved deformation compensation; print registration accuracy ±0.1mm
Specialty Material Capabilities
Ansix has extensive production experience with a wide range of engineering thermoplastics:
Material Family Specific Grades
PC/ABS blends Automotive interior grades
Polycarbonate (PC) Optical grade, thick-wall light guides
PPS + 40% GF High-temperature, high-strength applications
PEEK Ultra-high-performance engineering
PTFE / PFA Chemical-resistant, high-temperature
PA6 + GF30 Reinforced nylon
PBT Electrical and automotive components
PEI / PPS / LCP High-heat, precision applications
Liquid Silicone Rubber (LSR) Soft-touch and sealing applications
PMMA Primary optical light guide material
Flame retardancy meets UL94 V-0 standards for housing applications. Weather resistance is validated through 3,000-hour UV testing with no color change or degradation.
Section Four: Full-Service Lifecycle Support – Reducing Client Management Costs
Early-Stage Intervention (DFM Reports)
Before contract signing, Ansix provides comprehensive Design for Manufacturability (DFM) reports containing:
Draft angle recommendations
Wall thickness optimization
Gate location analysis
Ejector pin mark location allowances
Weld line and gas trap risk assessment
This ensures structural issues are identified before mold construction begins, preventing costly redesigns.
Trial Molding & Sampling
Ansix provides T0 through T3 trial samples, each accompanied by improvement reports. Interchangeable inserts enable rapid validation of different design variations without rebuilding the entire mold.
Pilot Production Validation
Before full-scale production, 100–500 shot pilot runs are conducted to establish yield rates and CPK statistics. Mass production commences only after process stability is confirmed.
Maintenance & Spare Parts
Spare wear parts (ejector pins, core inserts) are delivered with every mold
Preventive maintenance is performed every 200,000 cycles
Lifetime repair services are provided at cost-based pricing
2000-shot aging tests are conducted before delivery, with wear reports provided
Section Five: Differentiated Competitive Advantages – Addressing Common Industry Pain Points
Common Client Complaint Ansix's Solution
Frequent mold repairs disrupting orders 2000-shot aging test before delivery with wear report; 3-year structural warranty (excluding normal wear parts)
Excessive flash increasing post-processing costs 0.005mm parting line fit precision; self-locking clamp force compensation; flash controlled within 0.03mm per batch
Inconsistent dimensions batch-to-batch Ultrasonic wall-thickness sensors providing real-time feedback; automatic holding pressure compensation; in-cavity temperature and pressure sensors for closed-loop control
Long mold repair lead times In-house electrode machining and EDM workshops; most repairs completed without leaving the facility; standard weld repair/insert replacement within 24 hours
Material Science & Processing Technology
Raw Material Selection
For automotive light guide strips, material selection directly impacts optical performance, dimensional stability, and long-term durability. Ansix's material engineering team evaluates multiple parameters:
PMMA (Polymethyl Methacrylate) – The primary material for light guide applications due to its exceptional optical clarity (92% light transmission), weatherability, and dimensional stability. PMMA is specified for most interior and exterior lighting applications where optical efficiency is paramount.
PC (Polycarbonate) – Selected for applications requiring higher impact resistance and thermal stability. Thick-wall PC light guides (5mm–15mm) demand precise process control to prevent sink marks and internal stresses.
Material Certification – Every material batch is accompanied by full certification documentation, including melt flow index (MFI), tensile strength, flexural modulus, notched Izod impact strength, heat deflection temperature (HDT), and UV stability data.
Mold Flow Analysis (MFA)
Mold flow analysis is conducted for every light guide mold project. The analysis covers:
Fill pattern optimization – Ensuring balanced cavity filling without flow hesitation
Weld line prediction – Identifying and mitigating visible weld lines that compromise optical uniformity
Gas trap identification – Preventing burn marks and incomplete filling
Pressure drop analysis – Optimizing gate locations to minimize injection pressure requirements
Cooling simulation – Designing conformal cooling channels for uniform temperature distribution
Shrinkage and warpage prediction – Compensating for material-specific shrinkage behavior
Mold Design Priorities
For light guide strip molds, design focuses on:
Parting Line Design – Minimizing visible witness lines on optical surfaces. Mirror-polished parting lines ensure seamless light transmission without scattering.
Ejection System Design – Strategic placement of ejector pins in non-optical areas, with ejector pin marks controlled to acceptable tolerances.
Cooling System / Water Lines – Conformal cooling channels designed to maintain uniform temperature distribution. Temperature differentials across the cavity are maintained within ±2°C.
Runner & Gate System – Hot runner systems minimize material waste and provide precise melt delivery. Gate vestige is controlled to eliminate secondary trimming operations.
Venting System – Adequate venting prevents gas entrapment that causes burn marks and incomplete fill.
Manufacturing Process Flow
The complete mold manufacturing workflow includes:
Design & Engineering – CAD modeling, DFM analysis, mold flow simulation
Material Procurement – Certified steel grades with full traceability
Rough Machining – 5-axis high-speed machining of core and cavity
Heat Treatment – Precise hardening with documented heat treatment curves
Precision Machining – Finish machining, wire EDM for fine features
EDM & Electrode Machining – For complex geometries and micro-optical patterns
Fitting & Assembly – Precision fitting of all mold components
Polishing – Mirror-finish polishing for optical surfaces (Ra < 0.05μm)
Trial Molding – T0 through T3 trials with improvement documentation
Validation – Full dimensional inspection, CPK analysis, wear testing
Injection Molding Process Optimization
Efficiency Improvement – Cycle times are optimized through:
Advanced cooling system design reducing cooling time by up to 30%
Hot runner systems eliminating runner waste and reducing cycle time
Servo-electric drives providing faster response and energy savings
Automated part handling and conveyor systems
Cost Control – Production costs are minimized through:
Material waste reduction via hot runner and optimized gate design
Energy-efficient servo-electric machines reducing power consumption by 40–70%
Automated quality inspection reducing manual inspection costs
Preventive maintenance programs minimizing unplanned downtime
Quality Control & Assurance
In-Process Quality Control
First Article Inspection (FAI) – Comprehensive dimensional verification of first production shots
In-Process Monitoring – Real-time parameter monitoring with automated alarms for deviations
SPC (Statistical Process Control) – Continuous monitoring of critical dimensions
Last Article Inspection – Verification that process stability is maintained through the entire run
Final Quality Assurance
100% Dimensional Inspection – Critical dimensions verified on every batch
Optical Performance Testing – Light transmission, uniformity, and color consistency verification
Environmental Testing – Thermal cycling, humidity, and UV exposure testing as required
Packaging Validation – Protective packaging designed to prevent damage during transit
PPAP Documentation
For automotive OEM requirements, Ansix provides full PPAP (Production Part Approval Process) documentation including:
Design records
Engineering change documents
Process flow diagrams
FMEA (Failure Mode and Effects Analysis)
Control plans
Measurement system analysis
Dimensional results
Material test results
Capability studies (CPK ≥ 1.33)
Delivery & Logistics
Packaging
Custom-designed packaging to prevent surface damage and contamination
Anti-static packaging for electronic-sensitive components
Traceable labeling with batch and date coding
Export-worthy crating for international shipments
Rapid Delivery
Standard delivery – Based on project scope and complexity
Expedited options – Available for urgent requirements (validation protocols maintained)
Real-time tracking – Shipment tracking provided for all deliveries
Door-to-door logistics – International shipping coordinated through established logistics partners
Industry Experience & Reliability
With over 28 years of specialized experience, Ansix has developed deep expertise across:
Automotive Interior Lighting – Ambient lighting, dashboard illumination, footwell lighting
Exterior Lighting – DRL (Daytime Running Light) pipes, front grille signature lighting, rear combination lamps
Display Lighting – Instrument cluster backlighting, infotainment display illumination
Client Value Proposition
What problems does Ansix solve?
Client Concern Ansix Solution Value Delivered
Design uncertainty Comprehensive DFM reports before mold construction Prevents costly redesigns; reduces time-to-market by 3–6 weeks
Quality inconsistency CPK ≥ 1.33 on all critical dimensions; closed-loop process control Eliminates scrap and rework; reduces quality-related costs by up to 40%
Production bottlenecks 30–400+ ton machine fleet; stack mold capabilities Scales production capacity without capital investment
Supply chain complexity End-to-end service from design to delivery Single-source accountability; reduces vendor management costs
Hidden costs Transparent pricing with no surprise charges; lifetime repair support Predictable total cost of ownership
Cost Reduction Strategy
Ansix reduces client costs through multiple levers:
Material Cost Reduction – Optimized gate design and hot runner systems reduce material waste by 15–25%. Material selection guidance ensures optimal cost-to-performance ratio.
Process Efficiency – Cycle time optimization reduces per-part manufacturing cost by 20–35%. Servo-electric machines reduce energy consumption by 40–70%.
Quality Cost Reduction – Zero-defect capability eliminates inspection, rework, and scrap costs. CPK ≥ 1.33 ensures process capability that meets Six Sigma standards.
Tooling Cost Optimization – Extended mold life (500,000–1,000,000 cycles) amortizes tooling cost over larger production volumes. Standardized mold bases and interchangeable inserts reduce maintenance costs.
Conclusion: The Ansix Difference
For Ansix Tech, a mold is not merely a block of steel—it is a revenue-generating asset. Every mold is designed with comprehensive consideration of:
Process robustness – Ensuring trouble-free operation on the client's production line
Venting pathways – Preventing gas-related defects
Thermal balance – Eliminating warpage and dimensional variation
Ejection optimization – Minimizing cycle time and preventing part damage
The result is a mold that arrives at the client's facility ready for production—with minimal setup, minimal flash, and maximum lifespan.
Call to Action
Ansix Tech invites prospective clients to experience the difference firsthand. A full-process DFM report walkthrough can be arranged using an existing product as a case study, demonstrating how weld lines, gas traps, and shrinkage risks are identified and resolved before mold construction begins.
For more information about Ansix Tech's automotive light guide strip mold manufacturing capabilities, or to schedule a DFM consultation, please contact our engineering team.
Ansix Tech – Over 28 Years of Precision Injection Molding Excellence
Ansix Tech Co Ltd
If you have any plans related to Injection molding of automotive light guide strip mold , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #Injection molding of automotive light guide strip mold #Injection molding of automotive light guide strip mold Material #Injection molding of automotive light guide strip mold Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #Injection molding of automotive light guide strip mold injection molding #Injection molding of automotive light guide strip mold injection tools #Injection molding of automotive light guide strip mold injection moulds #Injection molding of automotive light guide strip mold plastic mould #Injection molding of automotive light guide strip mold plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #Injection molding of automotive light guide strip mold injection molding Customized #Ansix mold factory #Injection molding of automotive light guide strip mold china #Injection molding of automotive light guide strip mold molds #injection factory for Injection molding of automotive light guide strip mold #Injection molding of automotive light guide strip mold injection molding #Injection molding of automotive light guide strip mold injection molding factory #injection molding company #Injection molding of automotive light guide strip mold injection mold companies #Injection molding of automotive light guide strip mold Tooling #Injection molding of automotive light guide strip mold mold limited #Ansix mold china #Ansix companies for Injection molding of automotive light guide strip mold #Ansix company China #Injection molding of automotive light guide strip mold facotry #Ansix Tech #Ansix Tech mould #Injection molding of automotive light guide strip mold injection moulding #Injection molding of automotive light guide strip mold injection moulding company #Ansix Injection molding of automotive light guide strip mold parts injection mold companies #Injection molding of automotive light guide strip mold injection molding companies china #Injection molding of automotive light guide strip mold china factory #Ansix moulding companies #Ansix molding company #Injection molding of automotive light guide strip mold injection moulding facotry #Ansix Tech mold #Injection molding of automotive light guide strip mold mould #Injection molding of automotive light guide strip mold plastic injection molding #ansix plastic mold #Injection molding of automotive light guide strip mold Mold manufacturing #Injection molding of automotive light guide strip mold parts manufacturing #Injection molding of automotive light guide strip mold plastic parts factory #Injection molding of automotive light guide strip mold injection parts mold #Injection molding of automotive light guide strip mold PRECISION MANUFACTURING #Injection molding of automotive light guide strip mold TOOL #China Injection molding of automotive light guide strip mold mold #Injection molding of automotive light guide strip mold Material injection moulding china #Injection molding of automotive light guide strip mold mould china #china precision mold #Injection molding of automotive light guide strip mold Material mold in china #Injection molding of automotive light guide strip mold mold china #Injection molding of automotive light guide strip mold Precision molds #High-precision molds #Injection molding of automotive light guide strip mold High-precision tool #Injection molds #Injection molding of automotive light guide strip moldFactory #Injection molding of automotive light guide strip moldCompany #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #Injection molding of automotive light guide strip moldCompany #Injection molding of automotive light guide strip moldFactory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #Injection molding of automotive light guide strip mold Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #Injection molding of automotive light guide strip mold Large Injection Mold Manufacturer #Injection molding of automotive light guide strip mold Plastic Mold Factory #Injection Mold #Plastic Mold

- PMMA CM205 TDS