 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing

PEEK industrial valve seals
FEATURES
Hard Power Infrastructure: The Foundation of Manufacturing Excellence
1.1 Mold Manufacturing Equipment
Ansix Tech's manufacturing capabilities are built upon a foundation of precision equipment that directly translates into customer value. The company operates state-of-the-art 5-axis high-speed machining centers capable of machining complex curved surfaces with 0.002mm precision, ensuring that product parting lines are smooth and free from burrs—a critical requirement for valve sealing surfaces where even microscopic imperfections can compromise sealing integrity. Additionally, slow wire EDM (Electrical Discharge Machining) equipment enables the creation of fine micro-holes as small as 0.03mm and narrow slots while preventing thin-wall deformation, essential for complex valve seal geometries.
Customer Value: These capabilities eliminate secondary deburring operations, reduce post-processing costs, and ensure that sealing surfaces meet the most demanding surface finish requirements directly out of the mold.
-
Mold Description
Product Materials:
PEEK
Mold Material:
CNC MACHINING
Number of Cavities:
1
Glue Feeding Method:
COLD runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
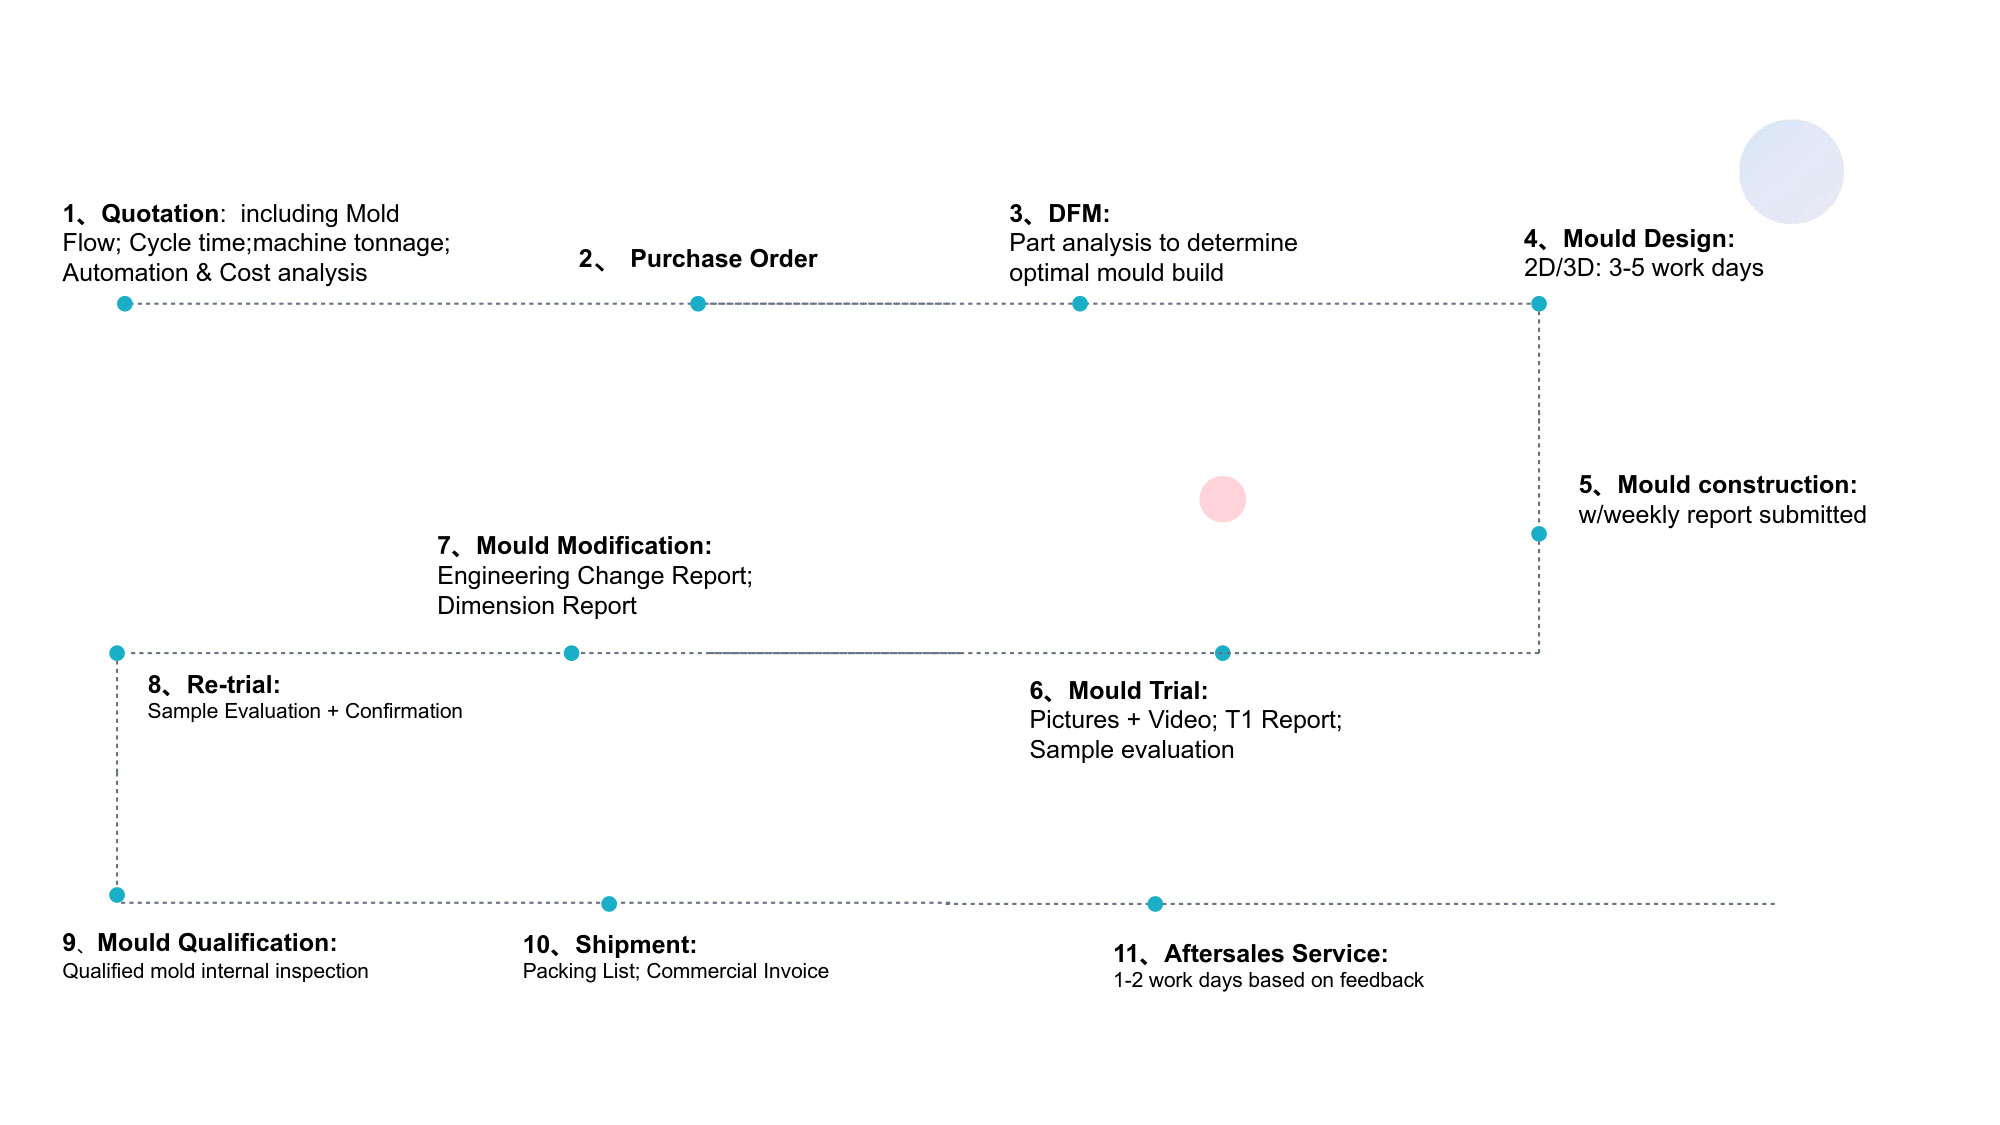

- The mold manufacturing process and product material selection
Inspection and Quality Assurance Equipment
Every mold shipped from Ansix Tech undergoes full dimensional reporting using Coordinate Measuring Machines (CMM) and optical imaging inspection systems. Key dimensional CPK (Process Capability Index) values are maintained at ≥1.33 for critical dimensions, demonstrating six-sigma-level process control. This rigorous inspection protocol ensures that every mold meets specifications before leaving the factory.
Customer Value: CPK ≥1.33 means the process produces virtually no out-of-spec parts—fewer rejects, less scrap, and lower total cost of ownership for the customer.
-
Mold Manufacturing Core Competitiveness: Delivering Measurable Results
2.1 Mold Steel Selection and Hardness
For PEEK injection molding, mold steel selection is critical due to the material's high processing temperatures and abrasive nature. PEEK and glass-fiber-reinforced PEEK present significant challenges in terms of wear, thermal expansion, sealing, venting, and dimensional stability. Ansix Tech selects mold steels based on application requirements:
Mold Component Recommended Steel Grades Rationale
Mold Base P20 Cost-effective, good machinability
Cavity/Core (Standard) H13, 2344, 8407, SKD61 High hot hardness, thermal fatigue resistance
Cavity/Core (Corrosive environments) S136, M340, 4Cr13, 9Cr18, STAVAX Corrosion resistance, excellent polishability
Cavity/Core (High wear) DC53, SKD11 Superior wear resistance for glass-filled grades
High-gloss/Transparent parts NAK80 Excellent polishability, Ra<0.05μm
For general PEEK molding applications, H13 or S136 high-hardness stainless steel with deep tempering is recommended—not just for wear resistance, but to ensure dimensional stability under long-term high-temperature cycling. For corrosive environments or medical/food-contact applications, S136 corrosion-resistant stainless steel is prioritized. All mold steels undergo full热处理 with hardness reaching HRC55 or above to ensure cavity wear resistance. Complete material certification reports and heat treatment curves are provided to customers.
Customer Value: Proper steel selection directly translates to mold life—50万 shots for glass-filled PEEK grades and 100万 shots for unfilled grades. This means fewer mold replacements, lower amortized tooling costs, and uninterrupted production schedules.
2.2 Achievable Tolerances
Ansix Tech delivers precision at multiple tolerance tiers:
Standard structural components: ±0.05mm
Precision gears and medical components: ±0.005mm
Customer Value: Customers receive parts that fit the first time, every time. No rework, no assembly issues, no field failures due to dimensional non-conformance.
2.3 Mold Types and Capabilities
Ansix Tech manufactures a comprehensive range of mold types to meet diverse production requirements:
Hot runner systems: Reduce material waste and cycle time
Stack molds: Double production efficiency
Two-shot/multi-material molds: Enable complex multi-material valve seal designs
High-gloss molds: Surface roughness Ra<0.05μm for transparent or cosmetic applications
2.4 Gate and Runner System Design
PEEK melt has high viscosity, requiring careful runner and gate design. Ansix Tech employs full-round runners to minimize pressure loss. For gate design, side gates or large-size point gates are preferred, with gate thickness reaching at least 50%-80% of the part's thickest section to prevent premature freezing during the packing stage. Through comprehensive Moldflow analysis, the company pre-identifies weld line and gas trap locations, optimizing gate quantity and positions to ensure balanced filling.
Customer Value: Optimized gate design eliminates short shots, weld lines, and voids—common failure points in valve seals that lead to leakage and field failures.
2.5 Mold Delivery Standards
Mold Complexity Standard Lead Time Expedited Lead Time
Simple molds 10 days N/A
Medium complexity 25-45 days 20 days (with accelerated validation)
High complexity 45-60 days 35 days
Customer Value: Predictable delivery timelines enable customers to plan production schedules with confidence, reducing inventory carrying costs and time-to-market.
III. Injection Molding Process Control: Eliminating Quality Anxiety
3.1 Process Standardization and Parameter Lockdown
All injection molding machines are networked and connected to a MES (Manufacturing Execution System). Critical process parameters—temperature, pressure, speed, and time—are locked within the system and can only be adjusted by authorized engineers. Every batch undergoes first-article and last-article inspection and comparison.
Customer Value: Parameter lockdown means consistent parts across batches, shifts, and production runs. Customers never receive a "bad batch" due to operator error.
3.2 Dimensional Stability Control
PEEK is sensitive to cooling rates, and its mechanical properties depend heavily on its degree of crystallinity. PEEK crystallizes evenly only when the mold temperature is uniform. Ansix Tech employs mold temperature controller zoning to maintain core and cavity temperature differences within 2°C, minimizing warpage and deformation. For a typical bracket product, three consecutive batches produced over one week showed key hole spacing fluctuation ≤0.02mm.
Customer Value: Dimensional stability means seals fit valve bodies consistently, eliminating assembly rejects and field leakage.
3.3 Core PEEK Injection Molding Parameters
PEEK injection molding is considered the "ultimate challenge" in molding due to its ultra-high melting point (approx. 343°C) and rapid crystallization characteristics. Ansix Tech maintains precise control over the following critical parameters:
Parameter Recommended Range Impact on Quality
Material drying 150-160°C, 3-4 hours, moisture <0.02% Prevents hydrolysis, bubbles, brittleness
Melt temperature 370-400°C Too low→poor melting; too high→gas degradation
Mold temperature 160-200°C (typically 175-190°C) Controls crystallinity; low temp→warpage
Injection pressure 80-120 MPa packing pressure Compensates for crystallization shrinkage
Injection speed Medium to high Prevents premature cooling
Cooling time Extended (longer than conventional thermoplastics) Ensures complete crystallization
The company uses oil temperature controllers or cartridge heaters to achieve and maintain these high mold temperatures.
3.4 Appearance Quality Standards
Ansix Tech achieves multiple appearance quality tiers:
Transparent parts: No bubbles, no flow marks
Plated parts: No gas marks
High-gloss parts: Surface roughness Ra≤0.2μm
Printed/coated parts: Pre-compensation for deformation, print registration accuracy ±0.1mm
3.5 Specialty Material Capabilities
Ansix Tech has extensive production experience with a wide range of high-performance engineering thermoplastics, including:
PC/ABS, PC
PPS+40%GF
PEEK (various grades: unfilled, 30% glass-filled, carbon-filled)
PTFE/PFA
PA6+GF30, PBT
PEI, PPS, LCP
Liquid Silicone Rubber (LSR)
For PEEK, the company works with multiple grades including Victrex® PEEK 450GL15 (15% glass fiber, excellent strength and dimensional stability) and other high-performance PEEK compounds qualified for use up to 288°C and 0.16 GPa.
Customer Value: Single-source capability for multiple material types reduces supplier qualification costs and simplifies supply chain management.
IV. Full-Process Service: Reducing Customer Management Costs
4.1 Early Intervention: DFM (Design for Manufacturability) Reports
Before contract signing, Ansix Tech provides comprehensive mold feasibility analysis reports including:
Draft angle recommendations
Wall thickness optimization
Gate location recommendations
Ejector pin mark location allowances
Identification of potential molding issues before tooling begins
Customer Value: Customers avoid the costly "discover-after-tooling" scenario where structural issues require expensive mold modifications.
4.2 Trial Molding and Sampling
Ansix Tech provides T0 through T3 trial samples, each accompanied by improvement reports. The company can quickly exchange inserts to validate different approaches without rebuilding the entire mold.
Customer Value: Rapid iteration reduces development time and costs. Customers see tangible progress at every stage.
4.3 Small-Batch Validation
Prior to full production, Ansix Tech provides 100-500 shot pilot runs with yield statistics and CPK calculations. Production only proceeds to mass manufacturing after stability is confirmed.
Customer Value: Zero-risk production ramp-up. Customers never commit to mass production until quality is proven.
4.4 Maintenance and Spare Parts
Each mold ships with spare wear parts (ejector pins, core inserts). Ansix Tech provides mold maintenance every 200,000 shots and offers lifetime repair service at cost.
Customer Value: Predictable maintenance costs, no production interruptions due to unexpected mold failures.
V. Differentiated Competitive Advantages: Addressing Common Industry Pain Points
5.1 Mold Wear and Production Interruptions
Industry Pain Point: Molds requiring frequent repair disrupt production schedules.
Ansix Tech Solution: Every mold undergoes 2,000-shot aging tests before delivery, with wear reports provided. The company offers a three-year structural warranty on all molds (excluding normal consumable wear).
Customer Value: Customers can plan production with confidence, knowing the mold will perform reliably for millions of cycles.
5.2 Flash (Burrs) and Secondary Finishing Costs
Industry Pain Point: Excessive flash requires expensive manual deburring operations.
Ansix Tech Solution: Parting lines are machined to 0.005mm fit precision. Self-locking clamp force compensation ensures flash is controlled within 0.03mm per batch, eliminating manual deburring.
Customer Value: Elimination of secondary finishing operations reduces per-part cost by 15-30% and accelerates production throughput.
5.3 Dimensional Inconsistency Across Batches
Industry Pain Point: Parts from different batches don't fit assemblies consistently.
Ansix Tech Solution: Ultrasonic wall thickness sensors provide real-time feedback on wall thickness fluctuations and automatically compensate packing pressure. In-mold temperature and pressure sensors enable closed-loop control.
Customer Value: Consistent parts = zero assembly rework = lower total cost.
5.4 Extended Mold Repair Lead Times
Industry Pain Point: Mold repairs require sending molds to external shops, causing weeks of downtime.
Ansix Tech Solution: In-house electrode manufacturing and EDM workshops enable most mold repairs without leaving the facility. Standard welding/insert replacement is completed within 24 hours.
Customer Value: Minimal production downtime = higher overall equipment effectiveness (OEE).
VI. Cost Reduction Strategy: Delivering Value Through Optimization
6.1 Material Cost Optimization
PEEK is an expensive material, and any scrap represents significant cost. Ansix Tech employs multiple strategies to minimize material waste:
Hot runner systems: Reduce material waste rate to 3.2%
Direct gating: Eliminates runner systems, reducing material waste and per-part cost
Multi-cavity tooling: Four-cavity molds cost approximately 1.8× a single-cavity mold but increase production efficiency by 3×+, significantly reducing per-unit energy and labor costs
6.2 Process Efficiency Optimization
All-servo electric machines: Reduce energy consumption by up to 30% compared to hydraulic machines
Automated manufacturing cells: Integrate in-line quality inspection, part separation, and robotic handling
MES-connected parameter control: Eliminates scrap from operator errors
6.3 Product Cost Reduction Through Metal Replacement
PEEK injection molding offers clear advantages over conventional metal-machining methods in terms of productivity and cost efficiency. Compared to machined metal valve seals:
Material utilization increases from ~20% (machining) to >95% (injection molding)
Production cycle time reduces to 1/5 that of CNC machining
Per-unit cost reduction of 30-40% for high-volume production
VII. Quality Assurance and Verification
7.1 Material Traceability
Every PEEK industrial valve seal produced by Ansix Tech is fully traceable from raw material receipt to finished product shipment. Material certificates, batch numbers, and processing parameters are recorded and archived.
7.2 In-Process Quality Control
Stage Control Method Acceptance Criteria
Raw material receipt Material certification review Material grade verification
Pre-drying Moisture content measurement <0.02%
First article Full dimensional inspection All dimensions within spec
In-process Random sampling, SPC monitoring CPK ≥1.33
Final inspection 100% critical dimension check Zero defects on sealing surfaces
Outgoing Full dimensional report Complete documentation package
7.3 Post-Molding Processing
For critical applications, Ansix Tech offers annealing—a controlled heat treatment that removes internal stresses and stabilizes crystallinity. Typical annealing procedure involves heating parts slowly to 200-230°C, holding for 2-4 hours, and cooling very slowly to room temperature.
Customer Value: Annealed parts are dimensionally stable—no "post-mold warpage" days or weeks later.
VIII. Industry Certifications and Standards
Ansix Tech maintains multiple quality certifications demonstrating its commitment to excellence:
ISO 9001:2015 (Quality Management)
ISO 13485 (Medical Devices)
IATF 16949 (Automotive)
HACCP (Food Safety)
For PEEK industrial valve seals serving the oil and gas industry, materials are selected to meet NORSOK M-710 and M-630 qualifications where required, confirming suitability for harsh offshore and subsea operating environments.
IX. Customer Value Summary
Customer Concern Ansix Tech Solution Measurable Benefit
Mold breaks down too often 50-100万 shot mold life, 3-year structural warranty Predictable production, lower TCO
Parts don't fit consistently ±0.005mm precision, CPK≥1.33 Zero assembly rework
Too much flash/scrap 0.03mm flash control, hot runner waste <3.2% 15-30% lower per-part cost
Long mold repair times 24-hour in-house repair Minimal production downtime
Parts fail in the field Full DFM, process validation, annealing Extended product service life
Too many suppliers to manage 260 machines, 28 years experience, multiple materials Single-source solution
Conclusion
PEEK industrial valve seals represent one of the most demanding injection molding applications in modern manufacturing. The material's exceptional properties—high-temperature resistance up to 250°C, chemical resistance against aggressive media, and mechanical strength that rivals metals—come with equally demanding processing requirements. Success requires mastery of high-temperature mold design, precise process control, rigorous quality systems, and deep material science understanding.
Ansix Tech, with over 28 years of manufacturing experience and 260 injection molding machines across four production bases in China and Vietnam, has developed comprehensive capabilities across the entire PEEK industrial valve seal value chain. From material selection and DFM analysis through mold design, manufacturing, process validation, mass production, and after-sales support, the company delivers measurable customer value at every stage.
As the company's philosophy states: a mold is not just a piece of steel—it is a money-printing machine. Every mold is designed with comprehensive consideration of flow balance, venting paths, thermal equilibrium, and ease of manufacturing to ensure that when it reaches the customer's production line, it delivers trouble-free operation, minimal flash, and extended service life.
For customers seeking a trusted partner in PEEK industrial valve seal manufacturing, Ansix Tech offers the hard infrastructure, technical expertise, process control, and full-service support to turn demanding specifications into reliable, cost-effective production solutions.
Ansix Tech Co Ltd
If you have any plans related to PEEK industrial valve seals , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #PEEK industrial valve seals #PEEK industrial valve seals Material #PEEK industrial valve seals Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #PEEK industrial valve seals injection molding #PEEK industrial valve seals injection tools #PEEK industrial valve seals injection moulds #PEEK industrial valve seals plastic mould #PEEK industrial valve seals plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #PEEK industrial valve seals injection molding Customized #Ansix mold factory #PEEK industrial valve seals china #PEEK industrial valve seals molds #injection factory for PEEK industrial valve seals #PEEK industrial valve seals injection molding #PEEK industrial valve seals injection molding factory #injection molding company #PEEK industrial valve seals injection mold companies #PEEK industrial valve seals Tooling #PEEK industrial valve seals mold limited #Ansix mold china #Ansix companies for PEEK industrial valve seals #Ansix company China #PEEK industrial valve seals facotry #Ansix Tech #Ansix Tech mould #PEEK industrial valve seals injection moulding #PEEK industrial valve seals injection moulding company #Ansix PEEK industrial valve seals parts injection mold companies #PEEK industrial valve seals injection molding companies china #PEEK industrial valve seals china factory #Ansix moulding companies #Ansix molding company #PEEK industrial valve seals injection moulding facotry #Ansix Tech mold #PEEK industrial valve seals mould #PEEK industrial valve seals plastic injection molding #ansix plastic mold #PEEK industrial valve seals Mold manufacturing #PEEK industrial valve seals parts manufacturing #PEEK industrial valve seals plastic parts factory #PEEK industrial valve seals injection parts mold #PEEK industrial valve seals PRECISION MANUFACTURING #PEEK industrial valve seals TOOL #China PEEK industrial valve seals mold #PEEK industrial valve seals Material injection moulding china #PEEK industrial valve seals mould china #china precision mold #PEEK industrial valve seals Material mold in china #PEEK industrial valve seals mold china #PEEK industrial valve seals Precision molds #High-precision molds #PEEK industrial valve seals High-precision tool #Injection molds #PEEK industrial valve seals Factory #PEEK industrial valve seals Company #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #PEEK industrial valve seals Company #PEEK industrial valve seals Factory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #PEEK industrial valve seals Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #PEEK industrial valve seals Large Injection Mold Manufacturer #PEEK industrial valve seals Plastic Mold Factory #Injection Mold #Plastic Mold