 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing

PEEK machining of aviation connector housings
FEATURES
Core Hard Capabilities – Building Customer Trust Through Infrastructure
1.1 Mold Processing Equipment
Ansix's mold manufacturing facility is equipped with state-of-the-art machinery that forms the foundation of precision manufacturing:
Five-Axis High-Speed Machining Centers: These advanced systems enable the machining of complex curved surfaces with precision up to 0.002mm. This capability ensures that parting lines on connector housings remain smooth and burr-free—a critical requirement for aviation connectors where surface integrity directly affects sealing performance and electrical insulation. For aerospace connector housings requiring ultra-high precision (±0.005–0.01mm) and fine surface finishes (Ra ≤0.8μm), 5-axis CNC milling is essential.
Slow-Wire EDM (Electrical Discharge Machining): This technology enables the creation of 0.03mm fine micro-holes and narrow slots without causing thin-wall deformation. Aviation connector housings often feature complex internal geometries with multiple pin positions and thin walls; slow-wire EDM ensures these features are machined with exceptional accuracy while maintaining structural integrity.
In-House Electrode Machining Center and EDM Workshop: Ansix maintains a fully self-contained electrode production and EDM capability. This means mold repairs and modifications can be completed without leaving the facility—conventional welding and insert replacement can be restored to production within 24 hours, dramatically reducing downtime.
-
Mold Description
Product Materials:
PEEK
Mold Material:
S136ESR
Number of Cavities:
1
Glue Feeding Method:
COLDrunner
Cooling Method:
Water cooling
Molding Cycle
42.5s
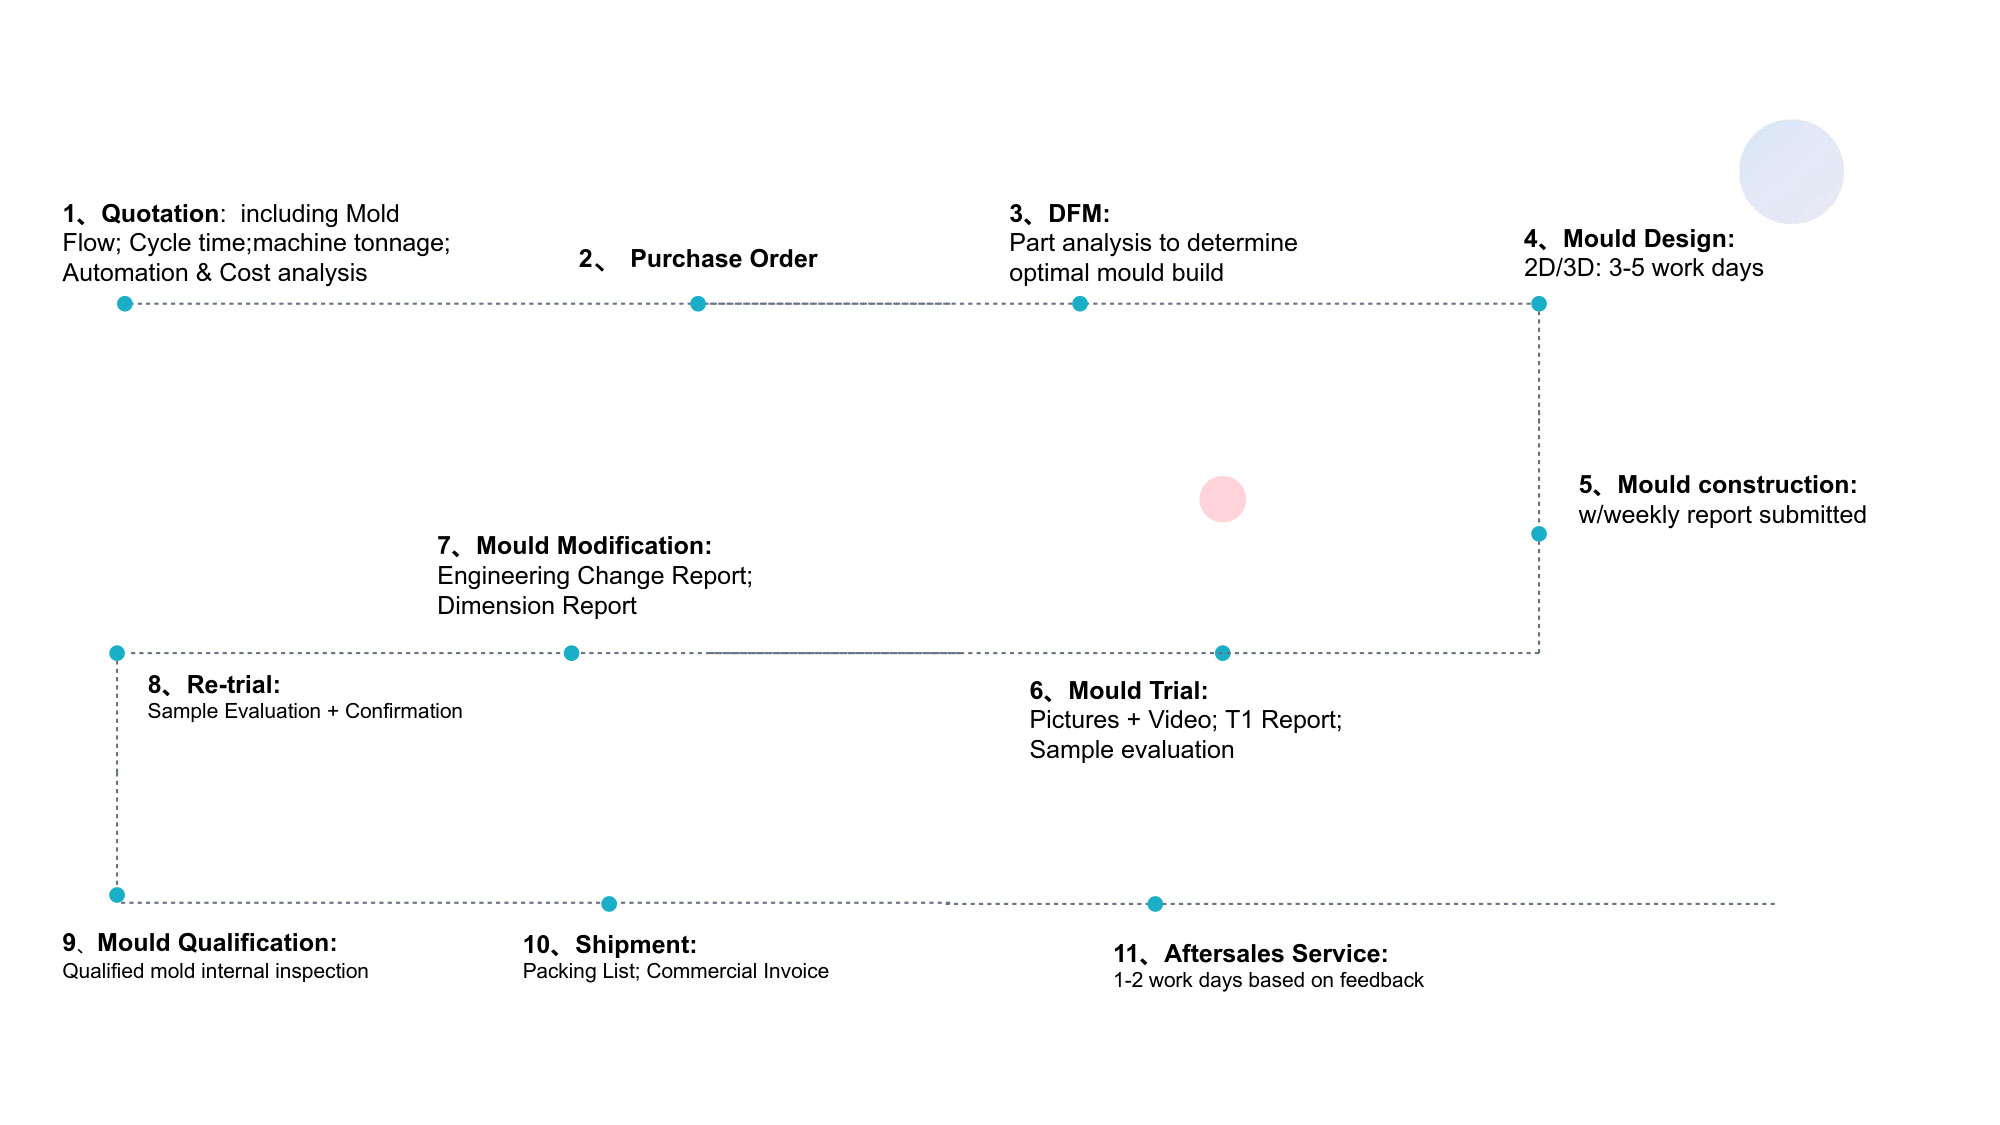

- The mold manufacturing process and product material selection
Injection Molding Machine Fleet
Ansix operates a comprehensive range of all-servo electric injection molding machines with clamping forces ranging from 30 tons to 4,000 tons. This extensive range covers everything from miniature connector components to large, complex housing assemblies.
All-Servo Electric Drive Systems: These machines deliver stable repeatability accuracy of ±0.1% , ensuring that every shot is consistent across high-volume production runs. For PEEK materials, which require precise thermal management, servo-electric drives provide the controlled velocity and pressure profiles necessary to achieve optimal filling and crystallization.
Key Technical Specifications:
Temperature Control: Precision barrel heating systems capable of maintaining PEEK melt temperatures above 350°C
Injection Pressure: Capable of holding 7–14 MPa during the packing phase
Closed-Loop Control: Real-time feedback systems that automatically adjust injection parameters to maintain dimensional stability
-
Inspection and Metrology Equipment
Coordinate Measuring Machines (CMM): Every mold undergoes a comprehensive full-dimension report comparison before leaving the factory. Critical dimensions are verified against design specifications with CPK ≥ 1.33—a statistical measure indicating that the process is highly capable and stable.
Optical Inspection Systems: High-resolution optical measurement systems verify surface quality, feature placement, and dimensional accuracy for both molds and production parts.
Ultrasonic Wall Thickness Sensors: Installed on injection molding machines, these sensors provide real-time feedback on wall thickness fluctuations and automatically compensate packing pressure to maintain consistency.
Section II: Mold Manufacturing – Core Competitive Advantages
2.1 Mold Life and Material Selection
Ansix's mold construction follows a rigorous material selection protocol based on the specific application requirements:
Mold Component Material Options Application Context
Mold Base P20 Standard applications, cost-effective
Core/Cavity Inserts S136, 2344, 2343, 8407, SKD11/61, DC53, M340, 4Cr13, 9Cr18, NAK80, H13 High-wear applications, glass-filled materials
Performance Guarantees:
Glass-fiber reinforced materials: Minimum 500,000 mold cycles
Unfilled or standard plastics: Minimum 1,000,000 mold cycles
Transparency and Documentation: Ansix provides material certification reports and heat treatment curves for all mold steels, giving customers full visibility into the quality and traceability of the materials used in their tooling.
2.2 Achievable Tolerances
Part Category Achievable Tolerance
Standard structural components ±0.05mm
Precision gears and medical/aerospace components ±0.005mm
For aviation connector housings, where pin alignment and housing dimensions directly affect electrical performance and mating reliability, these tolerances ensure consistent, high-quality connections.
2.3 Mold Types and Configurations
Ansix offers a comprehensive portfolio of mold technologies:
Hot Runner Systems: Reduce material waste by eliminating the cold runner, improving material utilization and cycle efficiency. For PEEK materials—which are expensive—hot runner systems deliver significant material cost savings.
Stack Molds: Double production efficiency by molding two layers of parts simultaneously, effectively doubling output without increasing machine footprint.
Two-Shot/Multi-Material Molds: Enable the production of components with multiple materials or colors in a single molding cycle, reducing secondary operations and assembly costs.
High-Gloss Molds: Achieve surface roughness Ra < 0.05μm, ideal for transparent or aesthetic-critical components.
2.4 Gate and Runner System Design
PEEK injection molding requires specialized gate design considerations. PEEK gates must be larger than those used for standard thermoplastics—typically designed at 2/3 of the maximum wall thickness of the product, with a minimum diameter of 6mm, to ensure adequate mold filling capability.
Mold Flow Analysis (MFA): Ansix employs advanced Moldflow simulation to:
Predict weld line and air trap locations
Optimize gate quantity and placement
Ensure balanced filling across the cavity
Minimize stress concentrations and improve overall part quality
Case Example: For a 3mm-thick aerospace connector mold, gate thickness can be precisely adjusted from 1.5mm to 1.8mm to eliminate sink marks, with residual traces ≤0.3mm.
2.5 Cooling System Design
PEEK's high processing temperature (melt >350°C) and crystalline nature demand sophisticated thermal management:
Multi-Zone Temperature Control: Ansix employs mold temperature controllers with zoned heating, maintaining temperature differences between core and cavity within 2°C to minimize warpage and distortion.
Conformal Cooling: Advanced cooling channel designs that follow the contour of the part geometry ensure uniform heat extraction, reducing cycle times and improving dimensional stability.
Hydraulic Mold Temperature Control: Capable of reaching 200°C to meet the demanding thermal requirements of PEEK processing.
2.6 Ejection System Design
Proper ejection system design is critical for PEEK parts, which can be prone to sticking due to their high crystallinity and shrinkage characteristics. Ansix's ejection systems are designed with:
Optimized ejector pin placement to minimize visible witness marks
Sufficient ejection force to overcome part adhesion without damage
Wear-resistant ejector components for long-term reliability
Section III: Injection Molding – Process Control Excellence
3.1 Material Pretreatment and Handling
PEEK is a hygroscopic material that requires careful drying before processing:
Drying Parameters:
Temperature: 150–200°C
Duration: 6–8 hours for virgin material
Moisture Target: Below 0.02% to prevent hydrolysis and surface defects
For reinforced PEEK composites, Ansix ensures uniform mixing of glass fibers or other additives through twin-screw extrusion processes to guarantee consistent material performance.
3.2 Process Standardization and Control
MES-Integrated Process Locking: All molding machines are networked and integrated with a Manufacturing Execution System (MES). All process parameters—including temperature, pressure, speed, and timing—are locked within the system and can only be modified by authorized engineers.
First-Article and Last-Article Inspection: Every production batch undergoes first-piece and last-piece comparison to verify process stability throughout the run.
Statistical Process Control (SPC): Continuous monitoring of critical-to-quality parameters ensures that any deviation is detected and corrected before non-conforming parts are produced.
3.3 Dimensional Stability Control
Real-Time Wall Thickness Monitoring: Ultrasonic sensors mounted on the mold provide continuous feedback on wall thickness. The system automatically compensates packing pressure to maintain dimensional consistency.
Temperature Differential Control: By maintaining the temperature difference between core and cavity within 2°C, Ansix minimizes warpage and distortion—common failure modes for PEEK components.
Performance Data: For similar bracket-type products, Ansix has demonstrated that critical hole spacing fluctuations remain within ±0.02mm across three production batches over a one-week period.
3.4 Surface Quality and Appearance Standards
Application Surface Quality Standard
Transparent components No bubbles, no flow marks
Plated/coated components No gas marks
High-gloss components Surface roughness Ra ≤ 0.2μm
For components requiring painting or printing, Ansix incorporates compensation for deformation into the design, achieving print registration accuracy within ±0.1mm.
3.5 Special Material Capabilities
Ansix has extensive experience molding a wide range of high-performance engineering thermoplastics:
PC/ABS – Automotive and consumer electronics
PC – Transparent and structural applications
PPS + 40% GF – High-temperature, chemical-resistant applications
PEEK – Aerospace, medical, and high-performance industrial
PTFE/PFA – Chemical-resistant and high-purity applications
PA6 + GF30 – Structural and automotive components
PBT – Electrical and electronic applications
PEI/PPS/LCP – High-temperature electronic applications
Liquid Silicone Rubber (LSR) – Sealing and gasket applications
Material Certifications: Ansix can provide:
UL94 V-0 flame rating certification for housings and bobbins
UV testing documentation (3,000 hours without discoloration)
Radiation resistance data—PEEK and PPS provide superior radiation resistance while maintaining low outgassing properties, making them ideal for satellite payloads and space avionics
3.6 Annealing and Stress Relief
PEEK parts can experience residual stress that leads to deformation hours or days after molding—particularly critical for parts used in aircraft sensor housings. Ansix addresses this through:
Controlled Slow Cooling: Parts are cooled gradually after ejection to minimize internal stresses.
Post-Molding Annealing: For critical applications, parts undergo a controlled annealing process to relieve residual stresses and ensure long-term dimensional stability.
Raw Material Pre-Annealing: For machined PEEK components, Ansix can anneal raw PEEK rods or plates before machining to reduce the risk of stress-induced distortion.
Section IV: Full-Process Service – Reducing Customer Management Costs
4.1 Early Intervention – Design for Manufacturability (DFM) Reports
Before any tooling commitment, Ansix provides a comprehensive mold feasibility analysis report that includes:
Draft angle recommendations – Optimized for easy ejection without part damage
Wall thickness optimization – Balancing strength, weight, and moldability
Gate location recommendations – Minimizing weld lines and stress concentrations
Ejector pin mark location allowances – Ensuring visible marks are placed in non-critical areas
Customer Value: Identifying and resolving manufacturability issues before tooling is cut prevents costly redesigns and delays. Early DFM evaluation, especially for high-performance thermoplastics like PEEK, plays a critical role in controlling cost, quality, and production risk.
4.2 Trial Molding and Sampling
Ansix provides T0 through T3 trial samples, with each iteration accompanied by a detailed improvement report.
Fast Insert Change Capability: Ansix can quickly replace inserts to validate different design approaches without the cost and time of building an entirely new mold.
4.3 Low-Volume Validation
Before full-scale production, Ansix offers 100–500 shot trial production runs to:
Statistically validate yield rates
Confirm process capability (CPK)
Verify dimensional stability
Ensure all quality criteria are met
Customer Value: This approach eliminates the risk of committing to full production before the process is fully validated and stable.
4.4 Maintenance and Spare Parts
Spare Parts Kit: Ansix provides a comprehensive kit of wear parts (ejector pins, core inserts) with every mold delivery.
Scheduled Maintenance: Preventive maintenance is performed every 200,000 mold cycles.
Lifetime Repair Commitment: Mold repairs are provided at cost for the lifetime of the tool.
2000-Cycle Aging Test: Before delivery, every mold undergoes a 2,000-cycle aging test with a detailed wear report provided to the customer.
Section V: Differentiated Competitive Advantages – Addressing Common Industry Pain Points
5.1 Mold Reliability and Maintenance
Common Customer Complaint Ansix's Solution
Frequent mold repairs disrupting production 3-year structural warranty (excluding normal wear parts) + 2,000-cycle aging test with wear report
Long repair lead times In-house EDM and electrode machining—24-hour restoration for welding/insert replacement
5.2 Flash and Secondary Finishing Costs
Common Customer Complaint Ansix's Solution
Excessive flash, high deburring costs 0.005mm fit precision on parting lines; self-locking clamping force compensation; flash控制在 0.03mm以内
5.3 Dimensional Consistency
Common Customer Complaint Ansix's Solution
Inconsistent dimensions batch-to-batch Ultrasonic wall thickness sensors with real-time packing pressure compensation; in-mold temperature/pressure sensors enabling closed-loop control
5.4 Cycle Time and Energy Efficiency
Advanced heating technologies can reduce cycle times by up to 40% and save 30% energy per shot compared to conventional molding. Ansix incorporates such technologies where applicable to improve production efficiency and reduce per-part costs.
Section VI: PEEK Aviation Connector Housings – Material and Application Overview
6.1 Why PEEK for Aviation Connector Housings?
PEEK (Polyether-Ether-Ketone) has emerged as the material of choice for aviation connector housings due to its exceptional property profile:
Thermal Performance: PEEK maintains mechanical properties from -60°C to +250°C continuous service temperature. This ensures reliable electrical connections across the extreme temperature ranges encountered in aerospace applications.
Mechanical Strength: High strength and rigidity make PEEK connectors durable and resistant to external damage, ensuring long-term reliability.
Chemical Resistance: PEEK resists aviation fluids, hydraulic oils, fuels, and de-icing chemicals—critical for components exposed to harsh operating environments.
Radiation Resistance: PEEK provides superior radiation resistance while maintaining low outgassing properties, making it ideal for satellite payloads and space avionics.
Weight Reduction: PEEK's high strength-to-weight ratio enables significant weight savings compared to metal housings—a critical factor in aerospace fuel efficiency.
Electrical Insulation: Excellent dielectric properties ensure signal integrity and prevent electrical leakage.
Low Outgassing: Meets stringent aerospace requirements for minimal volatile condensable materials in vacuum environments.
6.2 Common Applications
PEEK connector housings are used across the aerospace industry in:
Avionics systems
Engine monitoring systems
Satellite electronics
Aerospace sensor assemblies
Lightweight electrical systems
Wire harness insulation
Fuel system components
6.3 Material Grades and Specifications
Ansix works with all major PEEK grades, including:
Unfilled PEEK – General-purpose, high-performance
Glass-Filled PEEK (30% GF) – Enhanced stiffness and dimensional stability
Carbon-Filled PEEK – Enhanced wear resistance and thermal conductivity
Bearing-Grade PEEK – Modified for low friction and wear applications
The global PEEK connector market is experiencing significant growth, with the aerospace PEEK material market surpassing $750 million in 2025 and exhibiting a 15% CAGR, driven by next-generation aircraft weight reduction and extreme environment performance requirements.
Section VII: Ansix's Comprehensive Manufacturing Process – From Concept to Delivery
7.1 Project Initiation and Planning
Every PEEK machining of aviation connector housings project begins with a structured initiation phase:
Customer Requirements Analysis: Understanding application environment, performance requirements, regulatory standards (AS9100, NADCAP), and production volumes.
Material Selection Consultation: Based on operating temperature, chemical exposure, mechanical loads, and cost targets, Ansix recommends the optimal PEEK grade and any required modifications.
Feasibility Assessment: Evaluation of part geometry, tolerance requirements, and production economics.
7.2 Design and Development
Mold Flow Analysis (MFA): Advanced simulation to optimize filling patterns, minimize weld lines, and predict shrinkage.
3D Modeling and Design Review: Collaborative design reviews with customers to finalize part geometry, gate locations, and ejector pin placement.
DFM Report: Comprehensive manufacturability analysis delivered before tooling commitment.
7.3 Mold Manufacturing
Steel Selection and Procurement: Sourcing of certified mold steels with full material traceability.
CNC Machining: 5-axis high-speed milling for complex geometries.
EDM: Slow-wire EDM for micro-features and tight-tolerance details.
Heat Treatment: Precision heat treatment with controlled quenching and tempering cycles.
Fitting and Assembly: Precision assembly with 0.005mm fit accuracy on parting surfaces.
Polishing and Surface Finishing: Achieving required surface finishes, including high-gloss (Ra <0.05μm) for aesthetic or transparent applications.
7.4 Mold Validation
T0 Trial: First trial shot to verify basic mold functionality.
T1–T3 Optimization: Iterative improvements based on dimensional measurement and visual inspection.
2000-Cycle Aging Test: Extended run to validate durability and identify any wear issues.
Full-Dimension Report: Comprehensive measurement report with CPK analysis for all critical dimensions.
7.5 Production Qualification
Material Drying: PEEK pellets dried at 150–200°C for 6–8 hours to achieve <0.02% moisture content.
Process Setup: Injection parameters established and locked in MES.
First-Article Inspection: Full dimensional and visual inspection of first production parts.
Process Capability Study: Statistical validation showing CPK ≥ 1.33 for critical dimensions.
7.6 High-Volume Production
Continuous Process Monitoring: Real-time monitoring of temperature, pressure, velocity, and position.
In-Process Inspection: Regular sampling and measurement throughout production runs.
Last-Article Inspection: Verification that final parts meet all specifications.
Packaging: Custom packaging designed to protect parts during transport and storage.
7.7 Delivery and After-Sales Support
On-Time Delivery: Commitment to meet agreed delivery schedules.
Spare Parts Kit: Wear parts provided with every mold.
Technical Support: Engineering support for any production issues.
Lifetime Repair Service: Mold repairs at cost for the lifetime of the tool.
Section VIII: Cost Reduction – Ansix's Value Creation Engine
8.1 Material Cost Optimization
Hot Runner Systems: Eliminate cold runner waste, reducing material consumption by 15–30% for multi-cavity molds.
Precise Shot Size Control: Servo-electric machines deliver accurate shot sizes, minimizing material waste.
Regrind Management: Systematic collection and reintroduction of regrind material where specifications permit.
8.2 Process Efficiency Optimization
Cycle Time Reduction: Through optimized cooling systems and process parameters, Ansix achieves cycle time reductions of up to 40% compared to conventional processing.
Energy Efficiency: All-servo electric machines consume significantly less energy than hydraulic alternatives—up to 30% energy savings per shot.
Automation Integration: Robotic part handling and automated inspection reduce labor costs and improve consistency.
8.3 Quality Cost Reduction
Zero-Defect Manufacturing: Through rigorous process control and real-time monitoring, Ansix minimizes scrap and rework.
First-Time Quality: Comprehensive DFM and validation processes ensure that production ramps up quickly and efficiently.
Reduced Inspection Costs: High process capability (CPK ≥1.33) enables reduced sampling frequencies.
8.4 Supply Chain Cost Reduction
Single-Source Responsibility: Ansix provides end-to-end service from design through delivery, reducing customer management overhead.
Consolidated Logistics: Optimized packaging and shipping reduce transportation costs.
Inventory Management: Just-in-time delivery capabilities reduce customer inventory carrying costs.
8.5 Total Cost of Ownership (TCO) Reduction
Cost Element Ansix Advantage Estimated Savings
Tooling cost Optimized mold design, right-sized tooling 10–20%
Material cost Hot runners, precise shot control 15–30%
Production cost Cycle time optimization, automation 20–40%
Quality cost High CPK, reduced scrap 30–50%
Maintenance cost Durable tooling, in-house repair 20–40%
Logistics cost Consolidated shipping, JIT delivery 10–20%
Section IX: Ansix's Industry Experience and Reliability
With over 28 years of manufacturing experience, Ansix has developed deep expertise in PEEK machining of aviation connector housings. This experience translates into:
Proven Solutions: Ansix has successfully delivered thousands of PEEK connector housing projects across commercial aviation, military aerospace, and space applications.
Process Knowledge: Deep understanding of PEEK's unique processing characteristics—its high melt temperature, crystalline behavior, and tendency toward stress-induced distortion.
Regulatory Compliance: Experience meeting stringent aerospace quality requirements, including AS9100 and customer-specific standards.
Continuous Improvement: Ongoing investment in advanced equipment, process optimization, and employee training.
Global Supply Chain: Established relationships with leading PEEK resin suppliers ensure material availability and quality.
Conclusion: The Ansix Difference
Ansix Tech's leadership in PEEK machining of aviation connector housings is built on a foundation of technical excellence, process discipline, and unwavering customer focus. By systematically translating complex manufacturing capabilities into tangible customer value—reduced costs, mitigated risks, and guaranteed reliability—Ansix has earned the trust of the world's leading aerospace manufacturers.
Key Takeaways for Customers:
Hardware You Can Trust: State-of-the-art equipment delivering 0.002mm precision and ±0.1% repeatability
Molds That Last: 500,000–1,000,000 cycle life with full material certification
Processes That Deliver: CPK ≥1.33, real-time closed-loop control, ±0.02mm batch-to-batch stability
Service That Supports: Comprehensive DFM, validation protocols, spare parts, and lifetime repair commitment
Costs That Compete: Material savings, cycle time optimization, and reduced total cost of ownership
As Ansix often reminds its customers: "A mold is not just a piece of steel—it's a money-printing machine." Every mold is designed with production robustness, optimized venting, thermal balance, and ease of setup in mind—ensuring that when it reaches the customer's production line, it runs trouble-free with minimal flash and maximum lifespan.
For a deeper understanding of how Ansix can solve your specific PEEK connector housing challenges, the company offers comprehensive DFM report walkthroughs on existing products—demonstrating exactly how weld lines, air traps, and shrinkage risks are addressed before tooling ever begins.
Ansix Tech Co Ltd
If you have any plans related to PEEK machining of aviation connector housings , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #PEEK machining of aviation connector housings #PEEK machining of aviation connector housings Material #PEEK machining of aviation connector housings Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #PEEK machining of aviation connector housings injection molding #PEEK machining of aviation connector housings injection tools #PEEK machining of aviation connector housings injection moulds #PEEK machining of aviation connector housings plastic mould #PEEK machining of aviation connector housings plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #PEEK machining of aviation connector housings injection molding Customized #Ansix mold factory #PEEK machining of aviation connector housings china #PEEK machining of aviation connector housings molds #injection factory for PEEK machining of aviation connector housings #PEEK machining of aviation connector housings injection molding #PEEK machining of aviation connector housings injection molding factory #injection molding company #PEEK machining of aviation connector housings injection mold companies #PEEK machining of aviation connector housings Tooling #PEEK machining of aviation connector housings mold limited #Ansix mold china #Ansix companies for PEEK machining of aviation connector housings #Ansix company China #PEEK machining of aviation connector housings facotry #Ansix Tech #Ansix Tech mould #PEEK machining of aviation connector housings injection moulding #PEEK machining of aviation connector housings injection moulding company #Ansix PEEK machining of aviation connector housings parts injection mold companies #PEEK machining of aviation connector housings injection molding companies china #PEEK machining of aviation connector housings china factory #Ansix moulding companies #Ansix molding company #PEEK machining of aviation connector housings injection moulding facotry #Ansix Tech mold #PEEK machining of aviation connector housings mould #PEEK machining of aviation connector housings plastic injection molding #ansix plastic mold #PEEK machining of aviation connector housings Mold manufacturing #PEEK machining of aviation connector housings parts manufacturing #PEEK machining of aviation connector housings plastic parts factory #PEEK machining of aviation connector housings injection parts mold #PEEK machining of aviation connector housings PRECISION MANUFACTURING #PEEK machining of aviation connector housings TOOL #China PEEK machining of aviation connector housings mold #PEEK machining of aviation connector housings Material injection moulding china #PEEK machining of aviation connector housings mould china #china precision mold #PEEK machining of aviation connector housings Material mold in china #PEEK machining of aviation connector housings mold china #PEEK machining of aviation connector housings Precision molds #High-precision molds #PEEK machining of aviation connector housings High-precision tool #Injection molds #PEEK machining of aviation connector housings Factory #PEEK machining of aviation connector housings Company #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #PEEK machining of aviation connector housings Company #PEEK machining of aviation connector housings Factory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #PEEK machining of aviation connector housings Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #PEEK machining of aviation connector housings Large Injection Mold Manufacturer #PEEK machining of aviation connector housings Plastic Mold Factory #Injection Mold #Plastic Mold