 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


PEEK solenoid valve body injection mold
FEATURES
Hard Capabilities – The Foundation of Customer Trust
Mold Processing Equipment
Ansix Tech is equipped with state-of-the-art mold manufacturing machinery that forms the backbone of precision engineering:
Five-Axis High-Speed Machining Centers – These advanced systems enable the machining of complex curved surfaces with an accuracy of 0.002mm. This level of precision ensures that product parting lines remain smooth and burr-free, directly translating to superior surface finish and reduced post-processing requirements for customers.
Slow-Wire EDM (Electrical Discharge Machining) – Capable of machining fine micro-holes and narrow slots as small as 0.03mm, this equipment prevents thin-wall deformation—a critical consideration for solenoid valve body components that require intricate internal geometries and precise port dimensions.
Precision Grinding and Polishing Equipment – Ensures mirror-finish surfaces on mold cavities, essential for achieving the high-gloss requirements of certain PEEK applications.
-
Mold Description
Product Materials:
PEEK
Mold Material:
S136ESR
Number of Cavities:
2
Glue Feeding Method:
COLD runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
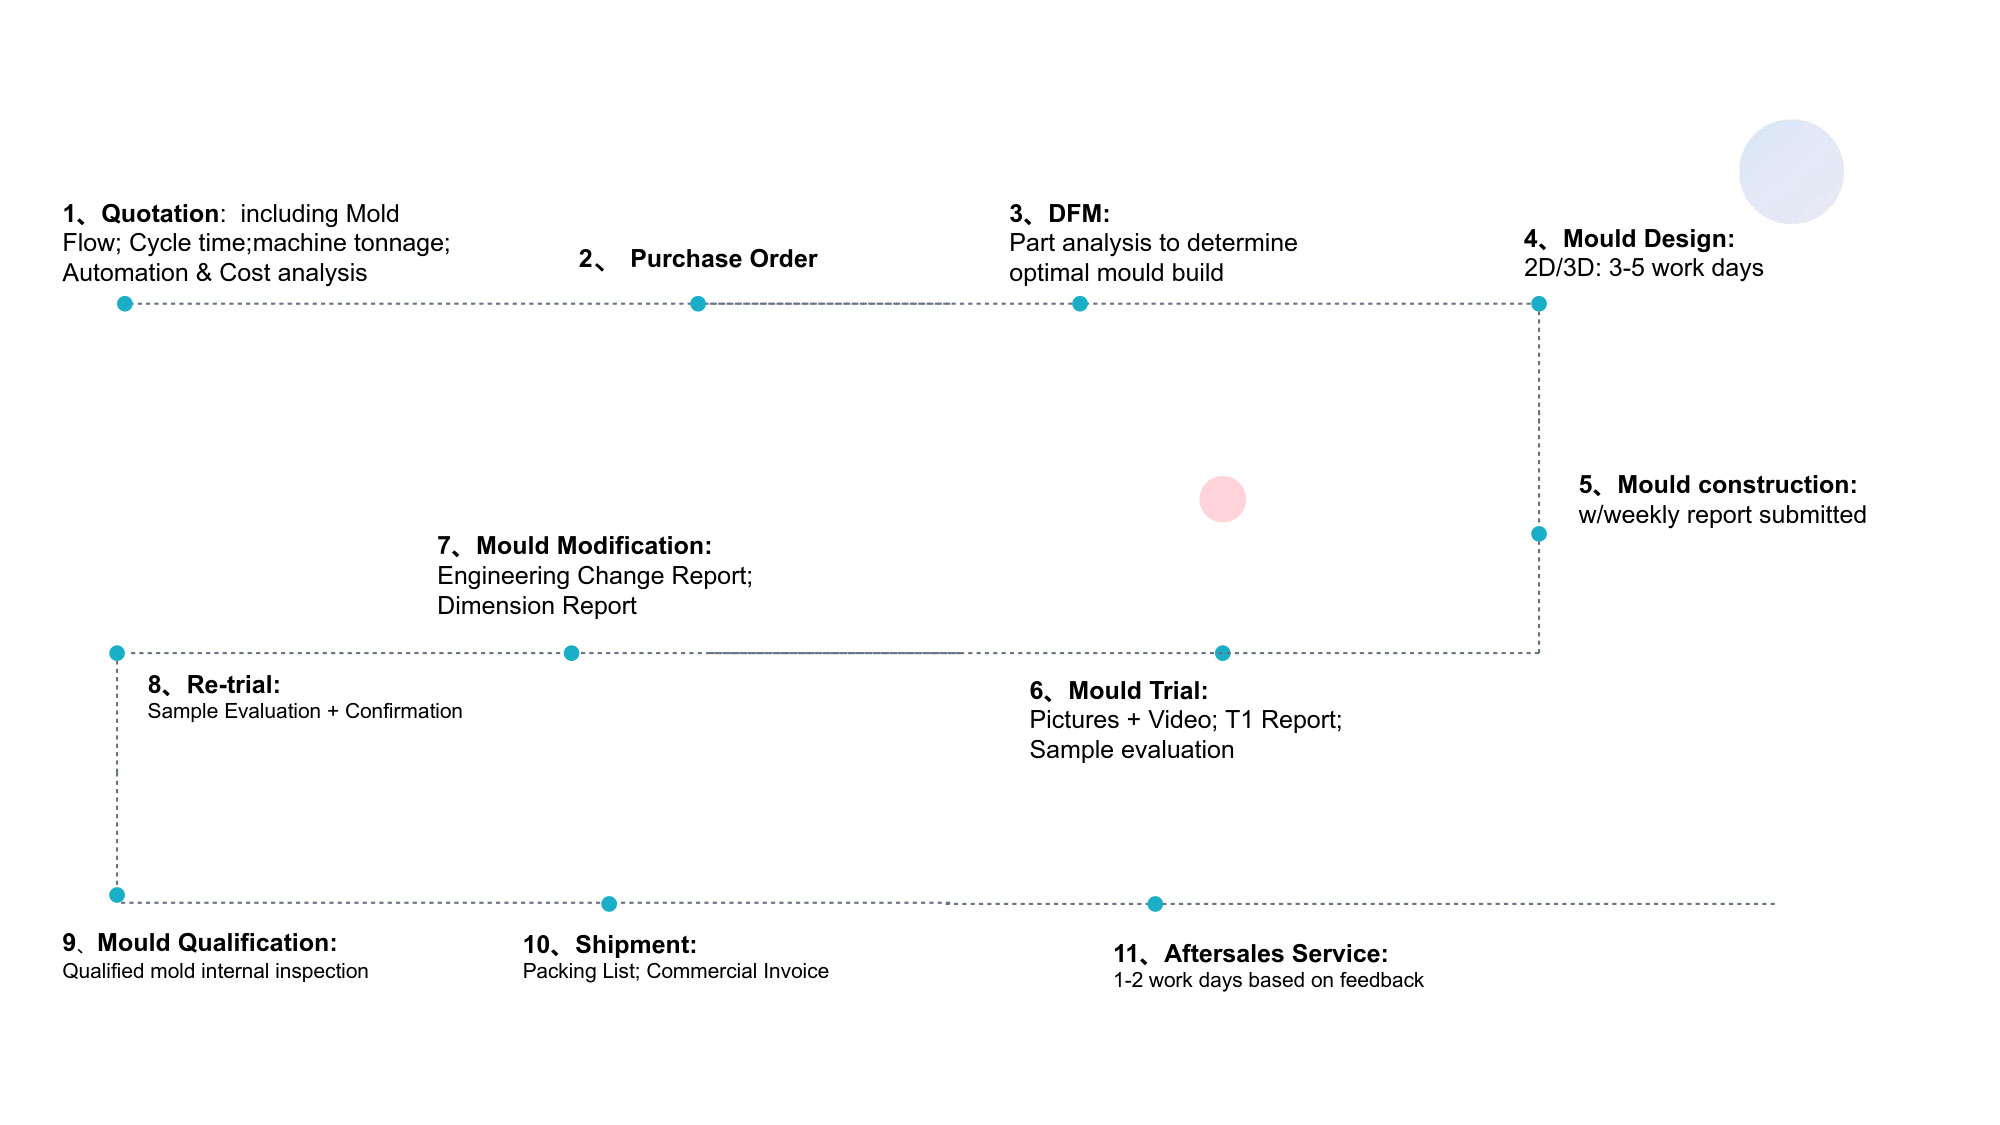
- The mold manufacturing process and product material selection
Injection Molding Machine Fleet
Ansix Tech operates a comprehensive range of injection molding machines with clamping forces spanning from 30 tons to 4,000 tons, covering a broad spectrum of product sizes from miniature precision components to large-scale industrial parts.
All-Servo Motor Drive Systems – Every machine is equipped with all-servo electric drives, delivering stable repeatability accuracy of ±0.1% . This means that every single shot in mass production maintains consistent quality—batch after batch, shift after shift.
High-Temperature Molding Capability – PEEK requires barrel temperatures between 360°C and 400°C (680°F to 752°F) and mold temperatures of 160°C to 200°C. Ansix Tech’s machines are specifically equipped with high-temperature screws, heating systems, and thermal insulation to handle these extreme conditions reliably.
Injection Pressure Range – Machines are capable of delivering injection pressures from 100 MPa to 200 MPa (14,500 to 29,000 psi), ensuring complete cavity fill even for complex, thin-walled PEEK solenoid valve body geometries.
Inspection and Metrology Equipment
Coordinate Measuring Machines (CMM) – Every mold undergoes comprehensive dimensional inspection before delivery. Full dimensional reports are provided, with critical dimension CPK ≥ 1.33—a statistical measure demonstrating that the process is highly capable and stable.
Optical Imaging and Vision Inspection Systems – Used for surface defect detection and precision measurement of fine features, ensuring that every component meets the most stringent quality standards.
Ultrasonic Wall Thickness Sensors – Installed on injection molding machines to provide real-time feedback on wall thickness fluctuations, with automatic compensation of holding pressure to maintain dimensional consistency.
-
Mold Manufacturing – Core Competitiveness Delivered Through Measurable Metrics
Mold Life Expectancy
Customers’ primary concerns are mold life, precision, delivery time, and repair costs. Ansix Tech addresses these with clear, data-backed commitments:
Dimension Technical Specification Customer Value
Mold Life Steel selection based on application: P20 for mold bases; S136, 2344, 2343, 8407, SKD11/61, DC53, M340, 4Cr13, 9Cr18, NAK80, H13 for mold cores 50万模次 (500,000 shots) for glass-fiber reinforced materials; 100万模次 (1,000,000 shots) for standard plastics. Extended mold life means lower tooling amortization cost per part
Achievable Tolerances Standard structural components: ±0.05mm; Precision gears/medical components: ±0.005mm Guaranteed dimensional accuracy eliminates assembly fit issues and reduces scrap rates
Material Certification Full mold steel material reports and heat treatment curves provided Complete traceability and quality assurance
Mold Types Hot runner (reduces material waste), stack molds (doubles productivity), two-shot/multi-material molds, high-gloss molds (Ra<0.05μm for transparent components) Optimized for specific production requirements—reduced waste, higher output, or superior aesthetics
Gate System Design Mold flow analysis pre-identifies weld line and gas trap locations; gate count and placement optimized for balanced filling Eliminates defects before steel is cut, reducing trial-and-error iterations
Delivery Standards Simple molds: 10 days; Medium complexity: 25-45 days; Expedited: 20 days (with full validation maintained) Predictable timelines enable customers to plan production schedules with confidence
Mold Design for PEEK-Specific Challenges
PEEK presents unique challenges due to its high melting point (approximately 343°C) and processing temperatures of 350°C to 400°C. Ansix Tech’s mold design addresses these challenges through:
Thermal Expansion Management – The mold design carefully considers the coefficient of thermal expansion of the mold frame, nuts, and all sliding components to maintain precise clearances at operating temperatures.
Insulation Measures – Special heat insulation boards and high-temperature-resistant components are integrated into the mold design to protect surrounding equipment and maintain process stability.
Specialized Cooling Systems – PEEK has low thermal conductivity (approximately 0.25 W/(m·K) ), requiring specialized cooling approaches. Ansix Tech employs:
High-thermal-conductivity materials such as beryllium copper for inserts
Spiral cooling channel designs for uniform temperature distribution
Mold temperature uniformity控制在 ±5°C 以内
Cooling time set at 2-3 times that of conventional plastics to ensure proper crystallization
Gate and Runner System Design
Multi-Point Gating – To minimize warpage and ensure balanced filling, Ansix Tech employs multi-point gating strategies rather than single-point gating, which can create uneven flow patterns.
Hot Runner Systems – Where applicable, hot runner systems reduce material waste and improve cycle times while maintaining melt temperature consistency.
Section III: Injection Molding Process Control – Eliminating Customer Quality Anxiety
Customers fear: sink marks, flash, dimensional instability, and batch-to-batch color variation. Ansix Tech systematically addresses each concern.
Process Standardization and Digital Control
MES-Integrated Process Lock – All injection molding machines are networked, with molding parameters (temperature, pressure, speed, and time) locked in the MES (Manufacturing Execution System). Only authorized engineers can make adjustments. First-article and last-article inspection is performed for every batch, ensuring process consistency from start to finish.
Dimensional Stability Control
Zone Temperature Control – Molds are equipped with zone-specific temperature controllers for the core and cavity, maintaining temperature differences within 2°C to minimize warpage and distortion.
Real-World Data – For comparable bracket products, three consecutive production batches over one week showed critical hole spacing fluctuation ≤ 0.02mm—demonstrating exceptional dimensional stability.
Packing and Cooling Optimization – Optimized packing pressure profiles and cooling profiles are developed for each product to manage shrinkage and warpage effectively.
Surface Quality Standards
Requirement Achievable Standard
Transparent components No bubbles, no flow marks
Electroplated components No gas marks
High-gloss components Surface roughness Ra ≤ 0.2μm
For products requiring painting or printing, Ansix Tech provides compensation for deformation during mold design, achieving print registration accuracy within ±0.1mm.
Shrinkage and Warpage Control
PEEK exhibits unique shrinkage behavior—reinforcement reduces overall shrinkage but increases anisotropy, which can introduce warpage if not carefully managed. Ansix Tech controls this through:
Mold Flow Analysis – Comprehensive simulation predicts volumetric shrinkage, sink mark depth, residual stress, and warpage before tooling begins.
Optimized Crystallization – Maintaining mold temperatures above 160°C ensures complete and uniform crystallization, preventing post-mold warpage that can occur days or weeks after molding.
Annealing Processes – Post-molding annealing stabilizes dimensions, eliminating “post-mold warpage” that can appear long after production.
Special Material Capabilities
Ansix Tech has extensive experience with a wide range of engineering thermoplastics, including:
PC/ABS – Automotive interior components
PC – Transparent and impact-resistant applications
PPS + 40% GF – High-temperature, chemical-resistant applications
PEEK – High-performance valve bodies, seals, and bearings
PTFE/PFA – Corrosion-resistant components
PA6 + GF30 – Structural components requiring high strength
PBT – Electrical and electronic applications
PEI/PPS/LCP – High-temperature electronic components
Liquid Silicone Rubber (LSR) – Flexible sealing applications
Flame Retardancy – Components can meet UL94 V-0 ratings for wire spools and housings.
Weather Resistance – Materials can pass UV testing of 3,000 hours without discoloration.
Section IV: Full-Process Service – Reducing Customer Management Costs
Early-Stage Engagement (DFM Reports)
Pre-Contract Feasibility Analysis – Before signing any agreement, Ansix Tech provides a comprehensive Design for Manufacturability (DFM) report that includes:
Draft angle recommendations (most PEEK components benefit from 1° to 2° draft angles)
Wall thickness optimization suggestions
Gate location recommendations
Ejector pin mark position allowances
Identification of potential manufacturing issues before mold design begins
This early engagement prevents costly design revisions after tooling has commenced—saving customers significant time and money.
Trial Molding and Sampling
T0 to T3 Trial Samples – Ansix Tech provides samples through multiple trial stages (T0 through T3), each accompanied by a detailed improvement report.
Quick Insert Change Capability – The ability to rapidly change inserts enables validation of different design approaches without rebuilding the entire mold—significantly reducing development costs and timelines.
Small-Batch Validation
Pre-Production Validation Runs – Before full-scale production, Ansix Tech provides 100 to 500-shot trial runs to validate yield rates and CPK values. Production only proceeds to full scale once stability is confirmed—eliminating the risk of large-scale quality issues.
Maintenance and Spare Parts
Spare Parts Kits – Wear parts (ejector pins, core inserts) are delivered with the mold, ensuring immediate availability when needed.
Scheduled Maintenance – Maintenance is performed every 200,000 shots, with lifetime repair service available at cost.
In-House Repair Capability – Ansix Tech maintains in-house electrode machining centers and EDM workshops, meaning mold repairs rarely leave the facility. Standard weld repair and insert replacement can be completed within 24 hours—minimizing production downtime.
Section V: Differentiated Value Proposition – Direct Answers to Common Industry Pain Points
Common Customer Complaint Ansix Tech’s Solution
Molds require frequent repairs, disrupting orders 2,000-shot aging test performed before delivery with wear reports provided; three-year mold structure warranty (excluding normal wear on consumable parts)
Excessive flash, high post-processing costs 0.005mm fit precision on parting surfaces; self-locking clamp force compensation ensures flash controlled within 0.03mm per batch—eliminating manual deburring
Inconsistent dimensions batch to batch Ultrasonic wall thickness sensors with real-time feedback and automatic holding pressure compensation; optional in-cavity temperature and pressure sensors for closed-loop control
Long repair lead times In-house electrode machining and EDM; standard repairs completed within 24 hours
PEEK Solenoid Valve Body – Product Overview and Manufacturing Process
Product Introduction
PEEK (Polyether Ether Ketone) solenoid valve bodies are critical components in demanding applications requiring:
Exceptional chemical resistance – Compatible with aggressive fluids and cleaning agents
High-temperature performance – Continuous service temperatures up to 260°C
Excellent wear resistance – Ideal for high-cycle valve applications
Low coefficient of friction – Reduces actuation forces and extends service life
Dimensional stability – Maintains precision across wide temperature ranges
These properties make PEEK the material of choice for solenoid valve bodies in automotive, aerospace, oil and gas, medical, and semiconductor industries.
Raw Material Selection
Ansix Tech works with leading PEEK resin suppliers including Victrex, Solvay, and Evonik, offering various grades:
Unfilled PEEK – For general-purpose applications requiring excellent mechanical properties
30% Glass-Fiber Reinforced PEEK – Enhanced stiffness and creep resistance
30% Carbon-Fiber Reinforced PEEK – Superior strength-to-weight ratio and wear resistance
PEEK with PTFE blend – Enhanced wear resistance and lower friction
Material selection is guided by application requirements, with full material certifications and traceability provided.
Mold Flow Analysis (DFM)
Comprehensive mold flow analysis is performed for every PEEK solenoid valve body project, addressing:
Filling pattern optimization – Ensuring complete cavity fill without short shots
Weld line prediction and mitigation – Critical for pressure-retaining components
Gas trap identification – Preventing burn marks and voids
Shrinkage and warpage prediction – Enabling proactive compensation in mold design
Injection Molding Process Parameters
Parameter Typical Range Critical Consideration
Barrel Temperature 360°C – 400°C Precise control essential; too low causes incomplete fill, too high causes material degradation
Mold Temperature 160°C – 200°C Critical for crystallization; below 160°C causes incomplete crystallization and warpage
Injection Pressure 100 – 200 MPa High pressure ensures complete fill of detailed features
Holding Pressure 30 – 150 bar Extended holding until gate freeze prevents sink marks
Injection Speed Moderate to high Prevents premature freezing and ensures complete cavity fill
Cooling Time 2-3× conventional plastics PEEK’s low thermal conductivity requires extended cooling
Quality Control and Assurance
In-Process Controls:
Real-time process parameter monitoring via MES
Automatic reject systems for out-of-tolerance parts
Vision inspection for surface defects
Post-Process Validation:
100% critical dimension inspection
CMM verification of key features
Pressure testing for valve body integrity
Surface finish verification
Packaging and Delivery
Clean Packaging – Components are packaged in clean environments to prevent contamination, with anti-static materials where required.
Traceability – Each batch is fully traceable to raw material lots, production parameters, and inspection records.
Rapid Delivery – With in-house mold manufacturing and dedicated production cells, Ansix Tech delivers PEEK solenoid valve bodies with industry-leading lead times.
Cost Reduction Strategy – Delivering Hard Savings
Ansix Tech reduces customer costs through three primary vectors:
Material Cost Optimization
Hot runner systems reduce material waste by eliminating cold runner scrap
Precise shot size control minimizes material consumption per part
Material selection guidance ensures the right grade for each application—never over-specifying
Process Efficiency Optimization
Cycle time reduction through optimized cooling channel design and process parameters
Automation integration reduces labor costs and improves consistency
Stack mold technology doubles output per machine cycle for appropriate applications
Quality Cost Reduction
First-pass yield > 98% eliminates rework and scrap costs
Dimensional stability eliminates assembly issues and field failures
Extended mold life reduces tooling amortization cost per part
Conclusion: Why Ansix Tech Is the Industry Leader
Ansix Tech has earned its position as a market leader in PEEK solenoid valve body injection molds through:
Uncompromising technical capability – State-of-the-art equipment, precision metrology, and deep PEEK processing expertise
Customer-centric value delivery – Every technical decision is framed in terms of customer benefit: cost reduction, risk mitigation, and quality assurance
Full-process service – From DFM through production to after-sales support, reducing customer management burden
Proven reliability – 28+ years of experience, with documented performance data on mold life, dimensional stability, and process capability
Transparent communication – Clear metrics, honest assessments, and data-backed commitments
“To our valued customers: a mold is not just a piece of steel—it is a money-printing machine. When we design a mold, we simultaneously plan for injection molding robustness, venting paths, and thermal balance—ensuring that when it reaches your production floor, it is ready for drop-in installation with minimal flash and maximum longevity. We invite you to experience our full-process DFM review on an existing product—you will see firsthand how we proactively eliminate weld lines, gas traps, and shrinkage risks before they become problems.”
This document represents Ansix Tech’s comprehensive capabilities in PEEK solenoid valve body injection mold manufacturing. For specific project inquiries, technical discussions, or to schedule a DFM review, please contact our engineering team.
Ansix Tech Co Ltd
If you have any plans related to PEEK solenoid valve body injection mold , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #PEEK solenoid valve body injection mold #PEEK solenoid valve body injection mold Material #PEEK solenoid valve body injection mold Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #PEEK solenoid valve body injection mold injection molding #PEEK solenoid valve body injection mold injection tools #PEEK solenoid valve body injection mold injection moulds #PEEK solenoid valve body injection mold plastic mould #PEEK solenoid valve body injection mold plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #PEEK solenoid valve body injection mold injection molding Customized #Ansix mold factory #PEEK solenoid valve body injection mold china #PEEK solenoid valve body injection mold molds #injection factory for PEEK solenoid valve body injection mold #PEEK solenoid valve body injection mold injection molding #PEEK solenoid valve body injection mold injection molding factory #injection molding company #PEEK solenoid valve body injection mold injection mold companies #PEEK solenoid valve body injection mold Tooling #PEEK solenoid valve body injection mold mold limited #Ansix mold china #Ansix companies for PEEK solenoid valve body injection mold #Ansix company China #PEEK solenoid valve body injection mold facotry #Ansix Tech #Ansix Tech mould #PEEK solenoid valve body injection mold injection moulding #PEEK solenoid valve body injection mold injection moulding company #Ansix PEEK solenoid valve body injection mold parts injection mold companies #PEEK solenoid valve body injection mold injection molding companies china #PEEK solenoid valve body injection mold china factory #Ansix moulding companies #Ansix molding company #PEEK solenoid valve body injection mold injection moulding facotry #Ansix Tech mold #PEEK solenoid valve body injection mold mould #PEEK solenoid valve body injection mold plastic injection molding #ansix plastic mold #PEEK solenoid valve body injection mold Mold manufacturing #PEEK solenoid valve body injection mold parts manufacturing #PEEK solenoid valve body injection mold plastic parts factory #PEEK solenoid valve body injection mold injection parts mold #PEEK solenoid valve body injection mold PRECISION MANUFACTURING #PEEK solenoid valve body injection mold TOOL #China PEEK solenoid valve body injection mold mold #PEEK solenoid valve body injection mold Material injection moulding china #PEEK solenoid valve body injection mold mould china #china precision mold #PEEK solenoid valve body injection mold Material mold in china #PEEK solenoid valve body injection mold mold china #PEEK solenoid valve body injection mold Precision molds #High-precision molds #PEEK solenoid valve body injection mold High-precision tool #Injection molds #PEEK solenoid valve body injection mold Factory #PEEK solenoid valve body injection mold Company #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #PEEK solenoid valve body injection mold Company #PEEK solenoid valve body injection mold Factory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #PEEK solenoid valve body injection mold Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #PEEK solenoid valve body injection mold Large Injection Mold Manufacturer #PEEK solenoid valve body injection mold Plastic Mold Factory #Injection Mold #Plastic Mold