 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


PPSU mouse cage
FEATURES
Foundational Hard Capabilities – Building Customer Trust Through Infrastructure
1.1 Mold Processing Equipment
Ansix operates a comprehensive suite of precision machining equipment that forms the backbone of its mold manufacturing capabilities:
Five-Axis High-Speed Machining Centers: These machines enable the processing of complex curved surfaces with accuracy reaching 0.002mm. For PPSU mouse cage products, this translates directly to smooth, burr-free parting lines—a critical requirement for laboratory animal housing where sharp edges can cause injury to animals or compromise sterile environments.
Slow Wire EDM (Electrical Discharge Machining): This technology enables the creation of micro-features including 0.03mm fine holes and narrow slots. For mouse cage designs requiring ventilation holes, water bottle interfaces, or intricate locking mechanisms, this capability ensures precision without inducing thin-wall deformation.
Electrode Machining Center and EDM Workshop: Ansix maintains in-house electrode production and spark erosion capabilities, ensuring that mold repairs and modifications can be completed without outsourcing—typically restoring production within 24 hours for routine repairs.
-
Mold Description
Product Materials:
PPSU
Mold Material:
S136ESR
Number of Cavities:
1
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
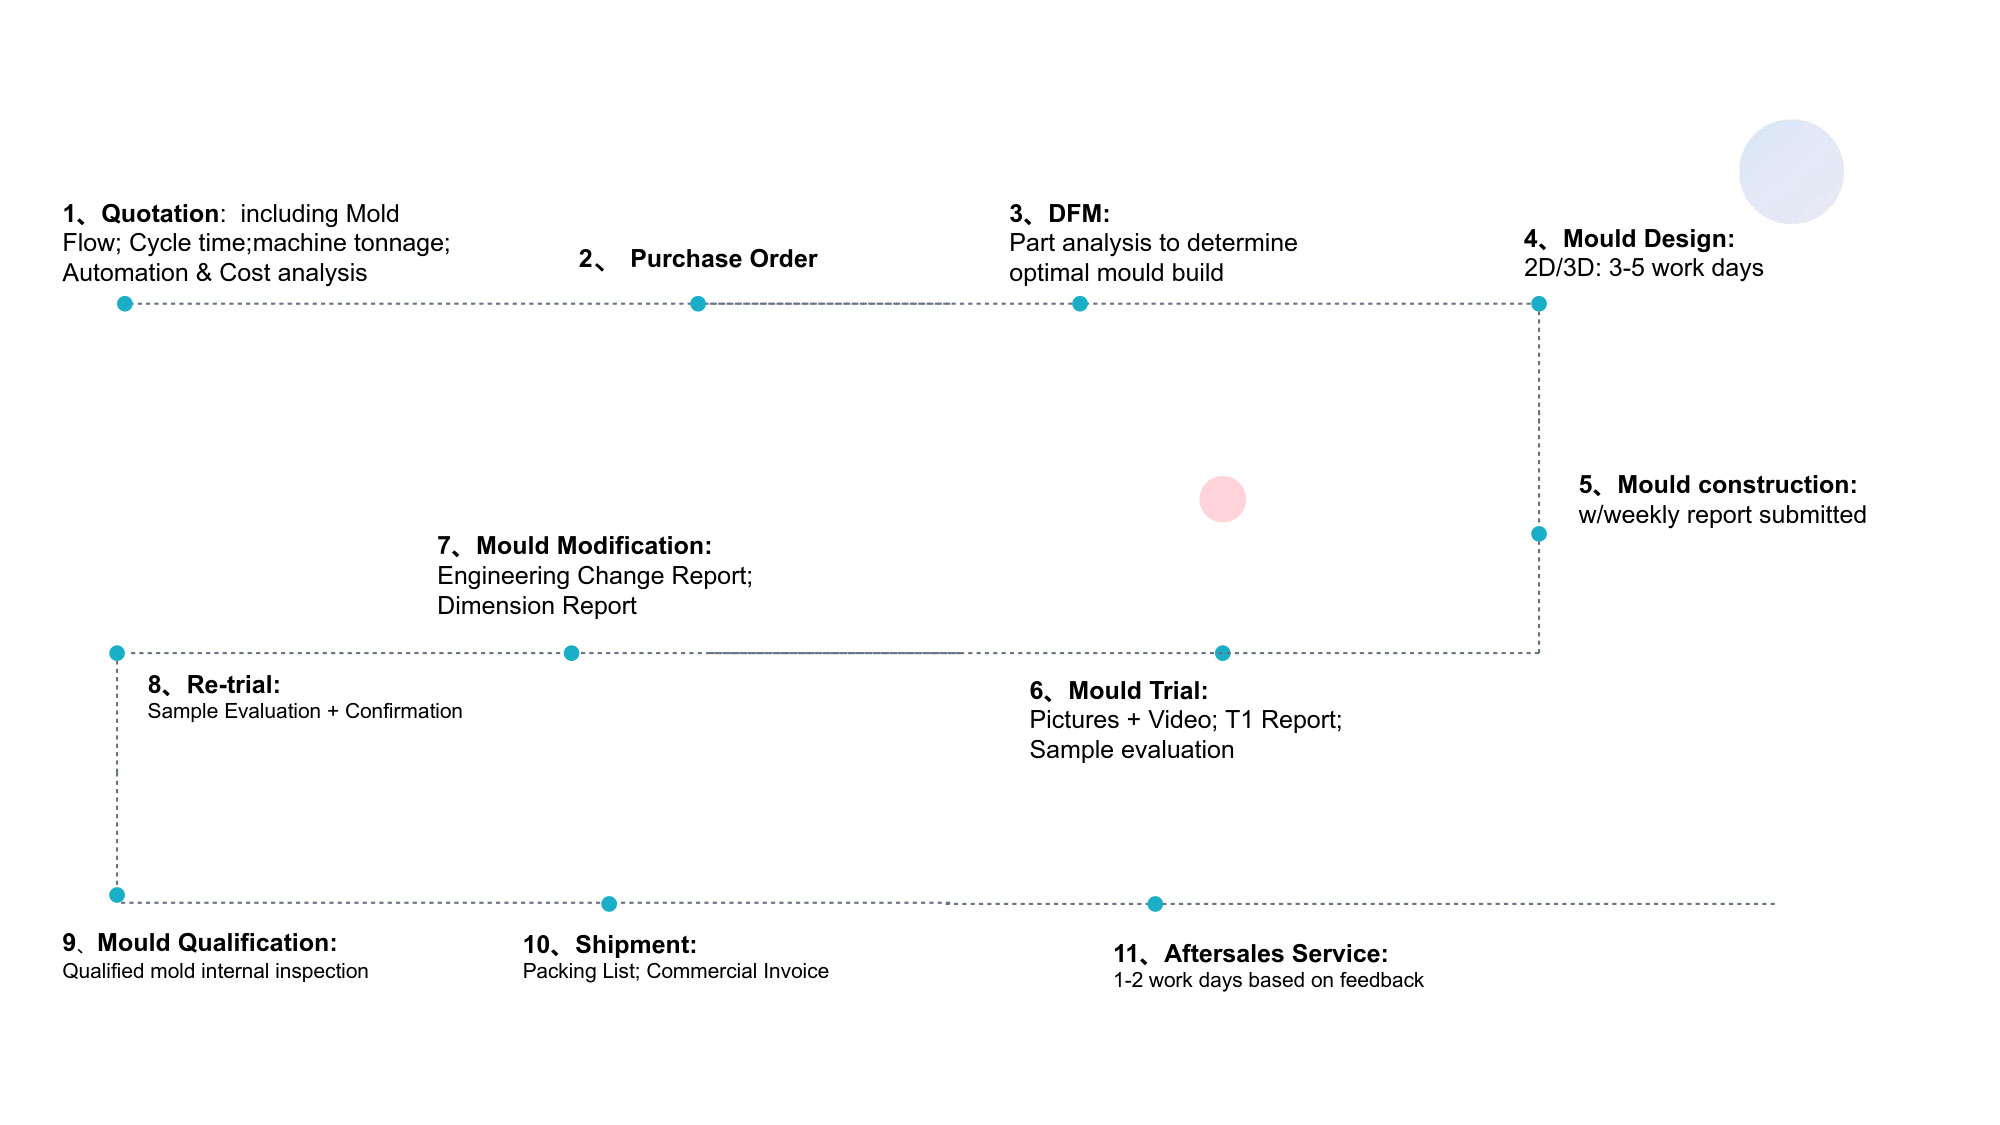
- The mold manufacturing process and product material selection
Injection Molding Machine Fleet
Ansix's injection molding press lineup spans 30 tons to 4,000 tons of clamping force, covering the full spectrum of PPSU mouse cage sizes—from small individual mouse cages to large rack-compatible systems.
All-Servo Electric Drive Systems: Every machine is equipped with all-servo motor drives, delivering repetitive precision of ±0.1% . This means that every shot is consistent across million-plus production runs—a critical requirement when customers need batch-to-batch uniformity for regulatory compliance and animal welfare standards.
1.3 Inspection and Metrology Equipment
Coordinate Measuring Machines (CMM) : Each mold undergoes full dimensional reporting before shipment, with critical dimensions verified at CPK ≥ 1.33—demonstrating that the process is statistically capable of meeting specifications.
Optical Imaging Inspection Systems: These systems enable rapid, non-contact measurement of complex geometries, ensuring that every feature—from ventilation slot dimensions to lid sealing surfaces—meets design intent.
-
Mold Manufacturing Core Competitiveness – Speaking the Language of Customer Value
2.1 Mold Steel Selection and Material Science
The choice of mold steel directly impacts product quality, mold寿命, and maintenance costs. Ansix employs a strategic selection of materials based on application requirements:
Steel Grade Application Customer Value Translation
P20 Mold bases, general-purpose frameworks Cost-effective foundation with good machinability
S136 / S136H / STAVAX Stainless steel for cavities requiring high cleanliness, corrosion resistance, and mirror finish Ideal for medical-grade and food-contact applications; prevents rust and contamination in sterile environments
H13 (1.2344 / SKD61) High-temperature, wear-resistant applications Handles glass-filled abrasive resins; survives >1 million shots
2344 / 2343 / 8407 Premium hot-work tool steels Extended tool life under high-temperature PPSU processing
SKD11 / SKD61 / DC53 High-hardness wear-resistant applications Maintains dimensional stability under abrasive conditions
NAK80 Pre-hardened steel for mirror-finish applications Excellent polishability for transparent PPSU cages requiring optical clarity
M340 / 4Cr13 / 9Cr18 Corrosion-resistant stainless grades Prevents staining and pitting in autoclave environments
Performance Commitments:
Glass-fiber reinforced materials: Guaranteed 500,000 mold cycles
Unfilled plastics: Guaranteed 1,000,000 mold cycles
Documentation: Full material certificates and heat treatment curves provided with every mold
2.2 Dimensional Tolerance Capabilities
Component Type Achievable Tolerance Customer Value
Standard structural components ±0.05mm Ensures proper cage assembly and rack compatibility
Precision gears and medical-grade components ±0.005mm Enables complex locking mechanisms and precise fitments
2.3 Mold Types and Configurations
Ansix offers a comprehensive range of mold technologies:
Hot Runner Systems: Reduce material waste and cycle time by eliminating cold runner scrap
Stack Molds: Double production efficiency by molding two layers of parts simultaneously
Two-Shot / Multi-Material Molds: Enable complex geometries with multiple materials in a single cycle
High-Gloss Molds: Surface roughness Ra < 0.05μm—essential for transparent PPSU cages requiring optical clarity for animal observation
2.4 Gate and Feed System Design
Through advanced mold flow analysis, Ansix predicts weld line formation, gas trap locations, and filling imbalances before steel is cut. This proactive approach enables:
Optimization of gate count and positioning
Balanced cavity filling across multi-cavity molds
Elimination of short shots and flow marks
Reduced scrap rates in production
2.5 Lead Time Standards
Mold Complexity Standard Lead Time Expedited Option
Simple molds 10 days —
Medium-complexity molds 25–45 days 20 days (with validation steps preserved)
Complex, high-cavity molds Negotiated based on scope Accelerated engineering support available
Section III: Injection Molding Process Control – Eliminating Customer Quality Anxiety
3.1 Process Standardization and MES Integration
All injection molding machines are networked and integrated with a Manufacturing Execution System (MES) . Key process parameters—temperature, pressure, speed, and timing—are locked within the system, accessible only to authorized engineers for adjustment.
First-Article and Last-Article Inspection: Every production batch undergoes comparison between first and last shots, ensuring process stability throughout the run.
3.2 Dimensional Stability Control
PPSU is a high-performance engineering plastic known for excellent heat resistance, impact strength, and chemical durability. However, its high processing temperature (typically 300–350°C melt temperature) demands precise thermal management:
Mold Temperature Control: Ansix employs zone-controlled mold temperature controllers with temperature differential between core and cavity maintained within 2°C—significantly tighter than the industry-standard range of 120–180°C. This precision minimizes warpage and distortion.
Real-World Validation Data: For similar structural components, three consecutive production batches over one week showed critical hole spacing variation ≤ 0.02mm.
Ultrasonic Wall Thickness Monitoring: Real-time sensors provide feedback on wall thickness fluctuations, automatically compensating holding pressure to maintain dimensional consistency.
In-Mold Temperature and Pressure Sensors: Closed-loop control systems enable real-time process adjustment, ensuring every shot meets specifications.
3.3 PPSU Material Processing – Critical Parameters
PPSU is highly moisture-sensitive; inadequate drying leads to hydrolysis, splay marks, and degraded mechanical properties. Ansix adheres to rigorous drying protocols:
Parameter Specification Industry Standard Reference
Drying temperature 135–177°C 150–170°C recommended
Drying time 4–8 hours 4–6 hours typical
Maximum moisture content < 0.02% 0.05% (500 ppm) maximum
Injection Parameters:
Parameter PPSU Specification Customer Value
Melt temperature 360–400°C High temperature capability prevents degradation
Injection pressure 80–160 MPa Ensures complete cavity fill for complex geometries
Holding pressure 40–80% of injection pressure Minimizes internal stress and warpage
Mold temperature 120–180°C Promotes flow, reduces internal stress
3.4 Surface Quality and Appearance Grades
Requirement Achievable Standard Application
Transparent parts No bubbles, no flow marks Observation-grade cage bodies
Plating-ready parts No gas marks Components requiring secondary finishing
High-gloss surfaces Ra ≤ 0.2μm Premium aesthetic applications
Printing/coating readiness Registration accuracy ±0.1mm with compensated design Branded or labeled products
3.5 Special Material Processing Capabilities
Ansix has extensive production experience with a wide spectrum of engineering thermoplastics:
Material Typical Application
PC/ABS Structural components
PC Transparent cages, lids
PPS + 40% GF High-strength, high-temperature applications
PEEK Ultra-high-performance medical devices
PTFE / PFA Chemical-resistant components
PA6 + GF30 Reinforced structural parts
PBT Electrical components
PEI / PPS / LCP High-temperature, precision applications
Liquid Silicone Rubber (LSR) Seals, gaskets, soft components
Regulatory Compliance: Ansix can achieve UL94 V-0 flame ratings and 3,000-hour UV stability without discoloration.
Section IV: Full-Process Service – Reducing Customer Management Overhead
4.1 Early Intervention – Design for Manufacturability (DFM) Reports
Before any tooling commitment, Ansix provides a comprehensive DFM (Design for Manufacturability) feasibility analysis. This report includes:
Draft angle recommendations
Wall thickness optimization
Gate location analysis
Ejector pin mark location allowances
Structural reinforcement suggestions
Customer Value: Problems are identified and solved before steel is cut—eliminating costly redesigns and project delays.
4.2 Trial Molding and Sample Development
T0 to T3 Sample Stages: Ansix provides samples at each trial stage, accompanied by improvement reports.
Rapid Insert Exchange: Design iterations can be validated by swapping inserts rather than rebuilding entire molds, significantly accelerating development cycles.
4.3 Pilot Production Validation
Prior to full-scale production, Ansix offers 100–500 shot pilot runs to statistically validate yield rates and process capability (CPK). Production proceeds to mass manufacturing only after stability is confirmed.
4.4 Maintenance and Spare Parts Support
Spare Parts Kit: Each mold is delivered with a complete set of spare wear components—ejector pins, core inserts, and other consumables.
Scheduled Maintenance: Maintenance service provided every 200,000 mold cycles.
Lifetime Repair Commitment: Repairs are provided at cost for the life of the mold.
Section V: Differentiated Commitments – Addressing Common Industry Pain Points
Common Customer Complaint Ansix's Solution Quantified Customer Benefit
"Molds require frequent repairs, disrupting orders" 2,000-shot aging test before delivery with wear report; 3-year structural warranty (excluding normal consumable wear) Predictable production schedules; reduced unplanned downtime
"Excessive flash increases post-processing costs" 0.005mm fit precision on parting lines; self-locking clamp force compensation; flash controlled ≤ 0.03mm per batch Elimination of manual deburring operations
"Dimensions vary from batch to batch" Ultrasonic wall thickness sensors with automatic holding pressure compensation; in-mold temperature/pressure sensors for closed-loop control Consistent parts, reduced scrap, stable assembly
"Mold repair lead times are too long" In-house electrode machining and EDM; repairs completed without outsourcing; routine repairs restored within 24 hours Minimal production interruption
Section VI: PPSU Mouse Cage Product Overview
6.1 Material Selection Rationale
PPSU (polyphenylsulfone) is the material of choice for laboratory animal cages due to its exceptional properties:
Thermal stability: Heat deflection temperature > 180°C; withstands 134°C / 205 kPa steam sterilization
Sterilization durability: Survives 500+ autoclave cycles without deformation
Chemical resistance: Withstands acids, alkalis, and chemical disinfectants
Optical clarity: Amber-transparent for unobstructed animal observation
Biocompatibility: Non-toxic, non-harmful to laboratory animals
Impact strength: Exceptional mechanical properties for demanding laboratory environments
6.2 Product Applications
PPSU mouse cages are used in:
SPF (Specific Pathogen Free) laboratory environments
IVC (Individually Ventilated Cage) systems
Metabolic cages for urine/feces separation studies
Sterile research facilities requiring repeated autoclave cycles
Section VII: Manufacturing Workflow – End-to-End Process Excellence
7.1 Raw Material Receiving and Drying
PPSU resin (typically sourced from leading suppliers such as BASF or Syensqo) is received with full traceability. Material is dried to < 0.02% moisture content using desiccant dryers at 135–177°C for 4–8 hours—preventing hydrolysis-induced property degradation.
7.2 Mold Flow Analysis and Simulation
Using advanced CAE software, Ansix simulates:
Melt front progression
Weld line locations
Gas trap positions
Pressure distribution
Cooling uniformity
This analysis informs gate design, runner balancing, and cooling channel layout—ensuring first-shot success and minimizing trial iterations.
7.3 Mold Manufacturing
Process Flow:
CAD design with DFM review
CAM programming for five-axis machining
Rough machining (turning, milling)
Heat treatment (with full documentation)
Finish machining (five-axis, EDM, wire EDM)
Bench fitting and assembly
Inspection (CMM full dimensional report)
Trial molding (T0–T3)
Process optimization and CPK validation
7.4 Injection Molding Production
Process Parameters (PPSU-specific):
Parameter Value Criticality
Barrel temperature 360–400°C Prevents degradation
Mold temperature 120–180°C Reduces internal stress
Injection pressure 80–160 MPa Ensures complete fill
Holding pressure 40–80% of injection Minimizes sink and voids
Cooling time Optimized per geometry Maximizes cycle efficiency
7.5 Quality Control and Assurance
In-Process Controls:
First-article inspection at start of each batch
In-process sampling at defined intervals
Last-article inspection at batch completion
Real-time process monitoring via MES
Final Inspection:
Dimensional verification (CMM, optical)
Visual inspection (transparency, surface defects)
Functional testing (assembly verification, lid closure, rack compatibility)
7.6 Packaging and Delivery
Products are packaged to prevent damage during transit, with custom packaging solutions available for high-volume shipments.
Delivery Commitments:
On-time delivery guaranteed per purchase order terms
Real-time production tracking available for customers
Emergency expediting available for critical orders
Section VIII: Cost Optimization – Delivering Hard Cost Reductions
Ansix achieves significant cost reductions through three primary levers:
8.1 Material Optimization
Hot runner systems reduce material waste by eliminating cold runners
Precise shot size control minimizes regrind generation
Multi-cavity mold design maximizes material utilization per cycle
8.2 Process Efficiency
All-servo electric machines reduce energy consumption by 40–70% compared to hydraulic systems
Optimized cooling reduces cycle times by 15–30%
Automated part handling reduces labor costs and improves consistency
8.3 Quality-Driven Savings
First-pass yield > 98% minimizes scrap and rework
CPK ≥ 1.33 reduces inspection requirements
Long mold life spreads tooling investment over millions of parts
Total Cost Impact: Customers typically achieve 15–30% total cost reduction compared to alternative suppliers, driven by lower scrap rates, reduced energy consumption, and extended tool life.
Section IX: Risk Mitigation – What Ansix Solves for Customers
Customer Risk How Ansix Mitigates It
Design flaws discovered after tooling Comprehensive DFM analysis before steel is cut
Production delays In-house mold repair capability; 24-hour emergency restoration
Quality inconsistency MES-locked process parameters; closed-loop control systems
High tooling amortization 500,000–1,000,000 cycle mold life; spare parts included
Regulatory compliance failure Full material traceability; CPK documentation; material certificates
Supply chain disruption Vertically integrated manufacturing; all critical operations in-house
Section X: Industry Experience and Reliability
With over 28 years of manufacturing experience, Ansix has developed deep expertise in:
High-temperature engineering thermoplastics (PPSU, PEEK, PEI, PPS, LCP)
Precision mold manufacturing for medical and laboratory applications
High-volume production with consistent quality
Regulatory-compliant manufacturing (ISO-certified processes)
Conclusion: The Ansix Value Proposition
Ansix Tech approaches every PPSU mouse cage project with a fundamental philosophy: "The mold is not a piece of steel—it is a money-printing machine."
Every design decision, every material selection, and every process parameter is optimized not for technical elegance alone, but for customer value:
Lower costs through material efficiency, energy optimization, and reduced scrap
Reduced risk through DFM analysis, process control, and full documentation
Faster time-to-market through accelerated development and in-house capabilities
Peace of mind through guaranteed mold life, spare parts support, and lifetime repair commitment
For customers seeking a manufacturing partner who understands that technical excellence must translate into business value, Ansix Tech delivers. A full-process DFM report walkthrough is available upon request—demonstrating how weld lines, gas traps, shrinkage, and other risks are identified and eliminated before production begins.
This document was prepared based on Ansix Tech's proprietary manufacturing capabilities and industry best practices for PPSU injection molding. For specific project inquiries, including material grades, dimensional requirements, and production volumes, please contact Ansix Tech's engineering team for a customized solution.
Ansix Tech Co Ltd
If you have any plans related to PPSU mouse cage , you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #PPSU mouse cage #PPSU mouse cage Material #PPSU mouse cage Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #PPSU mouse cage injection molding #PPSU mouse cage injection tools #PPSU mouse cage injection moulds #PPSU mouse cage plastic mould #PPSU mouse cage plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #PPSU mouse cage injection molding Customized #Ansix mold factory #PPSU mouse cage china #PPSU mouse cage molds #injection factory for PPSU mouse cage #PPSU mouse cage injection molding #PPSU mouse cage injection molding factory #injection molding company #PPSU mouse cage injection mold companies #PPSU mouse cage Tooling #PPSU mouse cage mold limited #Ansix mold china #Ansix companies for PPSU mouse cage #Ansix company China #PPSU mouse cage facotry #Ansix Tech #Ansix Tech mould #PPSU mouse cage injection moulding #PPSU mouse cage injection moulding company #Ansix PPSU mouse cage parts injection mold companies #PPSU mouse cage injection molding companies china #PPSU mouse cage china factory #Ansix moulding companies #Ansix molding company #PPSU mouse cage injection moulding facotry #Ansix Tech mold #PPSU mouse cage mould #PPSU mouse cage plastic injection molding #ansix plastic mold #PPSU mouse cage Mold manufacturing #PPSU mouse cage parts manufacturing #PPSU mouse cage plastic parts factory #PPSU mouse cage injection parts mold #PPSU mouse cage PRECISION MANUFACTURING #PPSU mouse cage TOOL #China PPSU mouse cage mold #PPSU mouse cage Material injection moulding china #PPSU mouse cage mould china #china precision mold #PPSU mouse cage Material mold in china #PPSU mouse cage mold china #PPSU mouse cage Precision molds #High-precision molds #PPSU mouse cage High-precision tool #Injection molds #PPSU mouse cageFactory #PPSU mouse cageCompany #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #PPSU mouse cageCompany #PPSU mouse cageFactory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #PPSU mouse cage Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #PPSU mouse cage Large Injection Mold Manufacturer #PPSU mouse cage Plastic Mold Factory #Injection Mold #Plastic Mold