 Medical Molds
 Packaging Molds
 Personal Care Molds
 Electronic Molds
 Automotive Molds
 Home Appliance Molds
 Special Molds
 Design & Engineering
 Production & Manufacturing
 Global Presence
 Business Scope
 Component Solutions
 Product Assembly
 Quality Management
 Medical Device Manufacturing


WAIM WIT and GAIM mold
FEATURES
Hard Infrastructure: The Foundation of Customer Trust
1.1 Precision Mold Machining Equipment
Ansix's manufacturing capability begins with a world-class machine park designed to produce complex geometries with micron-level accuracy. The company employs 5-axis high-speed machining centers capable of achieving 0.002mm precision on complex curved surfaces—ensuring that product parting lines remain smooth and burr-free, eliminating secondary finishing operations that consume time and cost. For fine-feature manufacturing, Ansix utilizes wire EDM (slow wire cutting) systems that can machine micro-holes and narrow slots as small as 0.03mm, preventing thin-wall deformation that commonly plagues conventional machining approaches. The company also maintains in-house electrode machining centers and EDM (electrical discharge machining) workshops, enabling rapid mold modifications and repairs without outsourcing—a critical advantage when customers require urgent design changes or unexpected maintenance.
-
Mold Description
Product Materials:
PA66+GF30
Mold Material:
S136ESR
Number of Cavities:
1
Glue Feeding Method:
Hot runner
Cooling Method:
Water cooling
Molding Cycle
42.5s
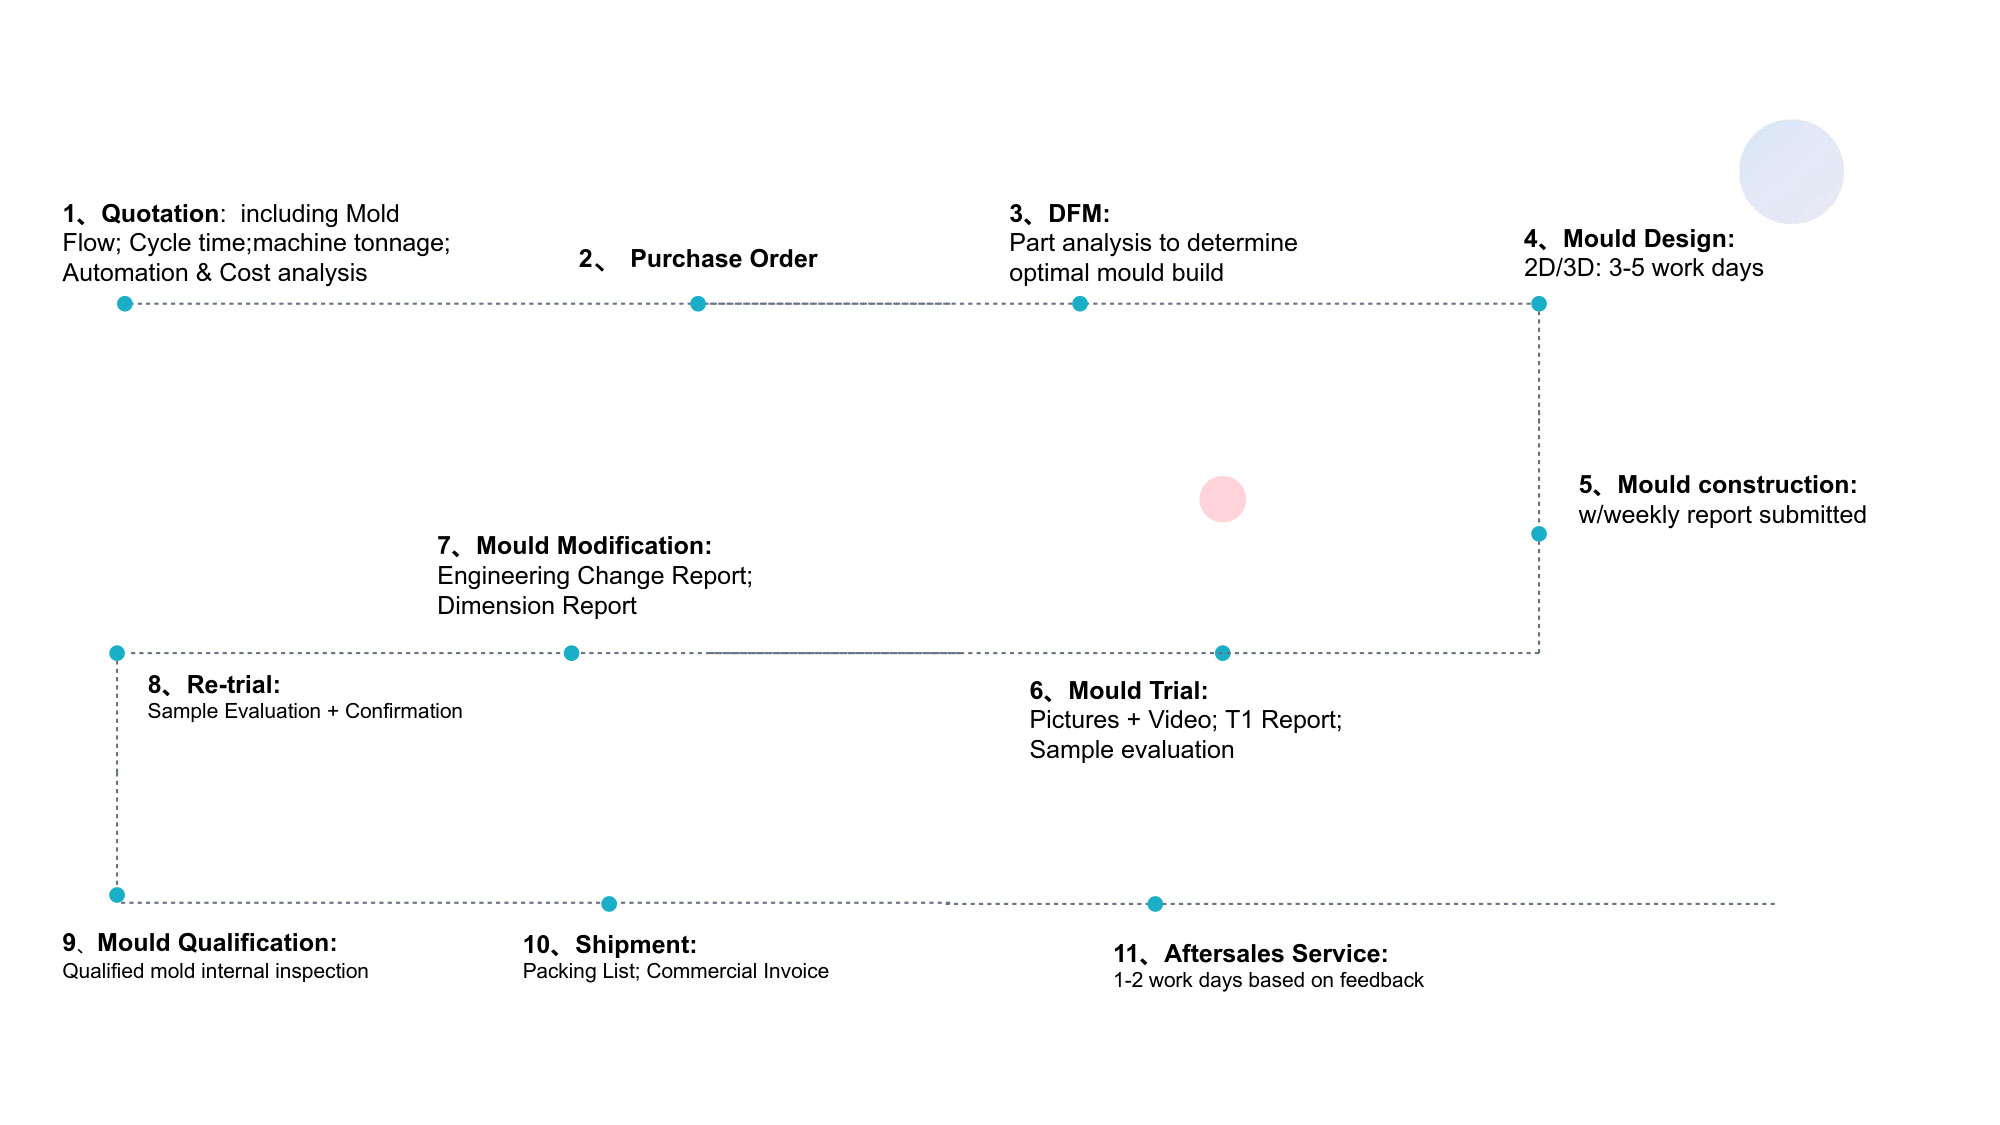
- The mold manufacturing process and product material selection
Injection Molding Machine Fleet
Ansix operates 260 injection molding machines from Japan's leading manufacturers including Fanuc, Sumitomo, and Toshiba, with clamping forces ranging from 30 tons to 2,800 tons. This comprehensive range covers product dimensions from micro medical components to large automotive and industrial parts. All machines are equipped with all-servo motor drives, delivering stable repeatability of ±0.1% —ensuring that every shot in a production run maintains consistent quality. This is not merely a specification; it translates directly to customer value: batch-to-batch consistency eliminates the costly scrap and rework that plague facilities with inferior machinery.
1.3 Quality Inspection and Metrology
Every mold and component undergoes rigorous inspection using coordinate measuring machines (CMM) and optical imaging systems. Ansix's quality protocol mandates that every mold set undergoes a full dimensional report before delivery, with critical dimension CPK ≥ 1.33—a statistical measure demonstrating that the manufacturing process is capable, stable, and produces parts well within specification limits. For customers, this means predictable quality, reduced inspection burden, and confidence that parts will assemble correctly the first time.
-
Mold Manufacturing Core Competitiveness: Value Through Specific Metrics
2.1 Mold Life and Material Selection
Customers' foremost concern is mold longevity—how many shots can they expect before expensive repairs or replacement become necessary. Ansix addresses this through meticulous material selection and transparent commitments:
Mold Component Material Grade Performance Commitment
Mold Base P20 Structural integrity and dimensional stability
Core/Cavity Inserts S136, 2344, 2343, 8407, SKD11/61, DC53, M340, 4Cr13, 9Cr18, NAK80, H13 Glass-fiber reinforced materials: 500,000 shots; Standard plastics: 1,000,000 shots
Each material is selected based on the specific application requirements—abrasion resistance for glass-filled materials, corrosion resistance for medical applications, or thermal conductivity for cycle time optimization. Ansix provides material certification reports and heat treatment curves for full traceability, giving customers documented assurance of material integrity.
2.2 Achievable Tolerances
Precision is not a marketing claim; it is a measurable outcome:
Standard structural components: ±0.05mm
Precision gears and medical components: ±0.005mm
These tolerances are achieved through a combination of high-precision machining, rigorous process control, and systematic verification. For customers, this means parts that fit without modification, assemblies that function as designed, and elimination of the "tolerance stack-up" problems that cause downstream failures.
2.3 Mold Type Capabilities
Ansix's technical portfolio encompasses the full spectrum of advanced mold configurations:
Hot runner systems: Reduce material waste by eliminating cold runner scrap, lowering per-part material costs by 15-30%
Stack molds: Double production output with the same machine footprint
Two-shot/multi-material molds: Enable complex multi-material components in a single molding cycle
High-gloss molds: Achieve surface roughness Ra < 0.05μm for transparent and optical applications
2.4 Gate and Runner System Optimization
Using advanced mold flow analysis, Ansix predicts weld line locations, gas entrapment zones, and filling imbalances before steel is cut. This simulation-driven approach enables optimization of gate quantity and placement to ensure balanced filling—eliminating short shots, sink marks, and dimensional variations that plague poorly designed molds. The result is first-time-right molds that start production faster and produce higher-quality parts.
2.5 Delivery Standards
Time-to-market is critical. Ansix offers tiered delivery commitments:
Simple molds: 10 days
Medium-complexity molds: 25-45 days
Expedited (premium service): As fast as 20 days
Crucially, expedited delivery never compromises validation—all verification steps remain intact, ensuring that speed does not come at the cost of quality.
III. Injection Molding Process Control: Eliminating Quality Anxiety
3.1 Process Standardization and MES Integration
All injection molding machines are networked and integrated with MES (Manufacturing Execution System) . Molding parameters—temperature, pressure, velocity, and time—are locked within the system and can only be modified by authorized engineers. Every production batch undergoes first-article and last-article inspection, ensuring that quality remains consistent throughout the run. For customers, this eliminates the "drift" that causes dimensional variation over long production runs.
3.2 Dimensional Stability Control
Ansix employs zone-controlled mold temperature controllers that maintain core and cavity temperature differentials within 2°C—a critical factor in minimizing warpage and distortion. This is complemented by ultrasonic wall thickness sensors that provide real-time feedback on wall thickness variations, automatically adjusting packing pressure to compensate. The results are measurable: for similar bracket components produced across three batches within one week, critical hole-to-hole spacing variation ≤ 0.02mm.
3.3 Surface Quality and Appearance Grades
Ansix achieves surface quality that meets the most demanding requirements:
Transparent components: No bubbles, no flow marks
Platable components: No gas marks or surface defects
High-gloss components: Surface roughness Ra ≤ 0.2μm
For components requiring painting or printing, Ansix provides compensation for deformation during the molding process, ensuring that print registration accuracy ≤ ±0.1mm—eliminating the costly rejects that occur when printed graphics misalign with part geometry.
3.4 Specialty Material Processing Capabilities
Ansix has extensive production experience with a broad spectrum of engineering thermoplastics:
Material Family Specific Grades Key Applications
PC/ABS Alloys PC/ABS Automotive interiors, electronics housings
High-performance PC, PPS+40%GF, PEEK, PEI, PPS, LCP High-temperature, high-strength applications
Fluoropolymers PTFE, PFA Chemical resistance, medical
Polyamides PA6+GF30, PBT Structural components, electrical
Silicone Liquid Silicone Rubber (LSR) Medical, sealing applications
Ansix also validates flame retardancy (UL94 V-0) for electrical housings and UV resistance (3,000 hours without color change) for outdoor applications—critical certifications that eliminate customer testing burdens.
IV. Full-Service Lifecycle Support: Reducing Total Cost of Ownership
4.1 Early Engagement and DFM Reports
Ansix provides Design for Manufacturability (DFM) reports before any contract is signed. These comprehensive documents include:
Draft angle recommendations
Wall thickness optimization
Gate location proposals
Ejector pin mark location allowances
This early intervention prevents the most costly mistakes: discovering after mold construction that a design cannot be manufactured. By identifying and resolving issues in the design phase, Ansix saves customers weeks of delay and tens of thousands of dollars in mold modifications.
4.2 Trial Molding and Iterative Refinement
The development process follows a structured T0 to T3 trial sequence:
T0: First mold trial—identifies fundamental issues
T1: First correction round—validates modifications
T2: Second refinement—fine-tunes process parameters
T3: Final validation—confirms production readiness
Each trial is accompanied by a detailed improvement report. Ansix can rapidly exchange inserts to validate different approaches without rebuilding the entire mold—significantly reducing development cost and time.
4.3 Pilot Production Validation
Before committing to full-scale production, Ansix offers 100-500 shot pilot runs to validate:
Production yield rates
Process capability (CPK)
Dimensional stability
Cycle time consistency
Only after confirming stability does Ansix transition to mass production—eliminating the risk of discovering problems after the production line is running at full capacity.
4.4 Maintenance and Spare Parts
Ansix delivers each mold with a complete set of spare wear parts (ejector pins, core inserts) to minimize downtime. The company provides:
Scheduled maintenance every 200,000 shots
Lifetime repair service at cost-based pricing
In-house repair capability—standard weld repair/insert replacement completed within 24 hours
V. Differentiated Competitive Advantages: Direct Answers to Customer Pain Points
Common Customer Complaint Ansix's Technical Response Customer Value
Frequent mold repairs disrupt production 2,000-shot aging test before delivery with wear report; 3-year structural warranty (excluding normal wear parts) Predictable maintenance costs; uninterrupted production
Excessive flash increases finishing costs 0.005mm parting line fit precision; self-locking clamp force compensation; flash控制在0.03mm以内 Eliminates manual deburring; reduces labor costs
Inconsistent dimensions batch-to-batch Ultrasonic wall thickness sensors with real-time compensation; in-mold temperature/pressure sensors with closed-loop control Reliable parts; no assembly issues
Long repair lead times In-house electrode machining and EDM; 24-hour repair turnaround for standard modifications Minimized production interruption
VI. The Ansix Philosophy: Mold as a Revenue-Generating Asset
At Ansix, a mold is not viewed as a piece of steel—it is understood as a revenue-generating asset. Every design decision considers:
Mold robustness: Ensuring the mold survives millions of cycles
Venting pathways: Eliminating gas traps that cause burn marks
Thermal balance: Minimizing cycle time through optimized cooling
Ejection systems: Ensuring reliable part removal without damage
The goal is a mold that arrives at the customer's production line ready for immediate production—requiring no debugging, producing minimal flash, and delivering maximum lifespan.
VII. Manufacturing Process Flow for WAIM/WIT/GAIM Molds
7.1 Project Initiation and Feasibility Analysis
Every WAIM, WIT, and GAIM project begins with a comprehensive feasibility assessment. Ansix evaluates:
Part geometry and hollow section requirements
Fluid channel layout and gate positioning
Material selection based on mechanical and thermal requirements
Production volume projections and cycle time targets
7.2 Mold Flow Analysis (DFM)
Using advanced simulation tools like Moldex3D, Ansix performs detailed fluid-assisted injection molding simulations. For WAIM processes, the simulation models water penetration behavior, cooling efficiency, and hollow section formation. For GAIM processes, the simulation evaluates gas penetration patterns and pressure distribution. These simulations identify:
Optimal fluid injection timing
Penetration depth and uniformity
Potential weld line and gas trap locations
Cooling channel effectiveness
7.3 Mold Design and Engineering
The mold design phase incorporates:
Cooling system design: Conformal cooling channels optimized for WAIM/GAIM processes, where water or gas is injected into the hollow sections
Runner and gate systems: Engineered to accommodate fluid injection needles or nozzles
Ejection systems: Designed for reliable part removal without damaging hollow sections
Venting: Strategically placed to allow air and gas escape during fluid injection
7.4 Mold Manufacturing
The manufacturing sequence includes:
CAD/CAM programming for precision machining
Rough machining of mold bases and inserts
Heat treatment of core/cavity inserts
Precision finishing: 5-axis machining, EDM, wire EDM
Surface finishing: Polishing, texturing, coating
Assembly and fitting of all components
7.5 Mold Validation and Tryout
Each mold undergoes rigorous validation:
T0 tryout: First shots to verify basic functionality
Process optimization: Fine-tuning fluid injection parameters
Dimensional verification: Full CMM inspection
Aging test: 2,000-shot run to validate durability
7.6 Production and Quality Control
During mass production, Ansix maintains:
Real-time process monitoring through MES
Statistical process control (SPC) for all critical dimensions
Regular maintenance per established schedules
Continuous improvement based on production data
VIII. Material Selection and Characteristics for WAIM/WIT/GAIM Components
8.1 Material Selection Criteria
Ansix selects materials based on:
Mechanical properties: Strength, stiffness, impact resistance
Thermal properties: Heat deflection temperature, glass transition temperature
Flow characteristics: Melt flow index, viscosity
Fluid compatibility: Resistance to water or gas exposure during WAIM/GAIM processing
End-use requirements: Chemical resistance, UV stability, flame retardancy
8.2 Common Materials and Specifications
Material Key Properties WAIM/GAIM Suitability
PA6+GF30 High strength, good flow Excellent for structural hollow sections
PPS+40%GF High temperature resistance, dimensional stability Ideal for automotive under-hood applications
PC Optical clarity, impact resistance Transparent hollow components
PEEK Extreme temperature resistance, chemical resistance Medical and aerospace applications
LCP High flow, thin-wall capability Electronic connectors, thin hollow sections
PP Low cost, good chemical resistance Consumer products, fluid handling
IX. Cost Reduction and Value Creation
9.1 Material Cost Optimization
WAIM and GAIM processes inherently reduce material consumption by creating hollow sections without sacrificing structural integrity. Ansix optimizes:
Wall thickness reduction through fluid-assisted core-out
Runner system optimization to minimize scrap
Material selection balancing performance and cost
9.2 Cycle Time Reduction
WAIM offers shorter cooling cycles compared to GAIM due to water's superior thermal conductivity. Ansix leverages this advantage through:
Optimized cooling channel design
Process parameter optimization
Automated part handling
9.3 Yield Improvement
Through rigorous process control and validation, Ansix achieves:
First-pass yield > 98% for mature production
Scrap rate < 2% across production runs
Minimal rework through right-first-time manufacturing
9.4 Total Cost of Ownership Reduction
Cost Factor Ansix Advantage Customer Savings
Mold investment Optimized design reduces complexity Lower upfront cost
Production cost Faster cycles, less scrap Lower per-part cost
Maintenance cost Predictive maintenance, long mold life Lower operating cost
Quality cost High CPK, minimal rejects Lower inspection and rework cost
X. Conclusion: Delivering Customer Value Through Technical Excellence
Ansix Tech's approach to WAIM, WIT, and GAIM mold manufacturing is built on a foundation of technical excellence translated into tangible customer value. The company's 28 years of experience, 260 injection molding machines, 30,000+ molds delivered, and precision capabilities reaching 0.002mm provide the infrastructure. But infrastructure alone does not create value—what distinguishes Ansix is the systematic translation of technical capabilities into customer benefits:
Risk reduction through DFM analysis, pilot validation, and rigorous quality control
Cost reduction through material optimization, cycle time reduction, and yield improvement
Time-to-market acceleration through parallel engineering, rapid prototyping, and expedited delivery options
Peace of mind through transparent communication, documented quality, and lifetime support
For customers considering WAIM, WIT, or GAIM solutions, Ansix offers not just a mold manufacturer, but a strategic partner committed to turning complex fluid-assisted molding technologies into competitive advantage. As the company's philosophy states: "A mold is not a piece of steel—it is a revenue-generating asset."
Ansix Tech Co Ltd
If you have any plans related to WAIM WIT and GAIM mold
, you can contact us at any time. We will turn your ideas into reality, let you realize your dreams, and obtain large orders from the market. Our contact information is info@ansixtech.com. Or contact our CTO, mail: stephen@ansixtech.com
#www.ansixtech.com #ansixtech.com #WAIM WIT and GAIM mold #WAIM WIT and GAIM mold Material #WAIM WIT and GAIM mold Mold injection mold companies #Ansix #Ansix moulds #Ansix china #Ansix tech china #Ansix tech company #Ansix facotry #WAIM WIT and GAIM mold injection molding #WAIM WIT and GAIM mold injection tools #WAIM WIT and GAIM mold injection moulds #WAIM WIT and GAIM mold plastic mould #WAIM WIT and GAIM mold plastic tools #Ansix Tech #Ansix molds #Ansix injection molding #Ansix mold factory #WAIM WIT and GAIM mold injection molding Customized #Ansix mold factory #WAIM WIT and GAIM mold china #WAIM WIT and GAIM mold molds #injection factory for WAIM WIT and GAIM mold #WAIM WIT and GAIM mold injection molding #WAIM WIT and GAIM mold injection molding factory #injection molding company #WAIM WIT and GAIM mold injection mold companies #WAIM WIT and GAIM mold Tooling #WAIM WIT and GAIM mold mold limited #Ansix mold china #Ansix companies for WAIM WIT and GAIM mold #Ansix company China #WAIM WIT and GAIM mold facotry #Ansix Tech #Ansix Tech mould #WAIM WIT and GAIM mold injection moulding #WAIM WIT and GAIM mold injection moulding company #Ansix WAIM WIT and GAIM mold parts injection mold companies #WAIM WIT and GAIM mold injection molding companies china #WAIM WIT and GAIM mold china factory #Ansix moulding companies #Ansix molding company #WAIM WIT and GAIM mold injection moulding facotry #Ansix Tech mold #WAIM WIT and GAIM mold mould #WAIM WIT and GAIM mold plastic injection molding #ansix plastic mold #WAIM WIT and GAIM mold Mold manufacturing #WAIM WIT and GAIM mold parts manufacturing #WAIM WIT and GAIM mold plastic parts factory #WAIM WIT and GAIM mold injection parts mold #WAIM WIT and GAIM mold PRECISION MANUFACTURING #WAIM WIT and GAIM mold TOOL #China WAIM WIT and GAIM mold mold #WAIM WIT and GAIM mold Material injection moulding china #WAIM WIT and GAIM mold mould china #china precision mold #WAIM WIT and GAIM mold Material mold in china #WAIM WIT and GAIM mold mold china #WAIM WIT and GAIM mold Precision molds #High-precision molds #WAIM WIT and GAIM mold High-precision tool #Injection molds #WAIM WIT and GAIM moldFactory #WAIM WIT and GAIM moldCompany #Super Large Injection Mold Factory #Large Tonnage Injection Molding Factory #WAIM WIT and GAIM moldCompany #WAIM WIT and GAIM moldFactory #2800T Injection Molding Factory #3000 Ton Injection Molding #4500 Ton Injection Molding Factory #WAIM WIT and GAIM mold Large Mold Injection Molding #Large Plastic Mold Injection Molding Factory #WAIM WIT and GAIM mold Large Injection Mold Manufacturer #WAIM WIT and GAIM mold Plastic Mold Factory #Injection Mold #Plastic Mold

- PA66+GF30 TDS